Flow and compaction
Bridging, rat-holing, settling and sensitivity to agitation influence hopper geometry, auger tooling and the consistency of powder presentation to the filler.
Packaging systems configured around your application Defined project scope

Configure the HS-180 horizontal form-fill-seal platform around the real powder, target dose, roll film, finished sachet and acceptance test. The machine route can include servo auger dosing, powder refill, dust management, coding, weight inspection and downstream handling, but each item must be confirmed in the issued project scope.
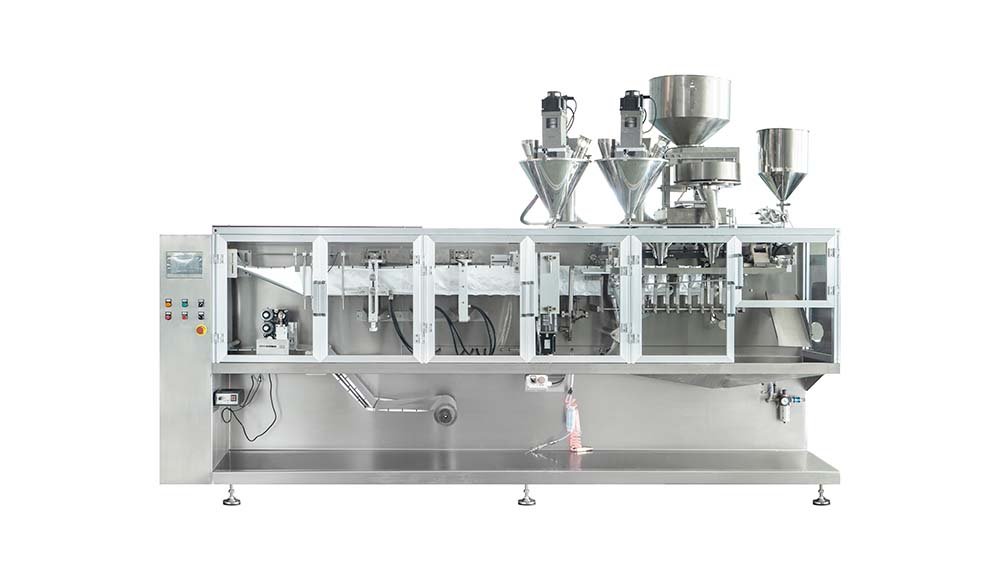
A powder sachet packing machine combines roll-film handling, sachet forming, powder metering, filling, sealing, cutting and discharge in one coordinated process. On this page, the HS-180 is the HFFS platform and the auger, feeder, dust-control, inspection and FAT requirements form the powder-specific configuration. The correct setup follows powder behavior and accepted finished packs, not the product name alone.
A product name such as coffee, seasoning, milk powder, flour, baking soda or detergent is only a starting point. Confirm the production condition that the machine must handle and test.
Bridging, rat-holing, settling and sensitivity to agitation influence hopper geometry, auger tooling and the consistency of powder presentation to the filler.
Record the conditioned and refill states. Aerated powder can occupy more volume during filling and settle after the sachet leaves the dosing station.
Observe airborne powder, cutoff behavior and residue near the pouch mouth. These conditions affect fill timing, extraction and final-seal cleanliness.
Define removable contact parts, retained-powder areas, allergen or cross-contamination controls and the verification required before the next product is released.
The packaging machine and auger filler must share one control and test boundary. A stable empty machine cycle does not prove that powder supply, dosing, sealing and downstream handling will produce accepted packs.
Present the powder to the dosing hopper under a defined condition. Confirm the manual or automatic refill method, level control, hopper capacity and interface responsibility.
Select the auger and operating recipe from the real powder and dose range. The available HS-180 source identifies a servo-driven auger route for its reference powder project.
Control roll dimensions, winding direction, web tracking, print repeat and registration marks before the film enters the sachet-forming sequence.
Create the approved 3-side or 4-side seal geometry from heat-sealable roll film. Seal width, temperature window and cut position belong to the controlled package specification.
Coordinate dose release, fill height and cutoff so powder reaches the open sachet without unacceptable contamination in the final-seal area.
Define coding, weight checks, reject logic, accepted-pack counting, collection and any downstream conveyor or cartoning interface in the quotation and FAT.
Need to compare this route with VFFS, stick pack or another forming architecture? Use the form fill seal machine selection guide before fixing the platform.
The sachet machine and dosing head must share one product and acceptance basis. Review the integrated auger filler setup for powder conditioning, tooling, cutoff, refill behavior and the handoff into the roll-film sachet sequence.
The complete HS-180 specification and Product entity belong to the HS-180 multifunction sachet platform. The summary below keeps only the source-backed boundaries needed to assess this powder application.
| Scope item | Documented HS-180 boundary | Project confirmation required |
|---|---|---|
| Machine architecture | Horizontal form fill seal with intermittent pouch transport and one listed filling station. | Final station layout, filler interface, controls, guarding and downstream handoff. |
| Platform speed | The source lists 40–70 bags per minute. | Accepted powder sachets per minute for the agreed powder, dose, film, size, run duration and defect rules. |
| Sachet envelope | Listed pouch dimensions are 60 × 80 mm minimum to 180 × 220 mm maximum. | Controlled drawing, seal layout, fill opening, headspace, artwork and change-part matrix. |
| Fill-volume boundary | The source lists a maximum pouch volume of 400 ml. | Actual powder mass, bulk-density range, aerated condition, settling and usable sachet volume. |
| Roll-film boundary | Maximum listed reel diameter 400 mm, reel width 440 mm and core diameter 76 mm. | Film structure, thickness, sealant layer, winding direction, print repeat, eye mark, friction and splice rule. |
| Powder dosing | The reference project lists a servo auger and identifies baking soda as the sample powder. | Auger tooling, target doses, tolerance method, powder conditioning, cutoff and refill behavior. |
| Construction | The source lists SUS304 product-contact parts; other mechanisms can include SUS304 and aluminum alloy. | Issued product-contact drawing, surface requirements, cleanability and any destination-specific requirement. |
| Utilities | The platform source lists 5.0 kW and 100 L/min compressed air at 0.6 MPa, with electrical supply configured to the project. | Valid voltage/frequency, installed load, air quality, pressure at the machine and buyer connection points. |
Performance boundary: these values describe the documented HS-180 platform and reference configuration. Dose accuracy, dust performance, seal integrity and accepted output must be demonstrated with the agreed sample, package material and FAT method.
The matrix is a review framework, not a promise that one standard auger handles every powder. Representative samples are needed before tooling and acceptance limits are released.
| Observed condition | Configuration questions | Evidence to request |
|---|---|---|
| Free-flowing, consistent powder | Confirm auger geometry, cutoff, target dose range and the effect of hopper level on repeatability. | Individual weight readings across startup, normal running and representative refill events. |
| Aerated or low-density powder | Define sample conditioning, hopper agitation, refill method, fill volume and post-fill settling time. | Recorded bulk-density condition plus dose checks at an agreed time after filling. |
| Cohesive or bridging powder | Review hopper wall angle, agitation, product feed, auger geometry and the acceptable response to interrupted flow. | Video and weight data showing stable supply, restart and recovery with the real sample. |
| Dusty powder or product tailing | Review fill height, cutoff, extraction point, seal-area protection and cleaning access. | Close-up seal images, contamination log, rejected-pack count and the agreed seal test. |
| Wear or corrosion concern | Identify the powder property creating risk and specify contact materials, finish and wear components in the issued scope. | Product-contact declaration, component drawing and maintenance responsibility for the approved configuration. |
| Frequent recipe or allergen change | Define the change matrix, removable contact parts, retained-product inspection and post-clean release method. | Recorded dismantling, cleaning, reassembly and first-acceptable-pack sequence. |
A finished sachet drawing does not replace a material specification. The machine supplier, film converter and product owner need one controlled set of dimensions and test conditions.
Provide finished width and length, seal widths, fill opening, headspace, cut style, tear feature, code area and the dimensional tolerances used for acceptance.
Provide structure, thickness, sealant face, web width, roll diameter, core, winding direction, friction information, splice rule and representative production rolls.
Provide print repeat, eye-mark location and contrast, artwork orientation, code location and the permitted print-to-cut and print-to-seal relationship.
If the final package format is still undecided, compare stick pack and flat sachet geometry before asking for one machine quotation. For a narrow single-dose food-supplement format, review the supplement powder stick-pack route rather than treating it as the same flat-sachet project.
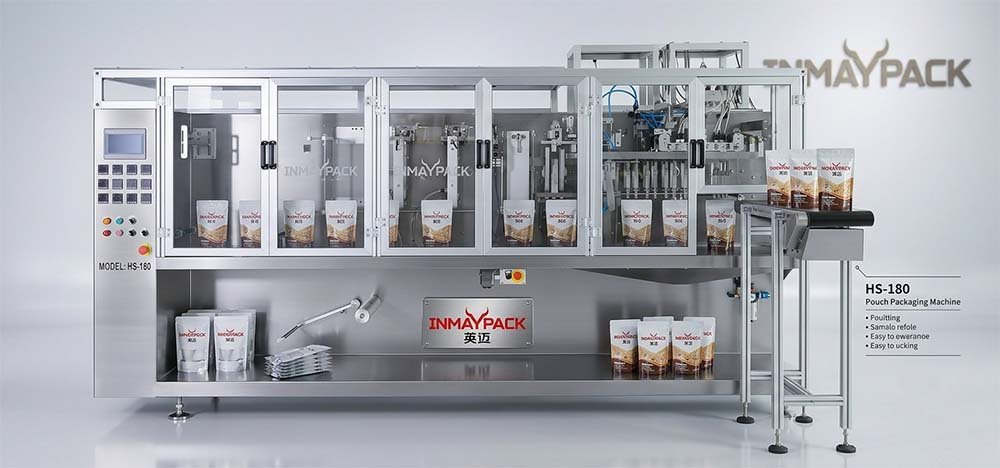
Send the powder, dose, sachet drawing and accepted-output target. The first review should select the architecture before fixing optional equipment.
Two quotations with the same model name are not comparable when one excludes the powder feed, inspection or acceptance work. Each line item needs an owner, interface and test.
| Scope layer | What to identify in the quotation | Acceptance question |
|---|---|---|
| Base HFFS platform | Film unwind, forming, pouch transport, sealing, cutting, controls, guarding, discharge and the exact supplied change parts. | Does the issued configuration produce the approved sachet geometry and remain stable under the agreed test? |
| Powder dosing | Auger filler, hopper, agitator if used, tooling, recipe range, mounting and control handshake with the packaging machine. | How will dose readings be sampled, calculated and accepted across the priority SKU range? |
| Powder replenishment | Manual loading or the listed screw-elevator option, level control, access, dust containment and responsibility for upstream supply. | What happens to dose and output during a normal refill event? |
| Dust management | The listed dust-removal option, pickup location, airflow responsibility, filters, utilities and cleaning access. | What visible or measured seal-contamination rule must the system meet? |
| Coding and inspection | Coder, checkweigher with rejection, code checks, reject confirmation and data or traceability interfaces when required. | Which defects trigger rejection, and how are rejected and accepted packs reconciled? |
| Downstream handling | Outfeed conveyor, collection, counting, buffering, cartoning interface and stop/restart signals. | Is accepted output measured at the packer discharge or after the required downstream handoff? |
| Buyer-supplied inputs | Representative powder, film, drawings, utilities, test instruments, acceptance rules and destination requirements. | Are the sample quantity, shipping condition and approval responsibilities recorded before FAT? |
Use the sachet packing machine price and cost guide to normalize machine, dosing, options, FAT, delivery, commissioning and spares before comparing supplier totals.
A useful FAT ties every result to one controlled powder condition, dose, film, sachet and operating basis. Retain the data needed to reproduce the approved state.
| FAT checkpoint | Record before testing | Evidence to retain |
|---|---|---|
| Controlled inputs | Powder batch and condition, nominal dose, sachet drawing, film roll, tooling and configuration revision. | Approved test sheet, sample identifiers, drawings and configuration record. |
| Dose result | Scale method, sampling frequency, tolerance basis, startup treatment and refill-event sampling. | Individual readings, summary calculation and out-of-tolerance count. |
| Package result | Dimensions, registration, code, cut, appearance and agreed seal-integrity method. | Retained samples, close-up images, measurements and defect log. |
| Accepted output | Run duration, planned stops, permitted rejects and the definition of an accepted sachet. | Total produced, accepted count, rejected count, stops, causes and recovery time. |
| Cleaning and change | Product or SKU change, dismantling boundary, cleaning method and post-clean release rule. | Recorded sequence, observations, inspection result and unresolved actions. |
| Handover | Required video views, manuals, drawings, backups, settings, training and open-item ownership. | Agreed files matched to the approved machine and test revision. |
Use this page for a roll-film, single-lane flat-sachet powder application. Continue to another page only when the finished pack, lane count or pouch-supply method is different.
If the project must be evaluated against the HS-130 reference envelope—60 × 80 to 140 × 180 mm sachets, up to 160 ml and 50–90 packs/min—review the HS-130 3/4-side seal sachet machine. Treat those values as screening boundaries; confirm powder behavior, dose, film and accepted output in the quotation and FAT.
No. This page covers the powder-specific application and auger route. Use the HS-180 multifunction sachet platform for the primary product entity and complete platform specification.
The auger filler meters powder. The complete powder sachet packing machine also handles roll film, forms the sachet, coordinates filling, completes the seals, cuts the pack and manages discharge. The two systems must be controlled and tested together.
Not reliably. The same named powder can vary in bulk density, aeration, flow, dust and compaction. A representative sample, dose basis, sachet drawing and film are needed before the auger, refill method and acceptance test are fixed.
No. That figure is the documented HS-180 platform range. Accepted output depends on the powder condition, dose, sachet dimensions, film, refill method, seal criteria, inspection rules and sustained test basis.
The HS-180 source lists 3-side and 4-side sealed flat packages. The issued proposal must identify the approved drawing, seal layout, film data, tooling and size range for the selected project.
The available source lists a screw elevator, dust-removal module and checkweigher with rejection as project options. Inclusion, utilities, controls, placement and acceptance criteria must be confirmed in the valid quotation.
Run a controlled trial using the agreed powder condition, scale, sampling frequency, tolerance basis, refill events and test duration. Retain individual readings and rejected-pack records. The result belongs to that tested setup rather than every powder the machine might run.
Send the production powder and its known behavior, dose range, sachet drawing, roll-film specification, target accepted output, cleaning needs, coding and inspection scope, destination utilities and the required FAT evidence.
Require every supplier to quote against the same powder, dose, package, output definition, options, FAT, delivery and support boundary. Compare accepted output and included responsibility rather than the base-machine total alone.
Share a representative powder sample, nominal grams per sachet, package drawing, roll-film data and target accepted output. INMAYPACK will review the dosing, refill, dust, inspection and FAT boundary before preparing the project scope.
Email: sales@ewpackmachinery.com · WhatsApp: +86 186 5879 9162