Bulk density may change through the line
Record the supplied condition, refill method and density range so hopper geometry, agitation and auger tooling are reviewed against the real product.
Packaging systems configured around your application Defined project scope

Choose a milk powder filling and packaging route by powder condition, bulk density, aeration, dose, moisture protection, cleaning and finished pack—not by an empty-cycle speed alone.
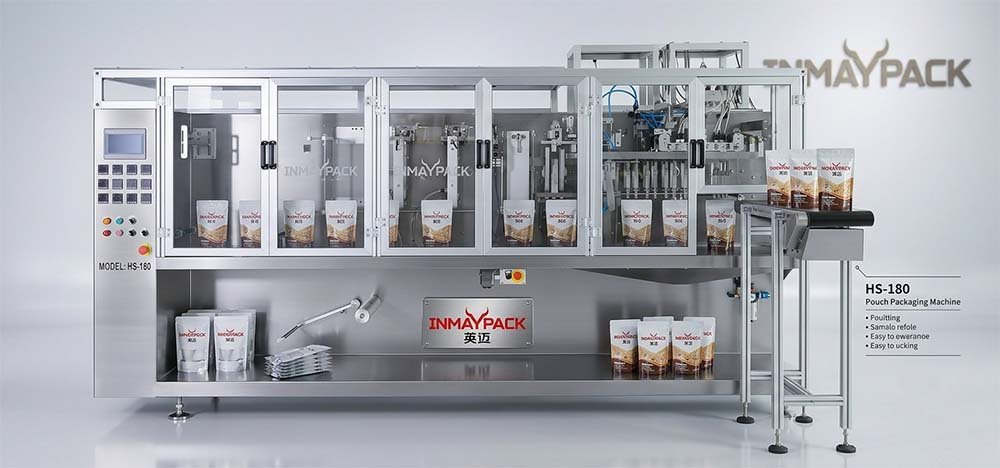
Different milk powders can aerate, settle, absorb moisture or behave differently after conveying and hopper refill. Confirm the representative powder, dose, pack format and acceptance method before selecting the feeder, auger tooling, product-contact boundary and sachet or pouch platform as one system.
The product name alone does not define machine behavior. Review the powder after conveying, hopper refill and exposure to the planned production environment.
Record the supplied condition, refill method and density range so hopper geometry, agitation and auger tooling are reviewed against the real product.
Fine powder near the package mouth can affect sealing. Headspace, cutoff behavior, extraction and environmental boundaries must be tested with the selected pack.
Define access, removable parts, cleaning method, cross-contact controls and verification before fixing the machine and line responsibility.
These architectures solve different package-handling tasks. Compare them using the same powder, dose, material and accepted-output basis.
A horizontal sachet platform can be paired with a project-confirmed powder filler after dose, film, bag size, dust control and seal acceptance are defined.
Review the powder sachet machineThe machine forms a compatible stand-up pouch from film, then coordinates opening access, milk powder dosing, headspace and sealing in one HFFS route.
Compare roll-film Doypack systemsA premade-pouch platform must prove pickup, opening, filling and clean top sealing with the supplied pouch and the selected powder dosing system.
Compare premade pouch systemsScope boundary: this page covers flexible sachets and pouches for project-confirmed milk powder applications. Cans, jars, rigid containers, open-mouth sacks and 25 kg bulk-bag systems require a separate equipment review.
| Route | Package supply | Dosing review | Use it when | Evidence to request |
|---|---|---|---|---|
| HS-180 powder sachet route | Flat sachet formed from roll film | Servo auger candidate for project-confirmed powder | The required pack is a 3-side or 4-side sealed flat sachet. The source configuration states 40–70 bags/min, subject to product, bag and test conditions. | Supplied-powder test, dose results, film registration, seal cleanliness and accepted packs. |
| HFFS Doypack route | Stand-up pouch formed from roll film | Filler and cutoff matched to the supplied milk powder | The retail format needs a project-confirmed roll-film stand-up pouch. | Controlled pouch drawing, forming, opening access, dosing, headspace and sealing evidence. |
| Premade pouch route | Finished pouches supplied to the machine | Powder filler selected after sample review | The pouch format, finish or material is better supplied preformed. | Pouch pickup/opening success, fill control, mouth cleanliness and top-seal results. |
Published values are not interchangeable guarantees. Final output, dose range, accuracy and machine scope must be confirmed with the representative milk powder and package during project testing.
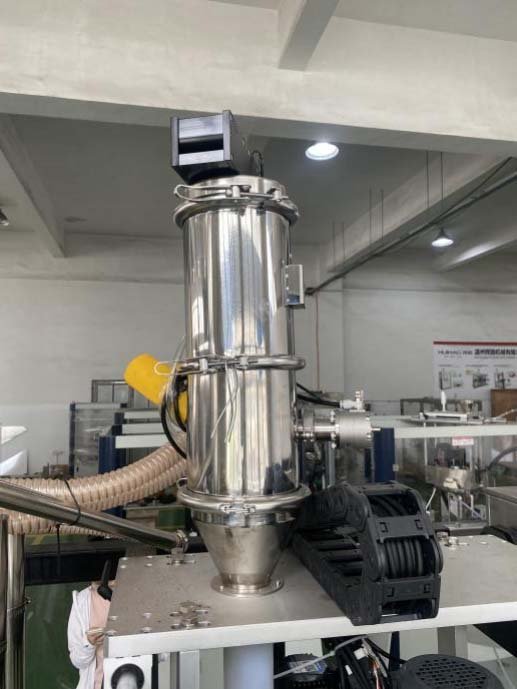
Stable output depends on how the powder reaches the hopper, how its condition changes during refill, how the package is presented, how seals are protected and how accepted packs leave the line.
| Input | What to provide | Decision it changes |
|---|---|---|
| Representative milk powder | Formula or grade, supplied condition, particle distribution, bulk-density range, moisture context, handling history and test quantity. | Feed, hopper, agitation, dosing tooling and environmental boundary. |
| Dose and tolerance | Nominal dose, allowed range and how accepted weight will be measured. | Filler size, control method, inspection and test duration. |
| Package | Format, controlled drawing, material structure, dimensions, headspace, seal geometry and coding area. | Machine route, forming parts, pouch handling and sealing. |
| Hygiene and cleaning | Product-contact boundary, cross-contact controls, extraction interface, cleanout method and verification. | Enclosure, access, removable parts and changeover plan. |
| Accepted output | Saleable packs per minute, test duration, allowed rejects, refill assumption and downstream state. | Commercial comparison and FAT acceptance criteria. |
| Line interfaces | Utilities, coding, checkweighing, reject handling, conveyors and secondary packaging. | Controls, layout, signals and responsibility split. |
Agree the representative milk powder, package, dose, environment, utilities and line state before the run.
Include the planned powder supply and hopper-refill sequence, not only isolated doses.
Check weight method, settling and headspace, seal cleanliness, code, appearance, leaks and defined rejects.
Keep settings, duration, sample identity, results, deviations and responsibilities.
Use the packaging machine FAT checklist to define samples, responsibilities, pass criteria and evidence before testing.
Share the representative powder, dose, package drawing, material, accepted-output basis, cleaning boundary and line interfaces. INMAYPACK will compare suitable flexible-package routes before recommending a configuration.