
Horizontal Form Fill Seal Machine Systems for Pouches
Form pouches from roll film, fill your product and seal the finished pack. Compare stand-up, zipper, spout and shaped-pouch configurations with the filling system matched to your application.
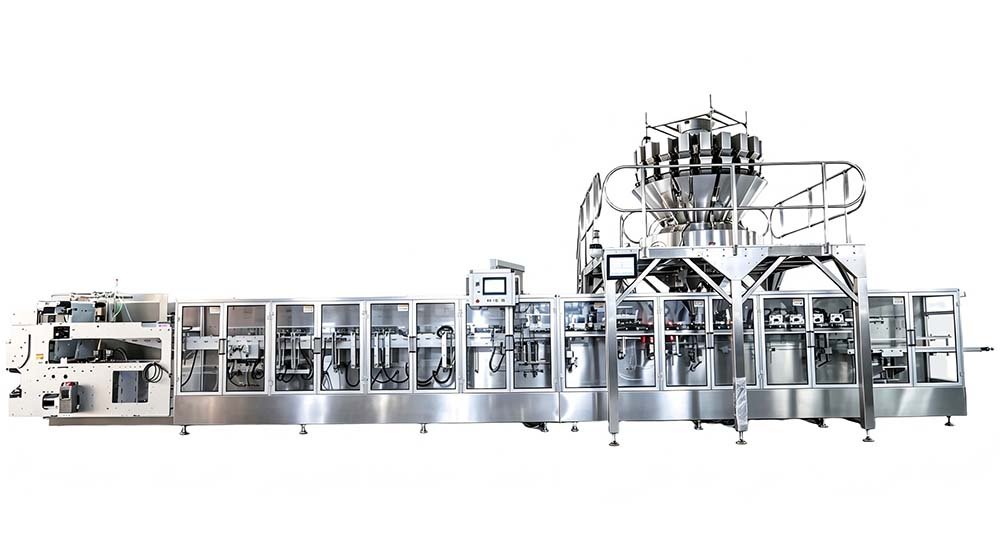
What is a horizontal form fill seal machine?
A horizontal form fill seal machine (HFFS) converts roll film into a pouch, presents that pouch for filling and closes the package in one indexed horizontal process. For INMAYPACK's pouch scope, the sequence can include film unwinding, registration, bottom-gusset forming, side sealing, cutting, pouch opening, product dosing, top sealing, cooling and discharge.
The machine architecture must be matched to the finished pouch. A standard stand-up pouch, zipper pouch, spout pouch and contour-cut pouch do not use identical tooling or cycle time. Film, filler, closure and output therefore have to be approved as one system.
Scope boundary This page concerns roll-film pouch-making HFFS systems. It does not describe horizontal flow wrappers, thermoformers, bottle fillers or premade-pouch machines. Those are different packaging routes even when a supplier uses the broad term “horizontal packaging machine.”
Start with the pouch you want to produce
Choose the pouch format first, then review the forming tools, filling system and closure requirements for that route.
Stand-up pouch formed from roll film
Bottom-gusset geometry, side seals, opening access, filling support and top sealing must work across the approved pouch range.
Review the HMK2000 stand-up pouch routeZipper Doypack
Zipper supply, alignment, application, sealing, opening force and final pouch access add dedicated tooling and process time.
Review zipper pouch machinerySpout or capped pouch
The spout, cap, weld geometry, filler, nozzle access, torque or closure condition and clean-seal requirement must be qualified together.
Review spout-pouch filling systemsShaped or bottle-shaped Doypack
Contour tooling changes web layout, cutting, edge support, transfer stability and opening access. A controlled drawing and real film trial are required.
Review shaped Doypack requirementsFollow the web from roll to accepted pouch
Each station creates the input condition for the next. A fault that appears at filling or top sealing may begin earlier with web tension, registration, gusset geometry, cutting or pouch transfer.
Unwind and guide
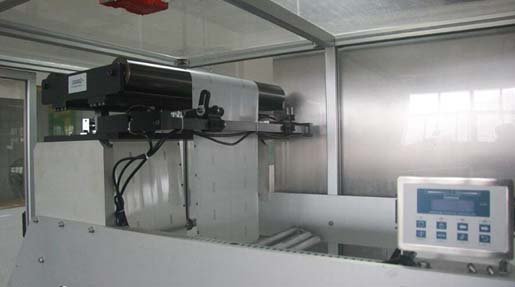
Present the approved roll, control tension, detect film condition and keep the web aligned through the forming path.
Register artwork
Coordinate print marks, indexed length, seal positions and cutting references within the validated film and speed window.
Form the pouch
Create the bottom fold or gusset, apply zipper or other approved features and build the side-seal geometry.
Cut and transfer
Separate the formed pouch and place it into the horizontal gripper path without losing alignment or opening access.
Open and verify
Use the configured vacuum and mechanical action to open the pouch, then confirm the required condition before filling.
Fill and settle
Meter the product with the project-matched filler while protecting the seal area and allowing the required settling time.
Seal and cool
Apply the approved temperature, pressure, dwell and cooling sequence for the chosen laminate and contamination condition.
Inspect and release
Confirm the defined fill, pouch, seal, code and reject criteria before counting the output as an accepted pack.
See the station-by-station explanation in how a horizontal form fill seal machine works.
The pouch is created before it is filled
Roll condition, splice method, web width, laminate stiffness, print pitch, registration mark, sealant layer and coefficient of friction influence how the web runs. A generic sample roll cannot qualify a production film family.
Approve the controlled drawing
Freeze pouch width, height, gusset, seal widths, zipper or spout position, cut geometry, artwork and registration reference.
Define the supplied roll
Record roll width and diameter, core, winding direction, splice, laminate structure, thickness and allowable variation.
Trial production material
Run the intended film through startup, steady operation and changeover; record registration, scrap, seal and opening results.
HFFS, VFFS or premade pouch?
The three architectures do not become equivalent because they can package the same product. Compare the package presentation, dosing access, material economics, changeover and accepted output over the intended operating model.
| Decision | HFFS pouch system | VFFS bag system | Premade-pouch system |
|---|---|---|---|
| Package input | Roll film converted into a pouch through horizontal forming and transfer stations | Roll film formed around a vertical product path | Finished pouches supplied to the machine |
| Format strength | Integrated stand-up, zipper, spout or shaped pouch production when tooling and film are validated | Efficient pillow, gusseted and selected specialty bag routes depending on platform | Broad access to sourced pouch constructions without forming them on the machine |
| Main proof | Web control, forming, transfer, opening, filling and sealing as one sequence | Film pull, forming tube, dosing, longitudinal seal and cross seal as one sequence | Pouch feeding, pickup, true opening, gripping, filling and top presentation |
| Changeover focus | Film, forming tooling, pouch path, filler parts, closure options and first-off approval | Film, forming set, seal jaws, filler settings and first-off approval | Pouch magazine, grippers, guides, opening, filler parts and first-off approval |
| Commercial comparison | Normalize film or pouch cost, tooling, startup waste, labor, cleaning, changeover loss, accepted output, spare parts and downstream scope. | ||
For a neutral architecture decision, start with the HFFS vs VFFS comparison, then use the HFFS vs premade pouch machine comparison to decide between forming from roll stock and running supplied pouches. Review the premade pouch machine hub only after that route is fixed.
Dosing time often sets practical HFFS output
The horizontal pouch path creates filling access, but the filler must still meter the actual product within the available cycle and protect the pouch top. The selected architecture may use an auger, weigher or pump only after product behavior and dose have been reviewed.
Powders
Provide bulk density, flow, aeration, dust, stickiness, dose range and refill condition. Define dust control and seal-area cleanliness.
Granules
Provide piece size, fragility, flow, density, target weight and settling behavior. Confirm the weigher, platform and product-drop path.
Liquids
Provide viscosity, temperature, foam, splash, particles, stringing and cleaning requirements. Confirm tank, pump, valve and nozzle motion.
Pastes and inclusions
Define the complete particle and viscosity envelope. Sample testing is required to confirm passage, cutoff, pouch support and clean closing.
Choose the HFFS architecture before fixing a model
The references below are separate documented configurations, not one transferable specification. Final performance is controlled by the approved product, dose, film, pouch drawing, lane count, filler, options and FAT method.
HMK2000 stand-up pouch HFFS
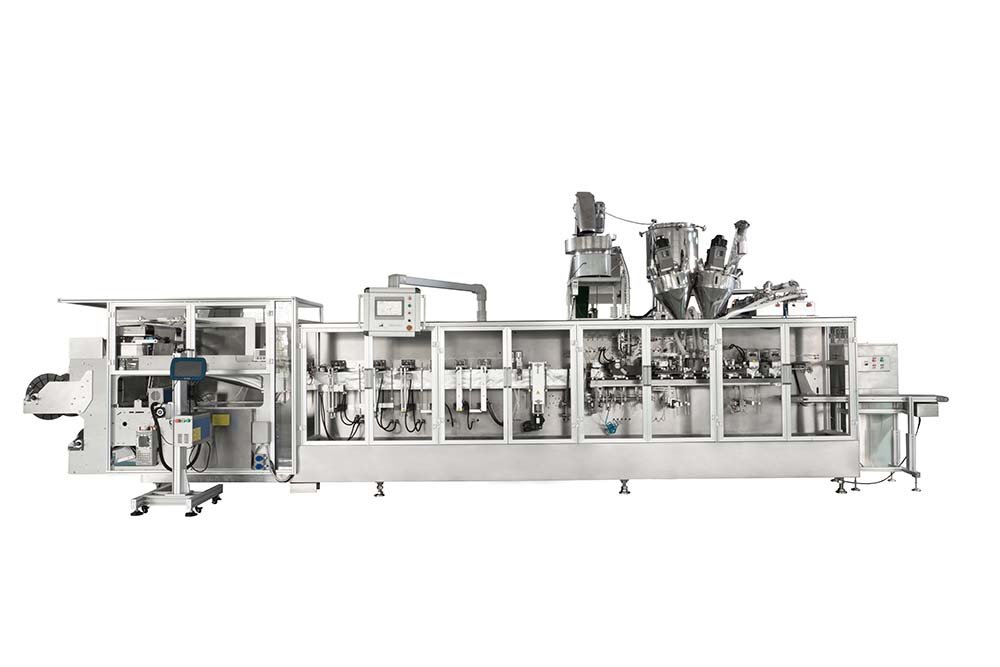
The documented HMK2000 reference covers standard Doypacks, zipper Doypacks and flat bags, with an indicative 20–40 bags/min range, pouch sizes from 80 × 120 mm to 200 × 300 mm and filling volume up to 1000 ml. Actual output must be confirmed with the product, film and accepted-pouch test.
Review HMK2000 specifications and scope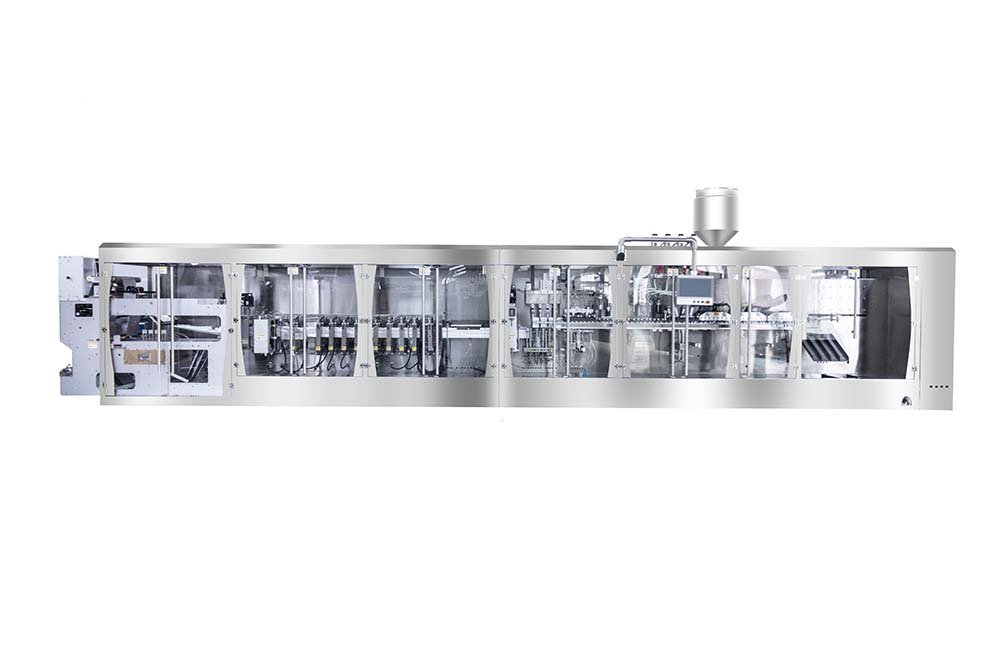
HMS320 full-servo top-spout route
The published HMS320 reference is a roll-film top-spout system for mayonnaise, ketchup, sauces and viscous liquids. Its page documents 90–160 mm pouch width, 120–300 mm pouch height and a project reference up to 70 pouches/min. Do not transfer that output to another product or package without a separate review and FAT basis.
Review the HMS320 project referenceHMK420Q four-station high-speed HFFS
The documented HMK420Q quotation reference is a four-station tomato-paste or purée configuration for bottle-shaped Doypacks or flat bags of 120 g or less, with 160–200 bags/min quoted for that agreed application. Other products, contours, closures and fillers require a new controlled scope.
Review the HMK420Q reference boundaryA good-looking seal is not enough
Seal release must connect the laminate, sealant layer, temperature, pressure, dwell, cooling and expected contamination condition to an agreed test method. Visual appearance alone cannot prove the package will perform through handling and distribution.
Define the window
Record the process range that produces acceptable seals instead of relying on one nominal temperature setting.
Challenge realistic contamination
Where the product can reach the seal area, reproduce the defined condition and agree how affected packs are evaluated.
Retain traceable evidence
Keep material identification, settings, samples, results and deviations linked to the approved configuration.
Specify accepted output instead of empty-cycle speed
Freeze the production basis
Name the product, dose, pouch, film, closure, run duration, operators, refill method, allowed rejects and downstream condition.
Find the real constraint
Measure filling time, pouch opening, settling, sealing, cooling, inspection and discharge rather than assuming transport is the bottleneck.
Select lane architecture
Add working stations only when the filler, pouch path, cross-lane quality, cleaning and maintenance access can support them.
Use the pouch packing line bottleneck analysis to identify the first limiting process and distinguish starvation, blocking, rejects and downstream loss before changing the HFFS speed target.
Send the information that changes the HFFS system
| Input | What to provide | Decision affected |
|---|---|---|
| Product | Representative sample, physical behavior, operating temperature, density or viscosity, pieces, dust or splash and cleaning requirement. | Filler, hopper or tank, product path, dosing time, protection and contact scope. |
| Dose and output | Nominal and range, tolerance method, accepted packs/min, run duration, refill condition and reject allowance. | Filler capacity, station count, lane balance, buffers and FAT pass criteria. |
| Pouch drawing | Width, height, gusset, seals, contour, zipper or spout, hole, coding area and finished-pack requirements. | Forming, cutting, tooling, transfer, opening, filling access and changeover. |
| Roll film | Web width, core, roll diameter, winding, structure, thickness, artwork, print pitch, registration, splice and samples. | Unwind, guiding, registration, forming, sealing, startup scrap and material approval. |
| Site and interfaces | Layout, electrical supply, air, product feed, coding, inspection, reject, discharge, secondary pack and line controls. | Machine layout, utilities, controls handshakes, included equipment and responsibilities. |
| Documents and service | Destination, required drawings, manuals, records, training, commissioning, spares and commercial handover terms. | Project boundary, lead activities, FAT evidence, delivery and lifecycle support. |
Turn the application into measurable acceptance
Approve inputs
Identify product batch, film roll, closure components, pouch drawing, configuration, utilities and operating basis.
Run the full sequence
Include startup, steady production, refill, defined stops, restart and any changeover required by the purchase scope.
Inspect agreed defects
Check fill, dimensions, registration, pouch opening, seal, closure, appearance, coding, reject logic and downstream handoff.
Close evidence
Retain settings, counts, results, samples, video, alarms, deviations, open items and responsible parties before shipment.
Use the stand-up pouch machine FAT checklist to define the acceptance record before the factory test begins.
Protect output after the first accepted run
Changeover control
List the required film, forming, zipper or spout, gripper, filler, cleaning and first-off tasks for each approved format family.
Preventive maintenance
Connect inspection and service tasks to the actual unwind, transport, vacuum, sealing, cooling, filler and safety configuration.
Critical spare parts
Separate commissioning spares, wear parts and business-critical components using failure evidence, lead time and production consequence.
Control the decisions around the HFFS machine
Horizontal form fill seal machine FAQ
What packages can a pouch HFFS machine make?
Depending on the confirmed platform and tooling, it may form standard stand-up pouches, zipper Doypacks, spout pouches, flat bags or shaped pouches from roll film. Each format requires an approved drawing, material, forming path, opening access and acceptance test.
Is HFFS the same as a premade pouch machine?
No. HFFS forms the pouch from roll film before filling. A premade-pouch machine receives an already manufactured pouch and must feed, grip, open, fill and close it. Compare material supply, tooling, changeover, waste, labor and accepted output before choosing.
Can one HFFS machine pack powder, granules and liquid?
A platform may be paired with different filling technologies, but a delivered configuration is approved for defined products and formats. Product behavior, filler timing, contact parts, dust or splash control, cleaning and sealing must be confirmed for every application family.
How fast is a horizontal form fill seal machine?
There is no useful universal speed. The published INMAYPACK references range from an HMK2000 planning range of 20–40 bags/min to an application-specific four-station HMK420Q quotation reference of 160–200 bags/min. Accepted output must be tied to the actual product, dose, pouch, film, lane count, test duration, rejects and downstream condition.
What determines HFFS machine price?
Price changes with pouch dimensions and features, forming and cutting tooling, filler, station or lane count, zipper or spout equipment, coding, inspection, utilities, controls interfaces, documentation, FAT, delivery, commissioning and spare-parts scope. Compare quotations only after those boundaries are normalized.
What samples are needed before quotation?
Send the real product, controlled pouch drawing, production film or complete material specification, closure components where applicable, dose range and an accepted-output target. Also provide site utilities, upstream and downstream interfaces, destination requirements and the required test evidence.
Define the pouch, film and product before pricing the machine
Start with your product, finished pouch format, fill weight or volume and required accepted packs per minute. Send the information you have so we can review the forming and filling route. Film drawings, utilities and detailed acceptance requirements can follow.
Detailed HFFS project checklist
Send your product behavior, dose range, pouch drawing, roll-film specification, closure components, accepted output, site utilities and downstream condition. INMAYPACK will review the appropriate HFFS architecture and identify the information still required for a scoped proposal.