Use this route for a roll-stock top-spout project
The reviewed HMS320-2 configuration forms the pouch from roll film, opens it, fills the product, inserts and welds the spout, applies the cap and cools the final seal within one horizontal system.
Packaging systems configured around your application Defined project scope

A full servo horizontal form-fill-seal (HFFS) doypack machine that forms, fills, caps and seals top-spout stand-up pouches from roll film. The reviewed reference configuration is for mayonnaise and ketchup applications.
Output scope: The 70 pouches/min value describes a reviewed mayonnaise/ketchup top-spout reference configuration. The source proposal states that actual speed depends on the filling material. Final accepted output also depends on dose, viscosity, pouch and spout geometry, cap handling, splash control and FAT conditions.
Get a Free Quote WhatsApp Us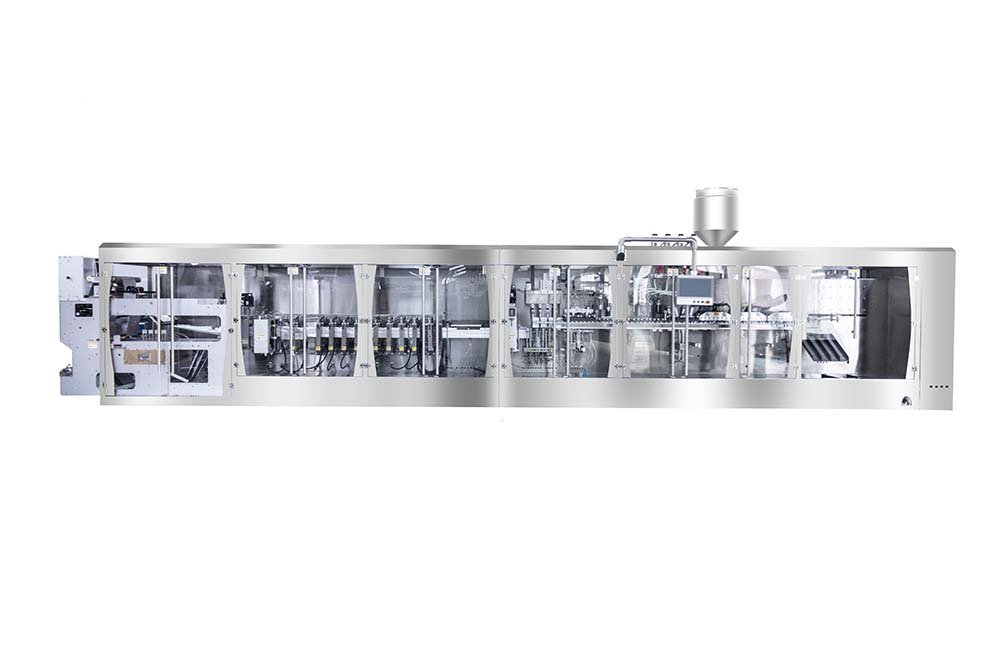
The HMS320 is a full servo doypack packing machine from INMAYPACK in Shanghai, China. The reviewed HMS320-2 reference forms top-spout pouches from roll film and integrates filling, spout welding, capping and seal cooling in one horizontal line. Its submitted project range covers 90–160 mm pouch widths and 120–300 mm pouch heights, with a reviewed output value of up to 70 pouches per minute. Final accepted output is established with the confirmed product, dose, pouch, spout and FAT conditions.
Start with the product, finished pouch and accepted output. “Full servo” describes the motion and control architecture; it does not by itself prove that a filler, spout, cap or seal process fits every application.
The reviewed HMS320-2 configuration forms the pouch from roll film, opens it, fills the product, inserts and welds the spout, applies the cap and cools the final seal within one horizontal system.
The source project uses two micro servo rotor-pump fillers for pumpable liquids and pastes without solid particles. Viscosity alone is not enough: send product temperature, solids, fibers, aeration, shear sensitivity, dose range and cleaning requirements.
Provide the production film structure, pouch drawing, roll direction, spout drawing, cap sample and tamper-evident requirements. Welding, opening and capping cannot be released from nominal pouch width alone.
The reviewed project value is up to 70 pouches/min and explicitly depends on the filling material. Contract output should be expressed as accepted finished pouches under an agreed product, dose, package and FAT method.
Choose another route when required: a premade spouted pouch, a side-spout geometry, a product containing particles, a non-pumpable powder or granule, or a pouch outside the submitted size range may require different handling, filling or sealing equipment. These are engineering inputs, not automatic HMS320 options.
Full servo doypack packing machine specifications — model HMS320-2 duplex configuration.
| Parameter | HMS320-2 Specification |
|---|---|
| Machine type | Horizontal form fill seal (HFFS) full servo doypack packing machine |
| Pouch styles | Top-spout doypack, stand-up pouch, 3-side seal, 4-side seal |
| Min. pouch size (W×H×Bottom) | 90 × 120 × (25×2) mm |
| Max. pouch size (W×H×Bottom) | 160 × 300 × (45×2) mm |
| Packing speed | Reviewed project value: up to 70 pouches/min; accepted output depends on product, dose, pouch, spout and FAT conditions |
| Filling system | Micro servo rotor pump, 26 ml/rev, 10–2000 RPM, viscosity 0–5000 cps, CIP-compatible, 316L contact parts |
| Voltage / Power | AC380V, 50/60 Hz, 35 kW |
| Air consumption | 0.6 m³/min |
| Noise level | < 75 dB |
| Machine dimensions (L×W×H) | 9500 × 1400 × 2000 mm |
| Net weight | 6000 kg |
| Frame & contact parts | SUS304 frame; product-contact parts SS304 / 316L |
Specification scope: These values describe the reviewed HMS320-2 duplex reference configuration. Confirm the final machine, filler, utilities, materials and accepted output in the issued proposal and FAT protocol.
The reviewed component schedule uses the brands listed below. Final brands, models, substitutions and supporting compliance documents must match the approved quotation and as-built handover package.
| Component | Brand |
|---|---|
| HMI screen / Servo motor / PLC / Frequency converter / Low-voltage & safety electric | Schneider Electric (France) |
| Pneumatic components | Festo (Germany) & AIRTAC |
| Main axis encoder | OMRON (Japan) |
| Photoelectric sensors | Pepperl+Fuchs (Germany) / KEYENCE (Japan) |
| Proximity switches | Pepperl+Fuchs (Germany) |
| Linear guides & lead screws | HIWIN (Taiwan) / NADELLA (Germany) |
| Bearings | SKF / THK / IKO / Igus |
| Vacuum pump (bag opening) | Schmalz (Germany), oil-free, Hygiene oriented |
The process must remain stable across all six handoffs. A problem at an upstream station can appear later as an opening, filling, seal or cap reject.
Feed the approved roll film, monitor film presence and correct lateral position before forming.
Create the specified bottom and pouch geometry while controlling tension, registration and transport.
Use vacuum and opening assistance so each mouth is presented consistently to the filling nozzles.
Coordinate the rotor-pump discharge, nozzle cutoff and optional nitrogen step with pouch position.
Feed the confirmed spout and cap, then control welding position and capping torque for that component set.
Cool the seal, inspect the agreed quality conditions and transfer only accepted pouches downstream.
The reviewed configuration coordinates six process areas to form, open, fill, weld, cap and cool top-spout doypacks in one horizontal line.
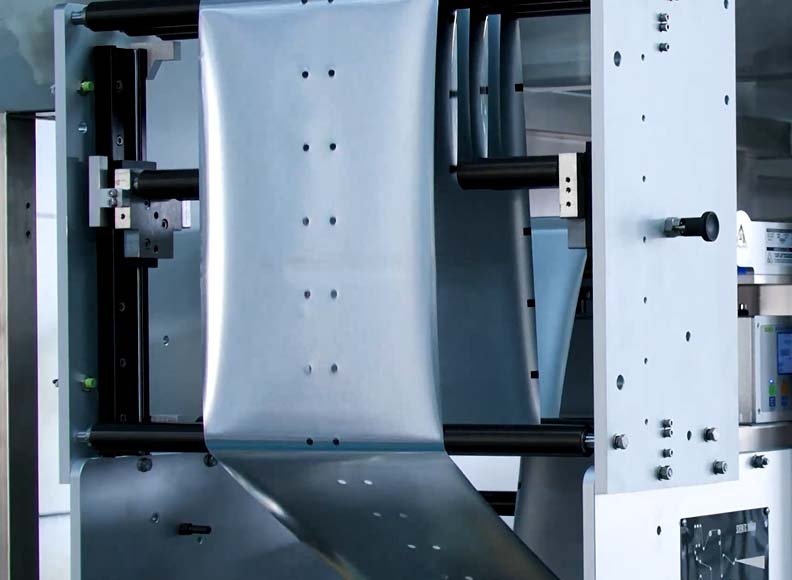
Servo film traction combines edge alignment, no-film detection, bottom punching and an inline UV exposure module before pouch forming. UV dose, microbial effect and validation requirements must be confirmed for the submitted film, line speed and customer process.
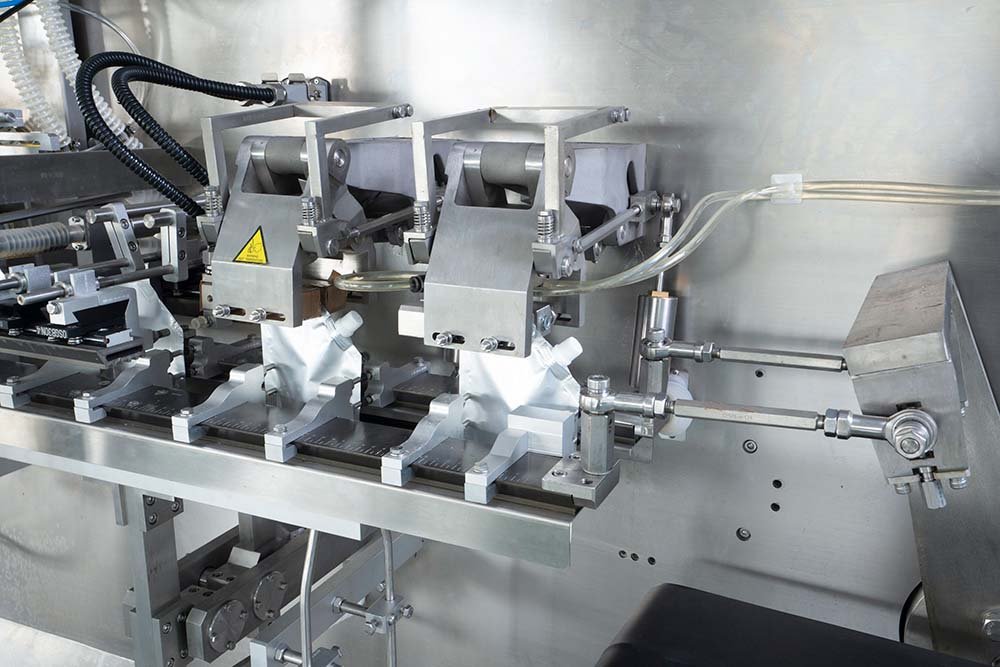
The reviewed configuration combines anti-drip nozzles, oil-free vacuum bag opening, nitrogen flushing and a rotor-pump filling circuit. CIP connection, cleaning sequence, materials and acceptance criteria must be confirmed for the submitted product and plant utilities.
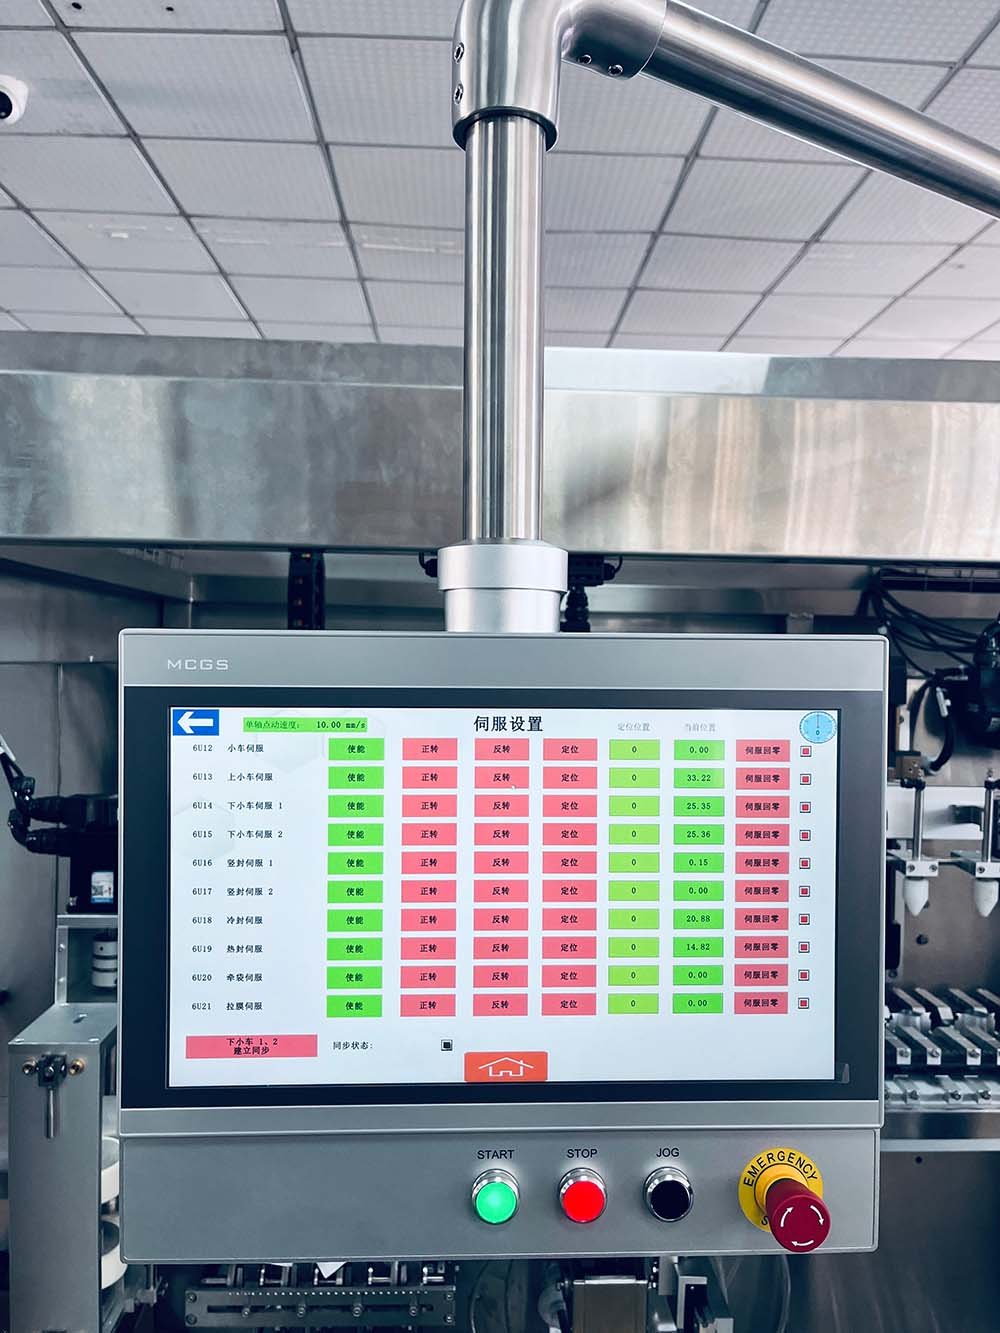
The reviewed configuration uses Schneider servo motors, motion control, PLC and HMI. Touchscreen recipes support controlled changes to approved operating parameters; changeover time and repeatability must be verified with the confirmed formats during FAT.
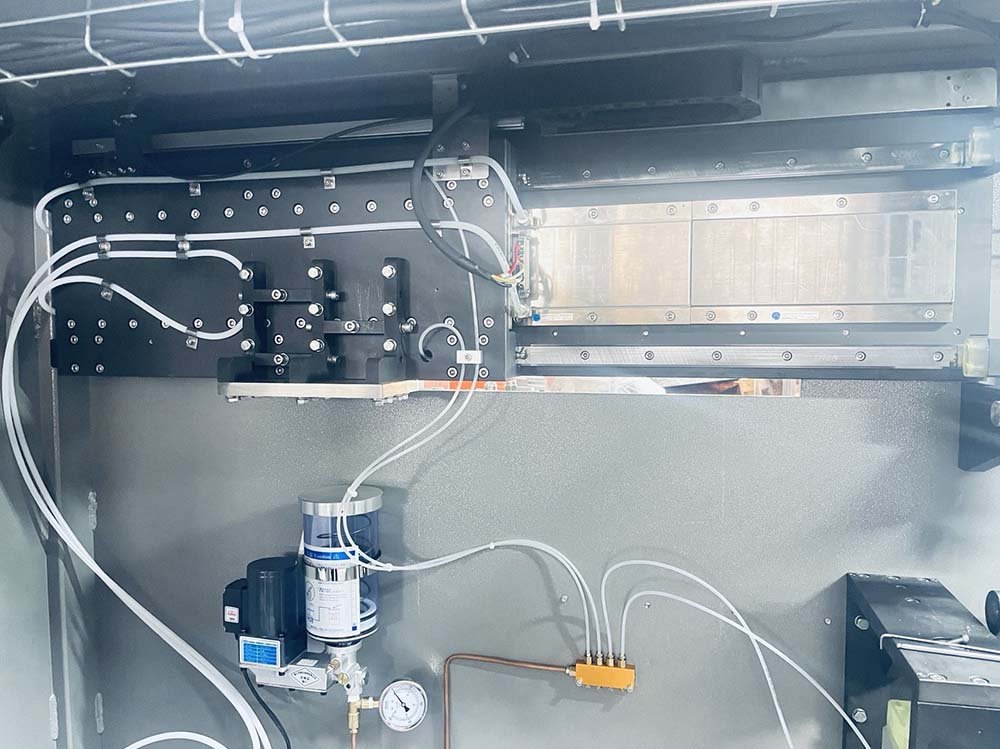
The reviewed transport arrangement uses linear-servo pouch grippers, adjustable bag-width settings, specified guides and bearings, and a lubrication system. Inspection, cleaning, lubrication where specified and wear-part replacement remain part of the approved preventive-maintenance plan.

The reviewed spout-feeding and servo-capping arrangement uses controlled feeding and programmable torque limits. Any feeder rating is a component value, not accepted pouch output; cap, spout and tamper-evident-ring performance must be validated with submitted samples during FAT.
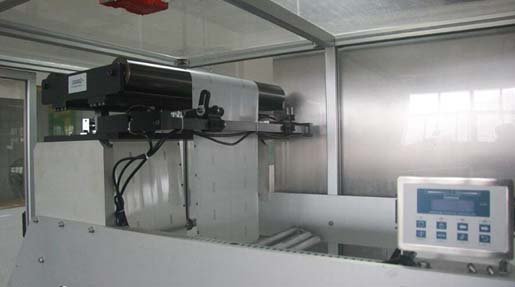
Spout-sealing and top-seal cooling modules control the sealing sequence and pouch discharge condition. Seal integrity must be accepted against the agreed test method using the confirmed pouch, spout, product and operating window.
A useful quotation connects product behavior to filler selection and connects the pouch material to a measurable seal-acceptance method.
HMS320 is a roll-stock HFFS reference. A project using purchased premade pouches follows a different feeding, opening and sealing path. Compare the premade pouch packing machine route before requesting the HMS320 configuration.
See the full servo doypack packing machine forming, filling, spout-welding and capping top-spout pouches on a real production line.

HMS320 full servo top-spout doypack packing machine — live running video by INMAYPACK
The reviewed rotor-pump project range covers liquids and pastes up to 5000 cps. Product behavior, dose, temperature, solids, cleaning requirements and accepted output determine the final filling configuration.

INMAYPACK is a packaging-machinery brand based in Shanghai, China and established in 2009. Its product scope includes sachet, roll-stock doypack, premade-pouch and coffee-capsule packaging systems configured around the approved application.
The proposal total is meaningful only when every supplier prices the same forming, filling, spout, inspection, testing and handover scope.
| Scope item | What the quotation should state | Evidence before release |
|---|---|---|
| Main HMS320 configuration | Exact model, duplex arrangement, confirmed pouch range, frame and product-contact material by location | Approved configuration sheet and as-built equipment list |
| Filling system | Pump model and quantity, tank, feed boundary, nozzle arrangement, product limits and cleaning connection | Product trial, dose record and cleaning demonstration as agreed |
| Spout and cap handling | Component drawings, feeder, insertion, welding, capping, torque basis and included change parts | Approved samples plus witnessed feed, weld and cap checks |
| Coding and inspection | Printer, code verification, checkweigher, leak or seal checks, reject method and reject confirmation | Seeded-fault tests and accepted/rejected count reconciliation |
| Line interfaces | Upstream product supply, downstream conveyor, permissives, blocked/starved behavior, utilities and guarding boundary | Interface list, cause-and-effect check and coordinated restart test |
| Delivery and support | Incoterm, destination, production timing, FAT attendance, documents, spares, training, commissioning and exclusions | Issued quotation, contract and handover register |
Commercial boundary: the historical project proposal includes project-specific prices and terms. They are not a current public offer. HMS320 cost, warranty, delivery, payment and service obligations must come from the issued quotation for the confirmed configuration and destination.
The factory acceptance test should reproduce the agreed product and packaging conditions closely enough to prove the configuration—not merely show that the machine can cycle.
Record product lot and temperature, dose, film roll, pouch drawing, spout and cap samples, installed options, recipe, run duration and permitted operator interventions.
Count accepted pouches separately from startup material, empty cycles, rejects, rework and planned test stops. State the calculation and the conditions beside the result.
Check dose, opening, registration, spout position, weld, cap application, seal condition, coding and reject handling using the agreed sampling and test methods.
Witness film end or loss, missing pouch or fill condition, feeder interruption, alarm handling, controlled restart and first-off inspection where included in the scope.
Use the agreed SKU transition to record parts, recipe control, drain or recovery, cleaning access, inspection and the first accepted pouch after restart.
Retain samples, settings, alarm and test records, drawings, backups, manuals, spare-parts list, training evidence and a dated deviation/retest register.
Use the full-servo doypack URS and FAT guide to turn the confirmed product, pouch, output and evidence requirements into a supplier comparison. If the machine later develops recurring defects, follow the stand-up pouch machine troubleshooting workflow before changing several settings at once.
A short message saying “sauce pouch machine” is not enough to release a configuration. Send the following package so the filler, pouch path and commercial boundary can be reviewed together.
Quick answers about the HMS320 full servo doypack packing machine.
Tell us your product, dose, pouch, spout, cap and target accepted output. INMAYPACK will review the applicable configuration and define the quotation, test and delivery boundary.
Get a Free Quote Now