
Food packaging seal integrity testing should prove more than a pouch looking closed. A useful control plan connects the approved laminate and package geometry to clean seal presentation, heat, pressure, dwell, cooling, sampling and a test method that can detect the failure being controlled.
This guide is for packaging, quality, engineering and procurement teams comparing stand-up pouch, flat sachet and premade-pouch processes. It explains what to measure, when to sample and what evidence to request before accepting a packaging machine.
Quick answer: use visual inspection to find visible defects, a controlled seal-strength method to measure separation force and failure mode, and an appropriate leak method to investigate channels or gross leaks. Define the specimen, conditioning, apparatus, test pressure or rate, units and acceptance rule before comparing results. There is no universal sealing temperature or pass value for every laminate and pouch.
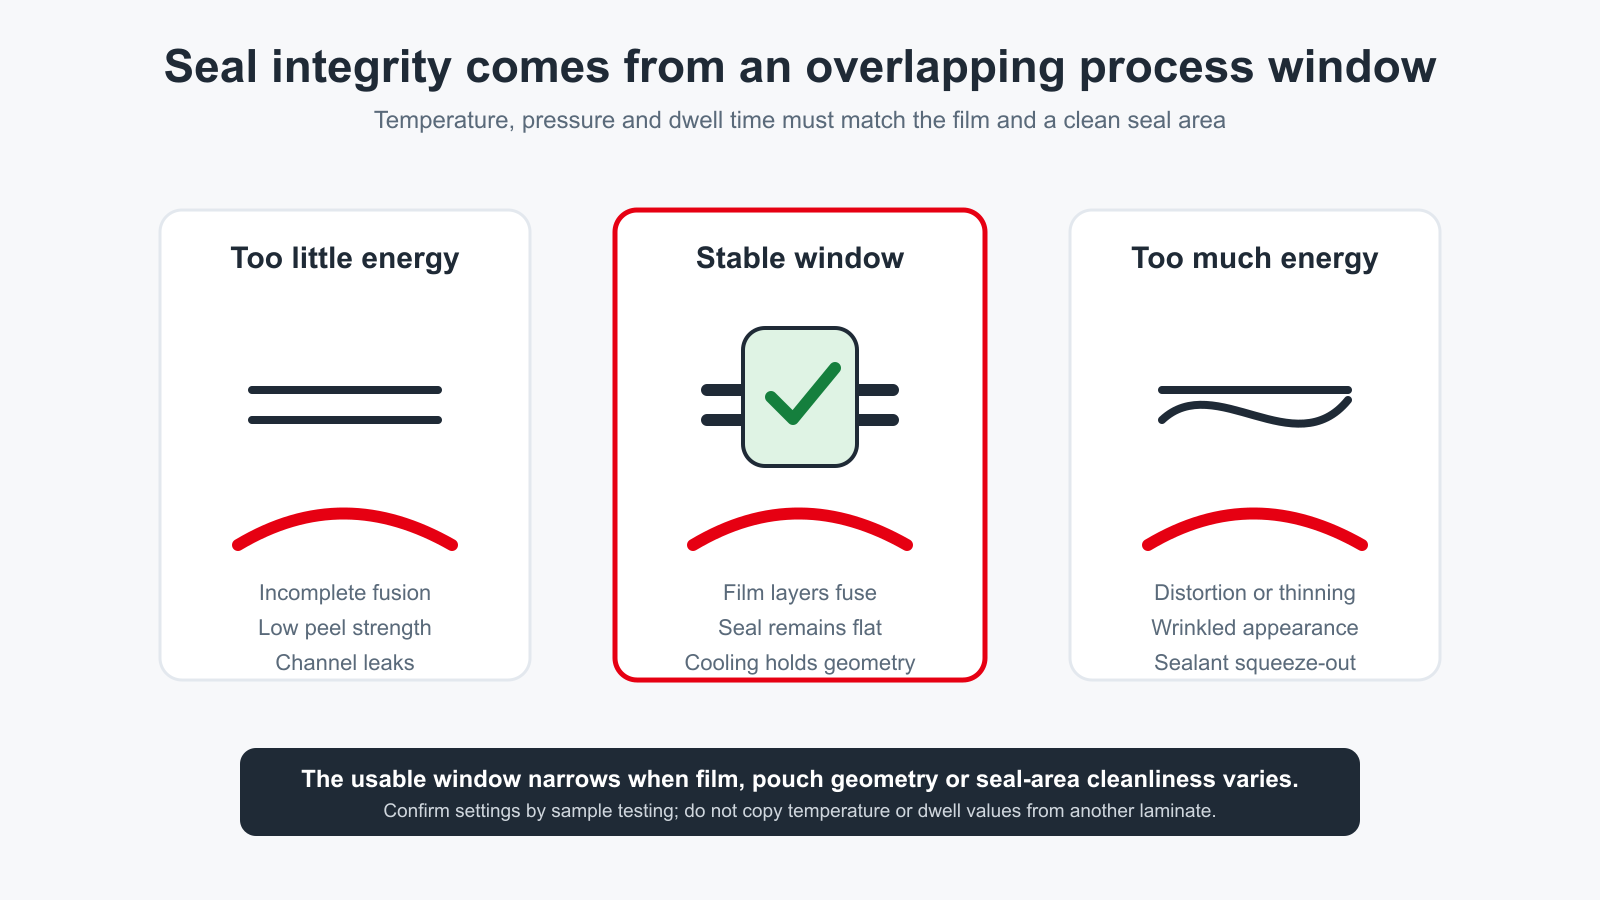
What should seal integrity testing prove?
A seal can look uniform and still contain a narrow channel. It can also have a high peel force while failing through film tear, delamination or another mode that does not match the approved package specification. For that reason, “seal integrity” should be separated into several questions.
Continuity
Is the seal band continuous, or is there a channel, wrinkle, fold, particle or damaged area that creates a leak path?
Strength and failure mode
What force separates the seal specimen, and does the specimen peel at the interface, tear through the film or fail elsewhere?
Package function
Does the finished package remain acceptable through cooling, handling, accumulation and the defined downstream process?
Process stability
Do results remain inside the approved limits after warm-up, stops, film changes, refills and normal operating disturbances?
The packaging specification should identify which of these questions matter for the product and distribution route. A destructive peel test cannot replace every leak test, and a bubble test does not establish seal strength. Use complementary methods only when each method has a defined decision role.
Build the sealing process window before setting acceptance limits
The machine, film and product behave as one system at the seal. Changing one input can move the usable window even when the pouch dimensions remain the same.
- Laminate and sealant: record the approved construction, sealant side, nominal thickness, coating or adhesive changes and the film lot used for validation.
- Seal-area presentation: control product dust, oil, liquid splash, wrinkles, gusset folds, zipper transitions, spouts and any feature crossing the seal band.
- Heat input: evaluate the actual production condition after thermal stabilization. The displayed setpoint does not by itself prove temperature uniformity at the jaw face.
- Pressure distribution: inspect jaw parallelism, wear, release surfaces and the support behind the seal. Local pressure loss can create a local channel.
- Dwell and line speed: record the operating recipe and the event that controls contact time. A result developed at one cycle condition should not be assumed at another.
- Cooling and handling: define when the hot seal first carries product load or downstream tension. A seal may deform after leaving the jaws if it is loaded before it is adequately supported.
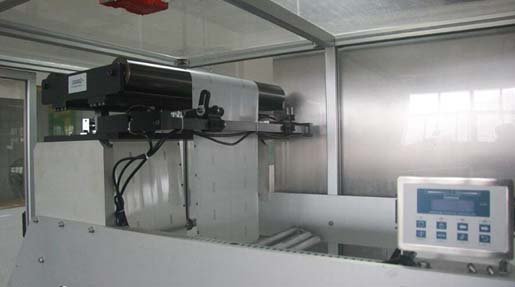
Choose a test method that matches the failure risk
The method name is not enough. The procedure, specimen location, conditioning and acceptance rule must be stated so results can be compared between a supplier trial, factory acceptance test and production quality check.
| Method | Question answered | What must be defined | Boundary |
|---|---|---|---|
| Visual inspection | Are wrinkles, burns, contamination, incomplete bands, folds or distorted transitions visible? | Lighting, defect examples, locations and disposition rule | Does not quantify seal strength or reliably reveal every channel |
| ASTM F88/F88M | What force separates a flexible-barrier seal, and what failure mode occurs? | Specimen width and location, conditioning, grip separation rate, tail technique and reporting units | Results from different techniques should not be compared as if they were the same setup |
| ASTM F2096 | Does internal pressurization reveal a gross leak by bubble emission? | Package preparation, immersion, pressurization, test pressure and observation rule | Destructive; method suitability and sensitivity depend on the package and procedure |
| ASTM F3039 | Does dye penetration reveal a channel in nonporous packaging or flexible barrier material? | Dye solution, application location, contact time and acceptance rule | Destructive and limited to the method's applicable package/material conditions |
| Production handling challenge | Does the sealed package remain acceptable through cooling and the agreed downstream route? | Line condition, duration, sample points, handling boundary and defect criteria | Not a substitute for a defined laboratory or leak method when one is required |
Acceptance values belong to the approved package specification. Do not copy a seal-strength value, leak-test pressure or temperature from another laminate, pouch size or test setup. Use supplier data and trials to establish candidates, then confirm the production window with the actual approved materials and documented methods.
Sample the events most likely to move the result
A single sample taken after the line has settled can miss the conditions that create intermittent defects. The sampling plan should cover normal production and the disturbances that buyers expect the machine to recover from.
- Startup and thermal stabilization. Separate cold-start samples from samples taken after the jaw system reaches the agreed stable condition.
- Normal sustained production. Collect samples across the agreed run, not only from the beginning or from one convenient lane.
- Film roll, pouch magazine or material lot changes. Preserve traceability to the roll, pouch lot and machine recipe.
- Product refill and supply variation. Check whether dust, splash, foam, stringing or particle distribution reaches the seal area.
- Stop and restart events. Record how the line handles material held near heated jaws and which packs are rejected after recovery.
- Changeover and cleaning release. Confirm jaw setup, pouch guidance, recipe selection and clean seal presentation after the approved changeover procedure.
- Downstream accumulation or interruption. Observe whether hot seals are compressed, bent, pulled or loaded before the agreed cooling point.
Diagnose the failure before changing the recipe
| Observed result | Possible mechanism | Evidence to retain |
|---|---|---|
| Low separation force across the full specimen | Insufficient fusion, unsuitable material pair, inadequate dwell or pressure, or a test-setup difference | Film and pouch lot, specimen location, conditioning, machine recipe, test technique and failure mode |
| Local channel or intermittent bubble location | Particle, wrinkle, gusset fold, zipper/spout transition, jaw damage or uneven pressure | Marked leak location, magnified seal image, lane or station, jaw-face condition and matching production event |
| Scorching, thinning, distortion or sealant squeeze-out | Excess heat or pressure, long dwell, inadequate cooling or unstable material presentation | Sample sequence, actual operating condition, speed, stop history and downstream load point |
| Acceptable at low speed but unstable at production speed | Reduced dwell, changed heat balance, filler timing, pouch movement or insufficient cooling time | Comparable samples at both conditions, recipe values, temperature trend and event timing |
| Failures concentrated after refill or cleaning | Contamination, trapped moisture, incomplete setup release or a recipe/change-part mismatch | Release checklist, product supply condition, sanitation/changeover record and first-off samples |
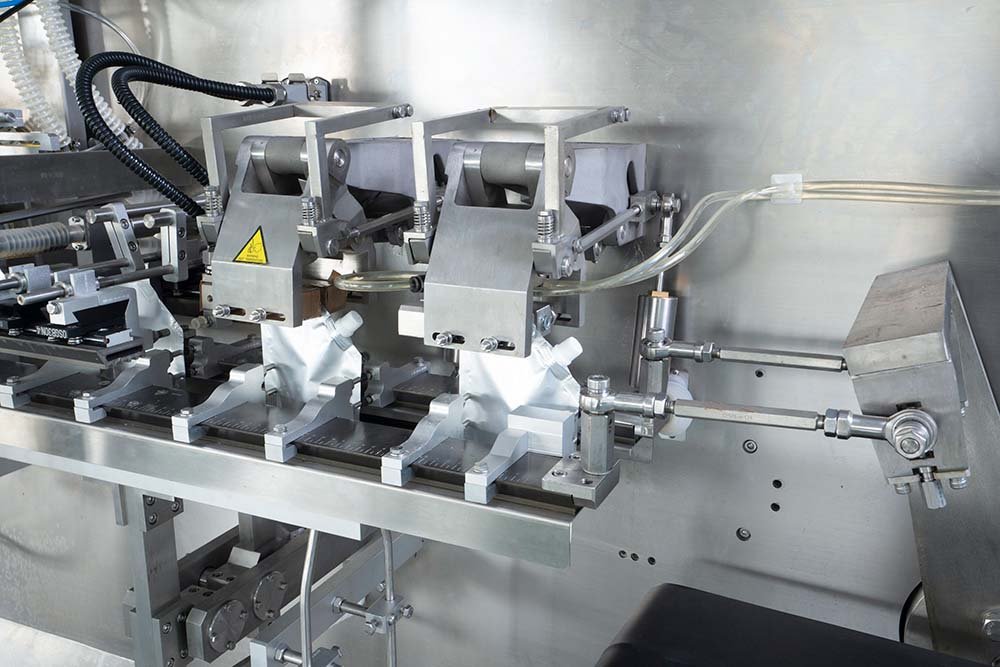
Adjust the control plan for HFFS and premade-pouch machines
Both architectures need an approved package specification, stable seal-area presentation and defined testing, but their disturbance sources differ.
| Control point | Roll-stock HFFS | Premade-pouch system |
|---|---|---|
| Incoming material | Film structure, web width, print registration, winding, splice and coefficient-of-friction behavior | Pouch construction, sealant orientation, opening, zipper/spout position, stack condition and lot consistency |
| Geometry creation | The machine forms the pouch and creates longitudinal/bottom/top seals according to the configured process | The converter supplies most pouch geometry; the machine must grip, open, fill and close the supplied pouch consistently |
| Common presentation risks | Web tracking, forming alignment, registration, folds and tension variation | Pickup variation, pouch deformation, incomplete opening, product contamination and top-seal alignment |
| Traceability emphasis | Film roll, splice, printed repeat, recipe, lane and forming/sealing station | Pouch lot, magazine load, station, recipe, opening/filling event and top-seal result |
Use the HFFS vs premade pouch machine guide when the package supply architecture is still open. For roll-stock projects, the HFFS film specification guide explains the information that should reach the machine supplier before trials.
Turn seal testing into an RFQ and FAT requirement
“No leaks” is not a complete acceptance criterion. A supplier needs enough information to reproduce the package task and to know how the buyer will judge the result. Include the following in the request for quotation and factory acceptance protocol:
- approved laminate or premade-pouch specification, drawing, critical seal bands and representative production samples;
- product condition at filling, including temperature, viscosity, particles, dust, oil, foam or other contamination risks;
- package size range, fill range, zipper or fitment locations and planned SKUs;
- target operating condition and the definition of conforming finished packs per minute;
- test methods, specimen locations, sample count, conditioning, units and acceptance rules;
- events that must be challenged, such as warm-up, refill, stop/restart, changeover and downstream interruption;
- required records: recipe, material lot, test result, failure mode, rejected packs, stops and corrective action.
The stand-up pouch machine FAT checklist can be used to connect this seal plan with pouch forming or handling, dosing, coding, inspection and sustained accepted output. For machine-level troubleshooting after release, use the HFFS stand-up pouch troubleshooting workflow.
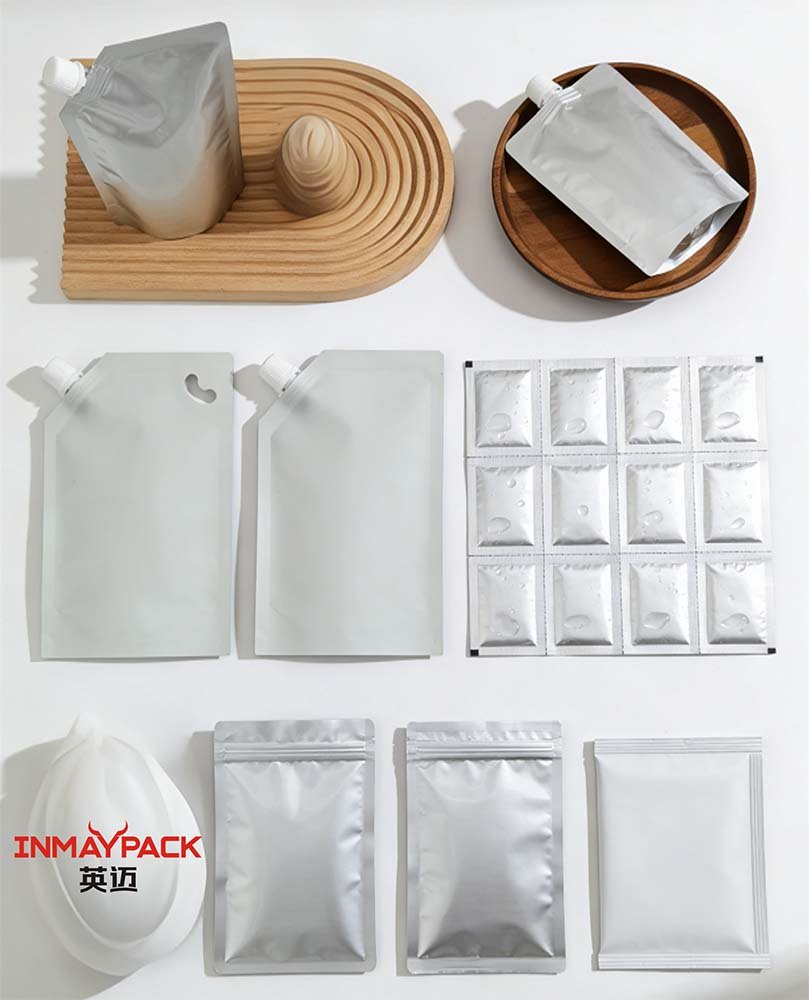
Seal integrity questions buyers should settle before approval
Is visual inspection enough for pouch seal integrity?
Visual inspection is useful for visible wrinkles, burns, contamination and incomplete seal bands, but it does not quantify separation force or reveal every narrow leak path. Add a strength or leak method when the package specification requires evidence for that risk.
What is the correct sealing temperature for a stand-up pouch?
There is no universal value. The usable condition depends on the approved laminate and sealant, thickness, jaw design, pressure, dwell, speed, contamination, cooling and package geometry. Establish and document the window with the actual material and process.
Does a stronger seal always mean a better package?
No. Strength must be considered with failure mode, continuity, package opening requirements and the behavior of the surrounding material. A result outside the approved specification can be unsuitable even when the measured force is high.
Should every pouch be leak tested?
The quality plan should define the method, sample frequency and disposition rule from the product and package risk. Some methods are destructive and therefore suited to samples rather than every pack. Do not invent a universal frequency without the buyer's quality basis.
What samples should be sent to the machine supplier?
Send representative production material, package drawings, good and failed examples when available, product at the intended filling condition and the current test protocol. Identify lots and explain any planned supplier, layer, thickness, zipper or fitment alternatives.
Related packaging engineering guides
Technical references
- ASTM International, F88/F88M Standard Test Method for Seal Strength of Flexible Barrier Materials.
- ASTM International, F2096 Standard Test Method for Detecting Gross Leaks in Packaging by Internal Pressurization (Bubble Test).
- ASTM International, F3039 Standard Test Method for Detecting Leaks in Nonporous Packaging or Flexible Barrier Materials by Dye Penetration.
Review the seal evidence for your pouch project
Send the approved laminate or pouch drawing, product condition, target output, current test method and representative samples. The INMAYPACK Engineering Team can review the machine boundary and identify which inputs still need confirmation before a quotation or FAT plan is fixed.







