
A multihead weigher and a linear weigher both portion product before packaging, but they do not create the portion in the same way. The useful comparison starts with product behavior, target weight, giveaway, accepted output, cleaning and the downstream package—not head count alone.
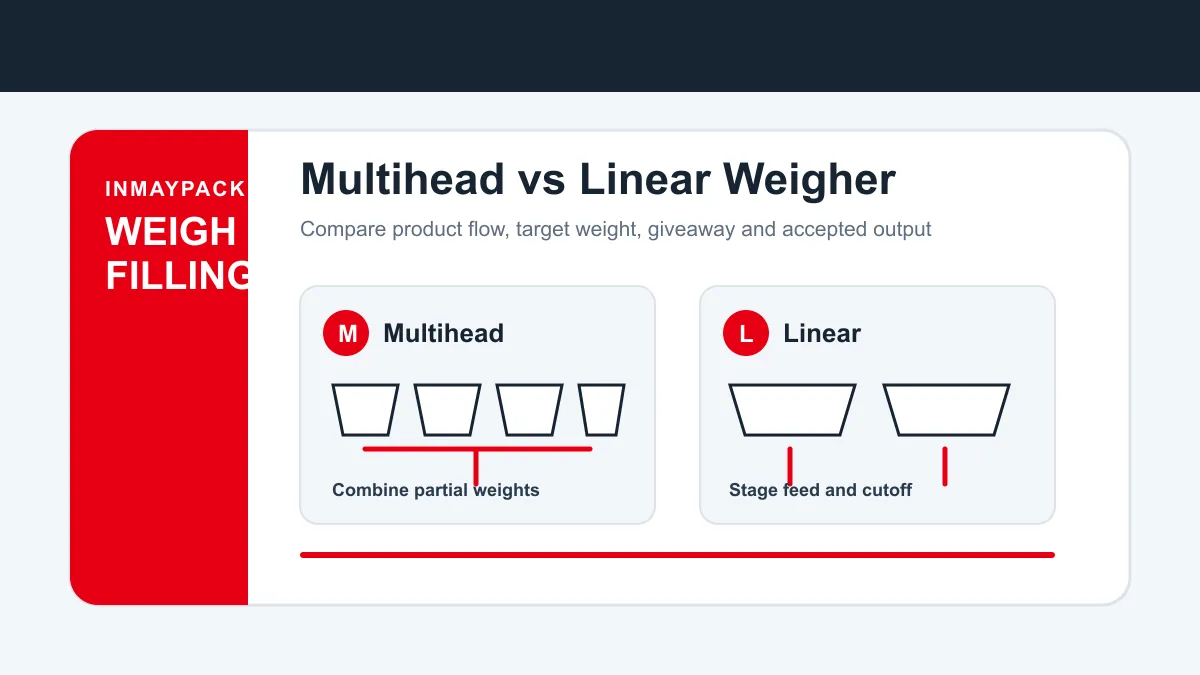
Neither route is automatically more accurate for every product. Compare accepted finished packs produced under one documented product, refill, package and test condition.
Direct comparison
Multihead vs linear weigher at a glance
The table describes operating principles and selection questions. It is not a performance promise for an unconfirmed INMAYPACK configuration.
| Decision point | Multihead combination weigher | Linear weigher |
|---|---|---|
| How the portion is formed | Several weigh hoppers hold partial quantities; the controller selects a combination that approaches the target. | One or more linear channels feed product toward a target, normally using staged feed and cutoff control. |
| Typical reason to evaluate it | Higher required throughput, tighter giveaway control, mixed pieces or a wide range of discrete food products. | Simpler dry-product dosing, moderate output, fewer channels or a project where straightforward change and access matter. |
| Product presentation | Needs stable central distribution to radial feeders, pool hoppers and weigh hoppers. | Needs repeatable flow along linear pans or channels without bridging or uncontrolled afterflow. |
| Main sizing variables | Head count, hopper volume, target weight, average piece volume, combinations available and discharge pattern. | Channel count, pan geometry, coarse/fine feed settings, target weight, cutoff behavior and discharge arrangement. |
| Common risk | Poor distribution leaves too few useful combinations or damages fragile and coated pieces. | Slow cutoff, dribble, bridging or density changes increase cycle time and weight variation. |
| Integration question | Can the pouch machine receive each combined discharge at the required timing and opening condition? | Can the package remain available while the sequential weigh cycle completes and discharges cleanly? |
| Evidence required | Finished-pack trials using the real product, target, refill method, packaging machine, reject rule and agreed test duration. | |
Do not select from the word “accurate.” Ask each supplier to state the product condition, target weight, sample method, giveaway calculation, speed basis and whether the reported result is measured at the weigher or on accepted finished packs.
Operating principle
Follow the product through the complete weighing cycle
The portion result begins before the load cell and continues after discharge. A capable weigher can still underperform when its infeed starves, its chute damages product or the package is not ready.
Product behavior
The same product name can require a different weigher
Test the hardest saleable condition, not only the easiest sample. Oil, seasoning, frost, fines, static, breakage and density variation can change feed and cutoff behavior.
Free-flowing pieces
Nuts, candy, beans, cereal pieces and many dry snacks can suit combination weighing. Confirm piece dimensions, bulk density and the number of useful hopper combinations at the target weight.
Small uniform granules
A linear or volumetric route may deserve comparison when the product flows consistently and the required output is moderate. Final choice still depends on acceptable giveaway and cutoff behavior.
Sticky or coated products
Gummies and oil- or seasoning-coated products may cling to pans and hoppers. Review surface treatment, feeder motion, door timing, cleaning and restart after a short stop.
Fragile pieces
Chips, crackers and brittle products need controlled vibration, drop height and transfer. Record breakage and fines as quality results, not only net weight.
Frozen or moist pieces
Frost, free water and temperature drift can create clumps and buildup. Confirm sanitation, drainage, contact time and the condition used during the trial.
Powders and liquids
Do not force either dry-piece weigher route onto fine powder, liquid or paste. Compare an auger filler or a product-matched pump where appropriate.
Weight acceptance
Separate target accuracy from product giveaway
A portion can fall inside the allowed range and still create avoidable giveaway. Define the legal or commercial minimum, permitted distribution, sampling rule and reject treatment before suppliers tune for speed.
Use one approved scale and sampling procedure to compare the in-process weigher result with the net content of finished packs. Include tare variation, product loss between discharge and package, and rejected packs.
Record these results
- Mean finished-pack net weight
- Minimum and maximum sampled value
- Standard deviation or agreed spread measure
- Underweight and overweight count
- Average giveaway above the commercial target
- Product lost or retained in the transfer path
- Rejected packs and their cause
- Test duration and refill events
The pouch machine must be ready for every discharge
A fast isolated weigh cycle does not create saleable output when a pouch is missing, incompletely opened or still sealing. I would compare both weighing routes only after each supplier documents the product feed, discharge chute, pouch-ready signal, hold logic, rejects and recovery sequence. The accepted rate belongs to the complete line.
Packaging integration
Match the weighing route to the package architecture
Roll-film HFFS pouch
The pouch is formed before opening and filling. Coordinate weigher discharge with pouch transfer, opening confirmation, fill access and top-seal cleanliness.
Premade pouch
A supplied pouch is picked and opened before the portion arrives. Pouch stiffness, zipper behavior, opening success and drop distance can limit useful output.
Sachet or stick pack
Small roll-film packs and multi-lane systems use another dosing and web architecture. Do not treat a multihead weigher as a universal substitute for lane-specific dosing.
Selection worksheet
Send the inputs that can change the answer
| Input | What to provide | Decision affected |
|---|---|---|
| Product | Samples, photos, piece size range, bulk density, coating, moisture, temperature, fragility and fines. | Feeder, surface, hopper or channel geometry, vibration, drop and cleaning. |
| Portion | Target weight, range, tolerance, giveaway objective and production recipes. | Head or channel count, hopper volume, combination availability and cutoff control. |
| Output | Required accepted packs per minute or hour, shift pattern, refill method and allowable rejects. | Weighing cycle, buffering, downstream capacity and test duration. |
| Package | Drawing, material, dimensions, opening, zipper or closure, fill level and samples. | Chute, discharge timing, drop height, contamination and sealing recovery. |
| Hygiene | Allergens, cleanout method, wash requirements, change frequency and inspection points. | Contact construction, removable parts, access, drainage and changeover scope. |
| Line controls | Upstream feed, pouch-ready signal, hold, faults, inspection, rejects, counts and data needs. | Interface list, permissives, recipe ownership, recovery and FAT challenges. |
Factory acceptance
Use one test basis for both proposals
Before the run
Freeze the product batch and condition, target, package, refill method, equipment boundary, inspection rule, duration and accepted defects.
During the run
Record weight samples, giveaway, starvation, buildup, product damage, missed discharges, pouch faults, rejects, stops and recovery.
At release
Compare good finished packs per hour and the approved weight distribution. Keep weigher cycles, pouch cycles and accepted packs as separate counts.
Source-backed INMAYPACK boundary: one reviewed pouch-line proposal includes a 14-head, 1.6 L multihead reference with stated theoretical weigher values. Those values are not transferred to a linear weigher or to a new product. Reconfirm the exact model, product, target, packaging machine and FAT result in the issued project documents.
Buyer questions
Multihead and linear weigher FAQ
What is the main difference between a multihead and linear weigher?
A multihead weigher selects a combination of partial weights held in several weigh hoppers. A linear weigher normally feeds product along one or more channels toward the target using staged feed and cutoff control. The suitable route depends on the product, target, output and accepted-pack test.
Is a multihead weigher always more accurate?
No. Combination selection can provide strong speed and giveaway control for suitable discrete products, but distribution, target weight, hopper loading, product behavior and setup determine the result. Compare finished-pack data under the same production conditions.
When should a linear weigher be evaluated?
Evaluate it when a simpler feed-and-cutoff arrangement may satisfy the dry product, target weight, moderate output and cleaning requirements. Confirm afterflow, bridging, density variation and actual pack results rather than relying on the lower component count.
Can both systems pack snacks, candy and granules?
They may be considered for some overlapping products, but suitability is not decided by the category name. Piece size, oil, coating, stickiness, fragility, fines, target weight and required rate change the correct configuration.
Does weigher speed equal packaging-line speed?
No. Accepted output is limited by product supply, weighing, discharge, pouch availability, filling, sealing, inspection and recovery. Count accepted finished packs over an agreed period.
What should I send for a comparison?
Send representative product, target weight and tolerance, pouch drawing and samples, required good-pack output, refill method, cleaning plan, upstream and downstream conditions, utilities and the FAT evidence you need.
Related reading
Continue with the confirmed product and package
Primary technical references
Sources used for the operating framework
- Ishida, Multihead Weigher Range Brochure — product flow through distribution, pool hoppers, weigh hoppers, combination selection and timed discharge.
- Ishida, multihead and linear weighing range overview — application-specific weigher families and selection boundaries.
- Yamato Scale, EPSILON multihead weigher — feeder, hopper and product-handling features in a commercial combination-weigher design.
These third-party manufacturer sources explain established weighing principles. They do not establish an INMAYPACK model, output, accuracy, supplied scope or commercial promise. Confirm every project fact in the INMAYPACK quotation, technical documents and FAT record.







