
A horizontal form fill seal machine converts roll film into a pouch, controls that pouch through opening and filling, then completes the final seal and discharge. On a pouch-forming HFFS line, the web moves through a horizontal sequence while the formed pouch normally remains upright for filling.
The useful explanation is not simply “form, fill and seal.” Every station must hand a controlled condition to the next: aligned film, repeatable pouch geometry, a verified open mouth, protected seal area, correct dose and a finished pack that meets the agreed acceptance test.
Confirm which horizontal form fill seal process is being discussed
The HFFS label is used for more than one material path. A flow wrapper forms a film tube around a horizontally presented product. A pouch-forming HFFS machine creates an empty pouch from roll stock, separates or transfers it, opens it, fills it and seals the remaining edge. This guide focuses on the second route.
Form the package before filling
Roll film is guided, folded or gusseted, sealed and cut into pouch geometry. The pouch is then controlled through opening, filling, top sealing, cooling and discharge.
Form film around the product
An oriented product travels on an infeed while film forms a tube around it. A longitudinal seal and transverse end seals complete the pack. Use the flow wrap packaging guide for that route.
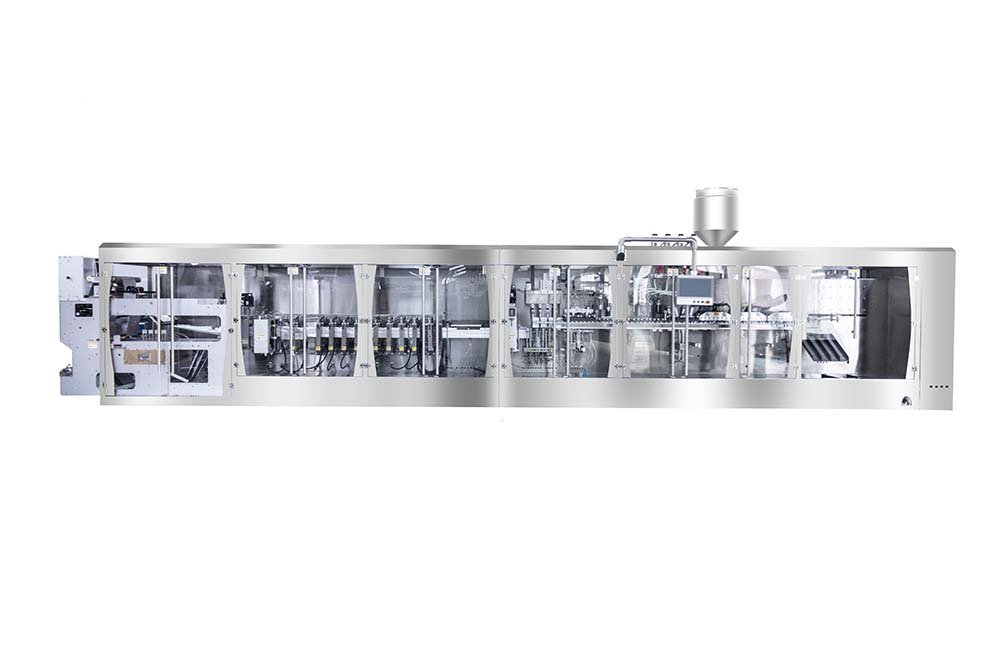
Follow the film from unwind to accepted pouch
Machine designs vary, but the working principle can be reviewed as ten linked functions. A stable downstream station cannot permanently correct an unstable condition created upstream.
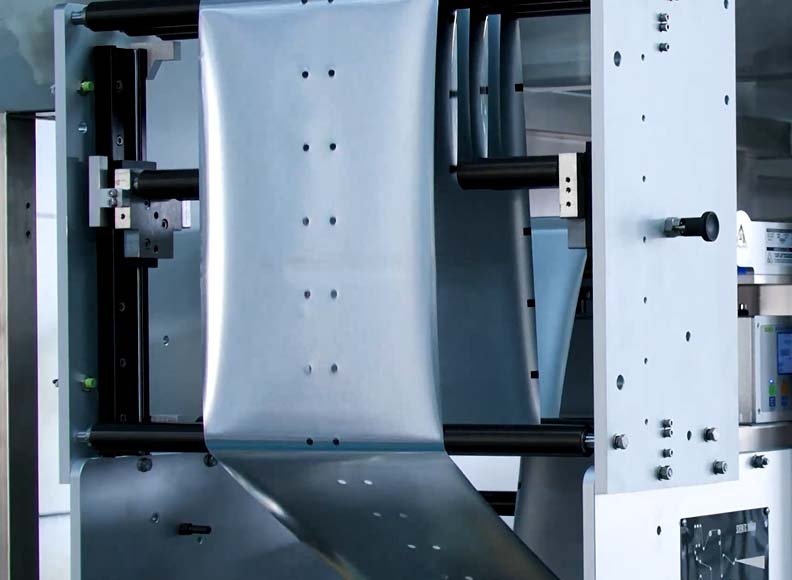
Unwind and tension the film
The approved roll is mounted, routed and presented at controlled tension. Roll diameter, core, splice, winding quality, friction and laminate stiffness affect how the web enters the machine.
Guide and register the web
Edge control and print-mark registration keep artwork, seal zones, notch positions and cut references aligned with machine pitch. Correction must remain within the usable movement range.
Create the pouch geometry
The web is folded or formed to the approved flat or stand-up shape. Bottom-gusset geometry, zipper, fitment or contour operations require application-specific tooling and film behavior.
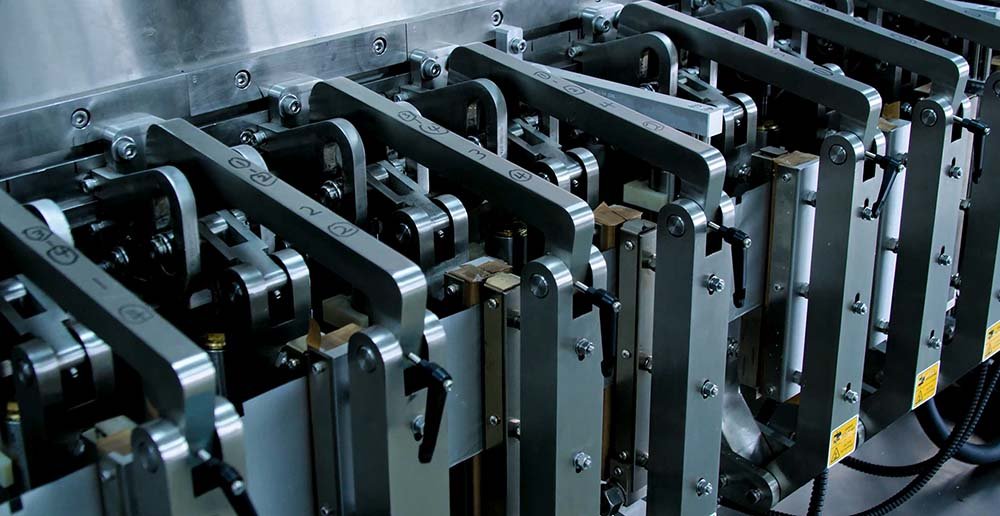
Make the required preliminary seals
Bottom, side or feature seals establish the pouch body before product is introduced. Temperature, pressure, dwell, cooling, material condition and contamination determine the usable sealing window.
Index, pull and cut
The machine advances one controlled pitch and separates the formed pouch where required. Pulling, cutting and registration must preserve the geometry needed by the transfer and opening stations.
Transfer and grip the pouch
Grippers or carriers take the pouch without losing height, squareness or mouth access. Grip position must tolerate the real pouch and film variation without marking or dropping it.
Open and verify the mouth
Vacuum cups, mechanical assistance or air may separate the pouch panels. The system should verify the required open condition before permitting the filler to discharge.
Dose the product
The selected pump, auger, weigher, cup or other filler delivers the controlled dose. Nozzle motion, product cutoff, dust, drip, splash, aeration and settling affect both output and seal-area cleanliness.
Close, seal and cool
The filled pouch mouth is presented flat and clean. The final seal is made and cooled according to the approved laminate and product condition before the pouch loses support.
Inspect, reject and discharge
The line applies the agreed presence, code, weight, metal, seal or other checks, confirms rejection where required and releases accepted pouches to collection or downstream equipment.
See the HFFS machine components map for a station-by-station hardware view and the horizontal form fill seal machine family for the commercial system boundary.
The control system coordinates references, not isolated devices
Servos, sensors, pneumatic devices, temperature control and the filler must act against one indexed or continuous timing model. A local device can be functioning correctly while the overall handoff is mistimed.
Know where film and pouch are
Encoder position, registration correction, gripper position and station pitch must describe the same physical package.
Use process interlocks
No pouch, failed opening, missing product condition or downstream block should produce an uncontrolled fill or release.
Control the approved setup
Format-specific timing, temperature, motion, filler and inspection settings need controlled identities and release checks.
Motion architecture changes the available process window
In an intermittent system, the web or pouch stops for selected forming, sealing, filling or cutting actions. In a continuous system, part of the process occurs while material remains in motion. The correct choice depends on package geometry, filler behavior, seal time, handling stability and accepted output.
| Decision point | Intermittent motion | Continuous or rotary section |
|---|---|---|
| Process time | Station dwell can be easier to isolate and adjust. | Actions must remain synchronized through movement. |
| Filling | A stationary pouch may simplify some dosing tasks. | Filler and package motion need a compatible delivery window. |
| Sealing | Jaw contact occurs during a defined stop. | Seal tooling follows or rotates with the material path. |
| Output | Cycle time includes stop, actuation and restart. | Higher mechanical throughput may be possible when every handoff remains stable. |
| Proof | Compare accepted pouches under the same product, film, format, refill, reject and downstream conditions. | |
Use the continuous versus intermittent motion guide for the shared decision principles, while keeping HFFS pouch transfer and opening requirements separate.
Trace a finished-pouch defect back through the handoffs
| Observed result | Review upstream | Evidence to retain |
|---|---|---|
| Cut or print position drifts | Roll condition, tension, web guide, registration mark, encoder and pull mechanism. | Film lot, mark signal, correction trend, pitch measurement and affected time. |
| Pouch does not open | Cut geometry, panel blocking, static, zipper or gusset condition, transfer height, vacuum and suction-cup contact. | Failed pouch sample, lot, station state, vacuum reading and opening response. |
| Product reaches the seal | Opening, nozzle position, filler cutoff, dust or drip, product settling and pouch support. | Product condition, dose, timing, nozzle state, contaminated sample and reject result. |
| Top seal is weak or wrinkled | Mouth presentation, contamination, laminate, jaw condition, temperature, pressure, dwell and cooling. | Film lot, settings, seal samples, test method and lane or station identity. |
| Accepted output is below target | Refills, film splice, opening failures, filler recovery, rejects, downstream blocking, stops and restart. | Gross cycles, accepted pouches, rejects by cause, stop log and test duration. |
A top-seal problem may begin with film tracking, pouch transfer, incomplete opening or filler cutoff. Isolate the first handoff that leaves the approved condition.
Test the complete horizontal form fill seal system
A dry cycle can show motion but cannot prove the real product, film, forming, filling and sealing process. The FAT should use approved or production-representative inputs and count conforming finished pouches.
Fix the trial basis
Record product condition, dose, film lot, roll data, package drawing, format parts, filler, recipe, utilities and downstream state.
Include real interventions
Observe refill, roll splice where required, normal adjustments, reject events, stop and restart rather than selecting only a short steady sample.
Apply agreed tests
Check dose, appearance, dimensions, registration, closure or fitment, code, seal continuity, leakage or strength by the defined method.
Report accepted output
Separate gross cycles, conforming pouches, rejects by cause, stops and recovery. State the duration and any excluded time.
Use the doypack film specification guide to prepare roll data, the seal integrity guide to define evidence and the RFQ builder to organize supplier inputs.
Production stability depends on the approved operating window
A horizontal form fill seal system is not released by finding one setting that makes one acceptable pouch. Production needs an operating window that tolerates the normal variation of film, product, refill, temperature, format parts and upstream or downstream behavior. The project team should define which changes require adjustment, verification or a new trial.
Control more than nominal thickness
Record structure, supplier, coefficient of friction where relevant, stiffness, seal initiation and usable sealing range, print repeat, roll build, splice and storage condition. A replacement roll that meets only width and thickness may still track, form or seal differently.
Define the condition at filling
Density, particle distribution, viscosity, temperature, aeration, dust, oil, static, fragility and particulates can change dosing and contamination. The accepted range belongs in the trial plan rather than remaining an operator assumption.
Release the first conforming pouch
Identify the format parts, recipe, forming and seal checks, filler verification, inspection challenges and retained first-off samples needed after a product or pouch change. Measure the complete return-to-production time.
Test stop and restart behavior
Film cooling, product held in the filler, partially formed pouches, material at the jaws and downstream blockage can change the first packs after a stop. Define how the machine clears, restarts and releases production.
Compare one issued system boundary
If the buyer is still choosing between roll-stock forming and purchased pouches, use the HFFS versus premade-pouch guide. For cost comparison, normalize the complete boundary with the doypack machine price guide.
Horizontal form fill seal machine FAQ
What does a horizontal form fill seal machine do?
It converts roll material into a package through a horizontal material path, coordinates product filling and completes the required seals. On a pouch-forming HFFS system, the machine forms an empty pouch, opens and fills it, then completes the final top seal.
Is an HFFS pouch machine the same as a flow wrapper?
No. Both may be called horizontal form fill seal equipment, but a flow wrapper forms film around a horizontally presented product. A pouch-forming HFFS machine creates a pouch before filling it. Procurement documents should name the real material path.
Which products can run on a pouch-forming HFFS system?
Liquids, pastes, powders, granules and pieces can be considered when the selected filler, product path, pouch support, seal protection and cleaning boundary match the application. Suitability requires representative product and film trials.
How should HFFS speed be measured?
Measure accepted pouches per minute for a defined product, dose, film, package, format, test duration, refill pattern, reject rule and downstream state. Empty cycles do not establish production output.
What information should be sent to an HFFS supplier?
Send product samples and condition limits, fill range, finished-pouch drawings, film specification and roll data, closure features, accepted output, package tests, cleaning needs, utilities, line interfaces, destination and required FAT evidence.
Sources used for the process framework
Industry definitions for horizontal form/fill/seal machines, pouch machines, flow wrappers and related equipment categories.
Reference sequence covering film unwind, pouch shaping, sealing, marking, pulling, cutting, opening, filling and closing.
Official machinery risk-assessment and risk-reduction principles. Project compliance remains configuration- and destination-specific.
Seal-strength test reference; the project must define sample preparation, conditioning, technique and acceptance limits.
Related HFFS guides and equipment
For powder applications, the powder filling guide explains the dosing system that works with the pouch former.
Discuss your product and pouch process
If a step in the process needs clarification for your application, share your product, pouch format and fill range with the INMAYPACK team.
Ask about your application






