
The right packaging machine is not selected from speed, bag width or price alone. It is selected by matching a defined product, an approved package, a controlled filling or feeding task, factory interfaces and an acceptance method to a suitable machine route.
This guide helps a project team compare VFFS, HFFS, premade-pouch, stick-pack, sachet, flow-wrap, capsule and cartoning routes without treating a brochure maximum as an accepted production result.
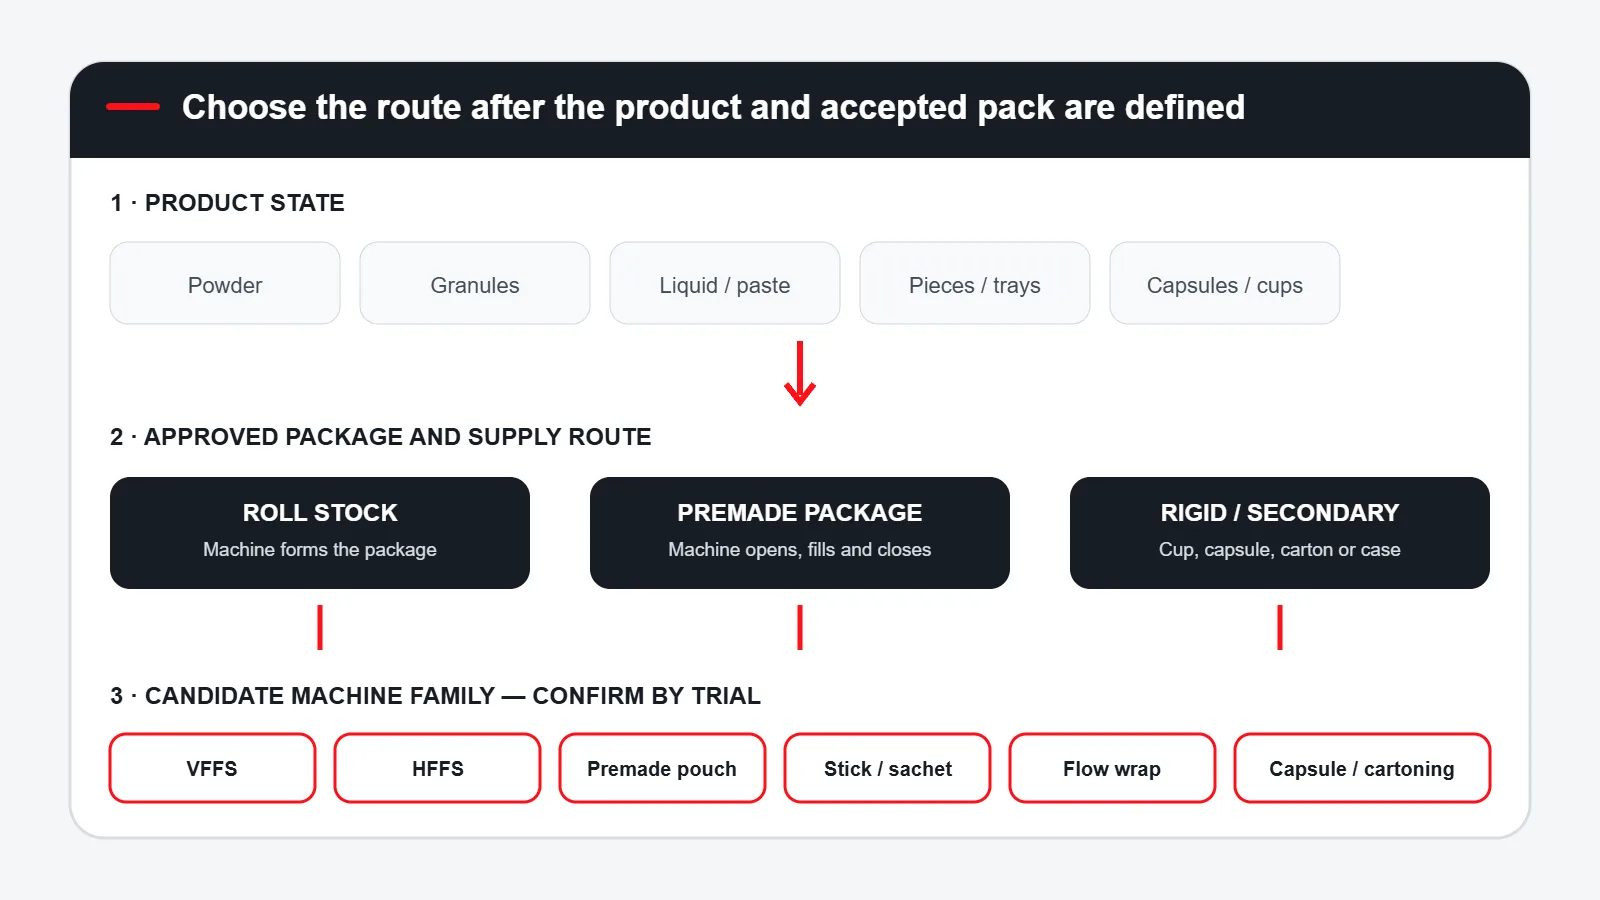
Define the accepted finished pack first, then document the product, dose, package material and supply route, required conforming output, factory interfaces and FAT method. Compare only machine proposals that cover the same boundary. Select the route that can demonstrate the required pack quality and accepted output under representative operating conditions.
If suppliers receive different product assumptions, package drawings or output definitions, their prices and speed claims are not comparable. The Packaging Machine RFQ Builder can standardize the first brief.
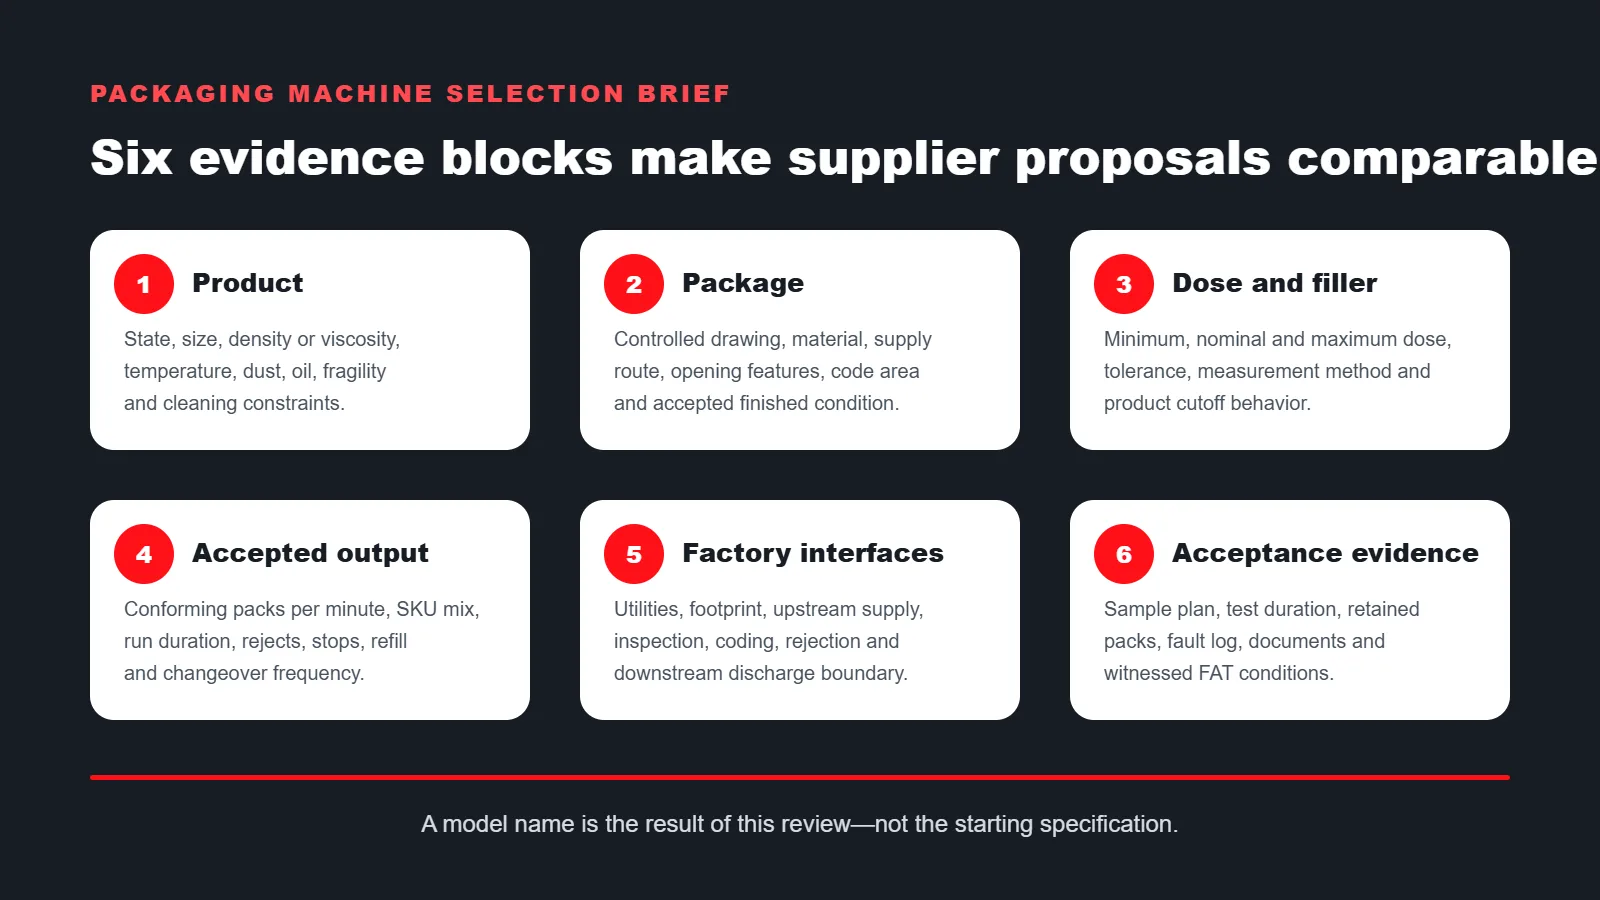
Define six decisions before requesting a machine model
A machine name is the result of the application review, not the starting specification. The following decisions prevent a familiar model from being applied to the wrong package or line condition.
Match the package supply route before comparing machines
Roll-stock equipment forms the package during production. Premade-package equipment receives a converted empty pouch, cup or capsule. Flow wrappers receive oriented products and wrap film around them. Cartoners handle a secondary package after the primary pack is ready. These routes assign different responsibilities to the converter, filler, feeder and packaging machine.
| Machine route | Typical starting material | Primary selection question | Relevant INMAYPACK page |
|---|---|---|---|
| Vertical form fill seal | Roll stock | Can gravity, dosing and product fall work through a vertical forming and sealing sequence? | VFFS machine guide |
| Horizontal form fill seal | Roll stock | Does horizontal pouch forming suit the required doypack geometry, filling access and sealing path? | Doypack packing machines |
| Premade pouch | Finished empty pouch | Can the system separate, open, grip, support, fill and close every approved pouch? | Premade pouch machines |
| Stick pack or sachet | Roll stock | Do lane count, dose, web width, seal map and cut method fit the small-format task? | Sachet packing machines |
| Horizontal flow wrap | Roll stock plus presented pieces | Can the infeed meter, space and orient the product before longitudinal and end sealing? | Flow wrap guide |
| Coffee capsule or cup | Rigid empty container and lid material | Are denesting, dosing, cleaning, lid placement and seal inspection defined by cavity or lane? | Coffee packaging machines |
| Cartoning | Flat carton blank plus primary packs | Can the product grouping, loading direction, leaflet, coding and closure be controlled? | Cartoning machines |
A machine family can also be ruled out early. Reject a route when it cannot accept the approved material, leaves insufficient access for the filler, cannot protect the product during transfer, requires an unsupported utility or cleaning method, or cannot connect to the required inspection and downstream equipment. Record the reason and the evidence used. This prevents a rejected route from returning later because a different supplier uses a more attractive model name or headline rate.
When the choice is specifically between roll-stock HFFS and converted empty pouches, use the HFFS versus premade-pouch comparison to assign material, forming, opening and changeover responsibilities.
The filler or feeder often sets the real line limit
The packaging machine cannot correct an unstable product supply by itself. Powder aeration, granule bulk density, liquid foaming, piece orientation, product temperature and refill behavior can change dose accuracy, seal contamination and usable speed. Select the filling or feeding method with the package route rather than adding it after the main machine is chosen.
Flow and dust
Record bulk density range, aeration, bridging, dust, moisture, oil and cleaning. Test cutoff and dust extraction with the intended dose and package opening.
Piece range and settling
Confirm the largest piece, fines, breakage, density, scale discharge, product fall, trapped product and how the fill settles before sealing.
Viscosity and cutoff
State temperature-dependent viscosity, particles, foaming, stringing, drip control, nozzle movement, cleanability and product recovery.
Presentation and spacing
Define orientation, pitch, contact, overlap, gaps, fragile surfaces, accumulation and reject logic before fixing the wrapper speed.
Container handling
Challenge denesting, empty-container detection, lane identity, fill cleanliness, lid placement, sealing and discharge.
Changeover boundary
List every priority SKU, required parts, recipe changes, cleaning, inspection reset and first-off approval after changeover.
Use the approved material and drawing—not a generic bag name
“Pouch,” “bag,” “sachet” and “film” do not define the sealant, stiffness, coefficient of friction, thickness, artwork repeat, eye mark, opening feature or converted tolerance. Send physical samples and a controlled flat drawing. For roll stock, include roll width, diameter, core, winding direction, splice and print registration. For premade pouches, include opening dimensions, zipper or fitment position, pouch-to-pouch tolerance and storage condition.
Package quality must be translated into measurable criteria. Seal strength, package leaks, visual continuity, dose, code, cut and dimensions answer different questions. The food packaging seal integrity guide explains how to keep these tests separate.
Compare accepted output instead of headline cycles
A cycle rate can be useful, but it is not the same as conforming finished packs per minute. A fair comparison must use the same product lot, target dose, package material, active lanes, inspection method, run duration, replenishment events and reject definition.
Record the reason for each reject and the time lost to stops, refill, film or pouch replenishment, cleaning, adjustment and downstream blocking. A short stable sample alone does not establish production behavior.
If the required machine speed was calculated without the filler, accumulation and downstream equipment, use the packaging line bottleneck analysis before increasing the headline speed requirement.
Define every interface that can stop or reject a pack
The quotation boundary should identify who supplies and integrates the filler, feeder, product elevator, conveyor, coder, vision system, checkweigher, metal detector, reject device, cartoner and case packer. State signal ownership, line control, emergency-stop zones, data exchange and the definition of a released finished pack.
Design for the installation site
Confirm voltage, frequency, phase, compressed air, extraction, nitrogen, water or cooling, ambient condition, washdown level, floor loading, access and maintenance clearance.
Fix accumulation and handoff
Define normal flow, starved and blocked behavior, buffer capacity, reject routing, discharge height, orientation, line speed signals and recovery after a stop.
For a multi-machine project, the turnkey packaging solutions page shows why interfaces, responsibilities and acceptance must be reviewed as one line.
Purchase price is one line in the machine cost
Compare the same scope: base machine, fillers or feeders, tooling, inspection, guarding, controls, documentation, freight, installation, commissioning, training and FAT. Then review material consumption, labor, utilities, change parts, cleaning time, planned maintenance, critical spares and expected downtime.
A lower initial quotation can become the higher-cost route when it excludes required interfaces or cannot demonstrate the agreed pack. A higher-speed route can also cost more per accepted pack if changeovers, material loss and line stops dominate the production mix. Use the VFFS cost guide for a worked framework, then adapt the categories to the selected machine family.
Send every supplier the same six evidence blocks
Attach product evidence
Provide data sheets, representative samples, condition ranges, minimum/nominal/maximum dose and the required measurement method.
Attach the package definition
Provide flat and filled drawings, complete material details, physical samples, all priority formats, code area and accepted finished-pack criteria.
State the operating requirement
Define conforming output, shifts, run length, replenishment, changeover frequency, sanitation, staffing and allowed rejects.
Mark every interface
Include layout, utilities, upstream and downstream equipment, signal list, inspection, rejection, documentation and site constraints.
Use FAT to test the promised boundary
The FAT protocol should name the approved product and packaging lots, installed configuration, recipes, run duration, sample frequency, measurement tools, defect criteria, stop and restart events, required documents and retained evidence. Record both accepted output and rejected packs by reason.
| FAT stage | Question | Evidence to retain |
|---|---|---|
| Configuration review | Does the installed BOM match the quotation, layout, utilities and interface list? | Approved BOM, drawings, photos, software and tooling identification |
| Material release | Are the product and package lots representative and traceable? | Lot details, condition, samples and deviations |
| Steady operation | Does the line produce conforming packs for the agreed duration? | Counts, time log, samples, test results, stops and interventions |
| Normal events | Can the line recover from refill, splice, replenishment, stop and restart? | Event log, first-off release, rejected quantity and corrective action |
| Closeout | Are open items, documents, training and site actions assigned? | Punch list, owner, due date, acceptance status and retained samples |
Avoid five shortcuts that make proposals look comparable
Selecting by speed first
Speed without product, package, filler, rejects and downstream conditions is not an accepted production commitment.
Using only bag dimensions
Dimensions do not define material, sealant, stiffness, opening features, tolerance, print registration or supply route.
Leaving the filler outside scope
Dose accuracy, cutoff, dust, foam, settling and product presentation can determine the usable line result.
Comparing unequal quotations
One supplier may include inspection, change parts, guarding or commissioning while another lists only the main frame.
Accepting a short demonstration
A brief clean run may not include material refill, thermal stabilization, restart, splice, blocked discharge or normal variation.
Keep one controlled brief
Issue the same revision to every supplier and track every confirmed value, exclusion, option, test condition and open item.
Packaging machine selection FAQ
Should I choose the package or the machine first?
Define the accepted product and package first, then select a machine route that can make or handle them. The package may still be refined during trials, but the project needs a controlled reference before proposals can be compared.
Is the fastest packaging machine usually the best choice?
No. The useful requirement is accepted output with the intended product, material, filler, inspection and downstream line. A slower headline rate may deliver a better result when changeovers, waste, rejects, cleaning or product handling dominate.
When should I choose roll stock instead of premade pouches?
Roll stock can suit high-volume forming routes and shifts package forming into the machine. Premade pouches transfer construction to a converter and can support distinctive formats, but the machine must reliably separate, open, fill and close the finished pouch. Compare both using the actual package mix and total cost.
What samples should be sent to a machine supplier?
Send representative product across the expected condition range, approved packaging material or pouch lots, flat and filled drawings, good and defective finished packs where available, and every priority SKU needed for selection and FAT planning.
What information is needed before a useful quotation?
At minimum: product condition, dose, package drawing and material, supply route, SKU list, accepted output, utilities, layout, interfaces, inspection, downstream scope and acceptance method. Mark unknowns as open items instead of allowing silent assumptions.
Sources used for the selection framework
Manufacturer reference that begins equipment selection with the application, package and container before presenting machine families.
Manufacturer guide distinguishing roll-stock form-fill-seal equipment from premade-pouch fill-and-seal machinery.
Industry reference explaining that acquisition and operating costs should be evaluated across the machine lifecycle, not by purchase price alone.
Manufacturer reference showing the relationship between roll-stock HFFS, product feeding, package format and line integration.
Move from selection to a controlled project brief
Send the product, package and accepted-output target
INMAYPACK will review the application boundary and identify which machine route, filling or feeding method, interfaces and trial evidence still need confirmation before a configuration is proposed.
Request a packaging application review






