Zipper Application on Roll-Stock Doypacks: Alignment, Sealing and Cutoff

A zipper that looks straight can still fail after filling. Reliable reclosure depends on the whole process chain: zipper unwind, profile orientation, flange presentation, registration, pre-sealing, end treatment, pouch forming and the relationship with the final top seal.
Quick answer: apply the zipper as a controlled secondary web. Keep its profile and flanges stable, register it to the pouch repeat, bond the correct flange areas without crushing the interlock, manage zipper ends where side seals cross extra layers, and validate both package integrity and repeated opening/reclosing with the actual film and product.
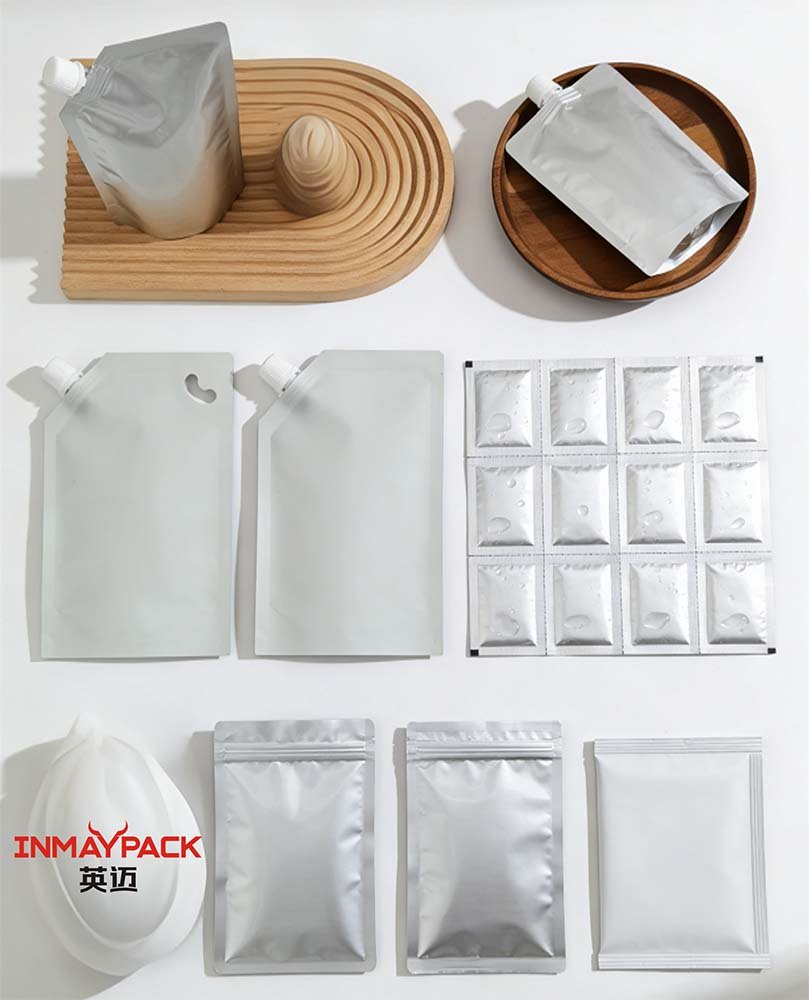
This article covers the application process. Machine specifications and available configurations belong on the dedicated product page, so procurement teams can compare equipment without mixing commercial selection and process troubleshooting.
Where zipper application fits into an HFFS line
The exact station order depends on the machine and pouch design, but the engineering logic remains consistent: the zipper must enter the web path in a controlled state and leave the application section bonded, registered and ready for the subsequent pouch-forming and sealing steps.
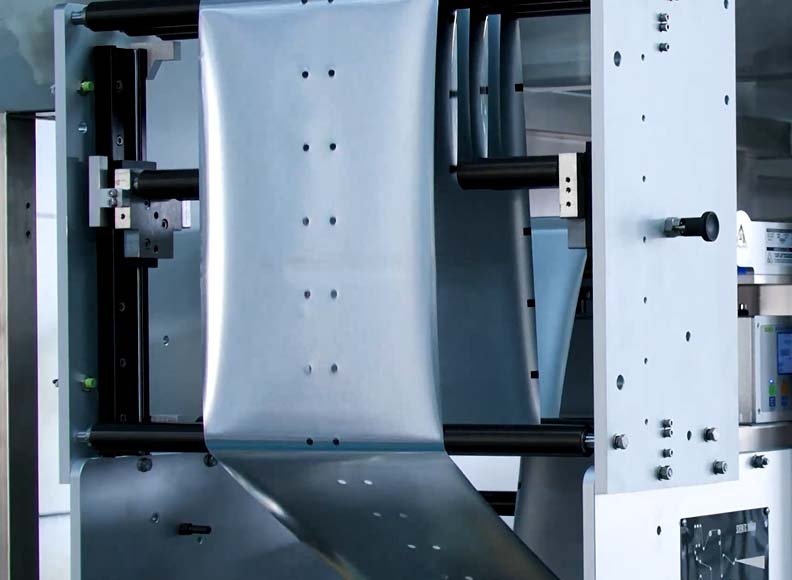
- Zipper unwind and tension control. The continuous profile is unwound without stretching, twisting or intermittent drag that would change its position relative to the film.
- Profile orientation and flange separation. The interlocking profile and seal flanges are guided in the required orientation. The flanges must present to the film without folding under or overlapping incorrectly.
- Lateral positioning. Guides establish the zipper line relative to the web edge, print repeat, future cut line, tear feature and top-seal area.
- Tack or pre-seal. A controlled attachment holds the zipper in position before the full bonding step or subsequent web movement. The approved process depends on zipper and film construction.
- Flange bonding and cooling. Heat, pressure and dwell must bond the intended flange area without collapsing the profile or shrinking the surrounding film.
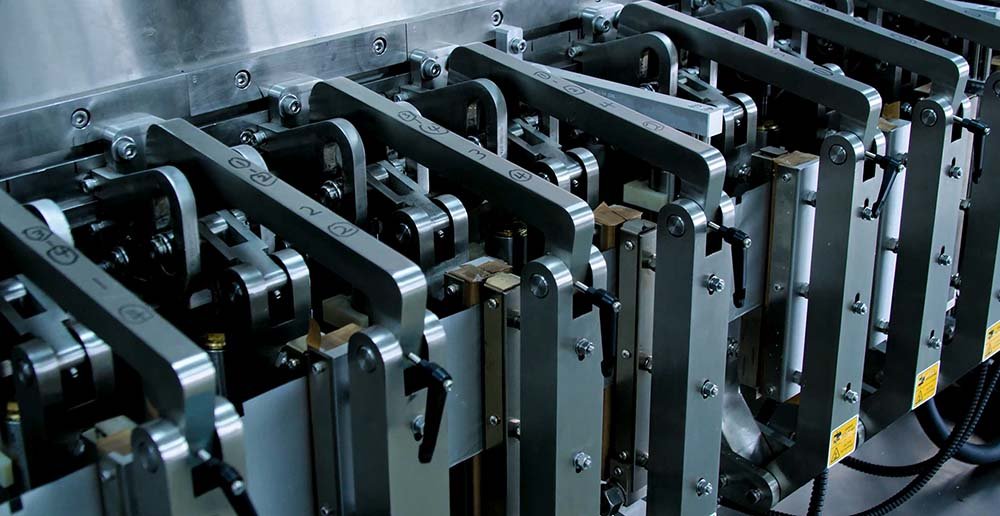
- End treatment and pouch conversion. Each bag repeat must transition through the side-seal area. End crushing, notching, cutting or other treatment is design-dependent and must match the tooling and seal map.
Important distinction: a reclosable zipper is not automatically the package’s initial hermetic closure. Many designs use a separate top seal or other tamper-evident construction above the zipper. The approved package drawing must define which feature provides initial package integrity.
Alignment is measured against the finished pouch—not only the film edge
A stable zipper line must be coordinated with the printed artwork, pouch top, tear notch, cut line, top seal and side seals. Measuring only from the raw web edge can hide registration drift or a mismatch between the zipper and bag repeat.
Profile position and seal clearance
The interlocking profile needs room to function after the package is filled and top-sealed. If it sits too close to a heated top-seal zone, the profile may distort or become difficult to open. If it is placed too low, the intended opening geometry and usable fill volume can change. The correct clearance is a drawing-controlled value, not a universal rule.
Flange bonding
Bond the zipper flanges to the film’s intended sealant surfaces. Compatibility depends on the zipper resin, flange construction, laminate sealant, any pre-applied adhesive and the defined heat history. A visually attached flange may still peel, channel or distort under filling and handling loads.
Zipper ends and side-seal crossings
At each pouch side, the zipper introduces extra material into the seal stack. The tooling and end treatment must create a continuous transition without leaving a channel or a hard lump that prevents jaw contact. Inspect both ends separately; a symmetrical drawing does not guarantee symmetrical running conditions.
Opening for filling
The package must open at the intended cavity without unintentionally separating the zipper flange bond or leaving the profile engaged where the filling operation requires access. Confirm the opening method with real zipper profiles, film stiffness and pouch dimensions.
Trace each zipper defect back to its process family
| Observed defect | Likely process family | First checks |
|---|---|---|
| Zipper drifts up or down through the run | Zipper tension, web tracking or registration control | Trend zipper-to-print and zipper-to-cut position over time; inspect unwind drag and guide stability. |
| Profile is flattened or difficult to reclose | Excess heat/pressure, jaw contact or insufficient profile relief | Inspect the profile cross-section and contact marks before changing temperature alone. |
| Flange peels from the pouch film | Material incompatibility, contamination or incomplete heat transfer | Confirm zipper/flange specification, film sealant side, surface cleanliness and cooling condition. |
| Leak or channel at one zipper end | End treatment, side-seal stack or local jaw contact | Compare left and right ends, section the transition and inspect multi-layer presentation. |
| Zipper interferes with the top seal | Drawing clearance, repeat registration or cut-position error | Measure zipper, top seal, tear feature and cut line against the approved finished-pouch drawing. |
| Pouch will not open correctly for filling | Opening sequence, profile engagement or flange placement | Observe the empty-pouch opening motion at reduced speed with the actual zipper and laminate. |
| Good empty pouch, failure after filling | Product contamination, internal load or downstream handling | Run the real product and inspect flange, profile and top-seal areas after filling, cooling and transport. |
Change only one process family at a time. Raising heat or pressure before checking alignment, contamination and layer presentation can conceal the original cause while damaging the zipper profile.
What to approve before ordering production film and zipper
Bag drawing: pouch dimensions, zipper centerline/profile location, flange zones, top seal, tear notch, cut line, side seals and bottom gusset.
Zipper specification: supplier, profile and flange construction, roll details, winding/orientation, recommended bonding conditions and any defined end treatment.
Film specification: laminate layers, sealant side, thickness, roll width, print repeat, registration mark, winding direction and approved food-contact documentation where applicable.
Application trial: zipper position across the run, flange bond, profile condition, end transitions, cooling and repeatability after thermal stabilization.
Package test: initial package integrity, top-seal performance, zipper opening and reclosing behavior, filled-package handling, drop/transport requirements and shelf evaluation defined by the package owner.
FAT acceptance: real film, real zipper, real product, required output, sustained run duration, changeover method, reject criteria and recorded sample plan.
Do not combine unlike measurements
Seal strength, zipper opening force, reclosure performance and leak integrity answer different questions. ASTM F88/F88M measures the force required to separate a seal specimen and records the failure mode; it does not by itself qualify zipper engagement, reclosure cycles or the integrity of the whole package. Define separate methods and acceptance limits for each required function.
For roll width, repeat, registration mark, winding direction and laminate information, use the doypack film specification checklist before requesting a machine trial.
Match the zipper process to the approved package
The HMK-1600 zipper doypack machine page covers equipment configuration and confirmed model specifications. This guide covers the application logic that must be validated with your actual zipper, film, pouch design and product.
Prepare a meaningful sample-run request
Send the approved pouch drawing, zipper supplier specification, laminate structure, roll layout, product data, target fill, required output and acceptance methods. INMAYPACK can then identify the tooling and tests that require confirmation.
Technical references
Google Patents, EP4194357A1: Zip strip for a flexible pouch and method and apparatus for manufacturing reclosable flexible pouches—reference for continuous zipper supply, interlocking profiles, flanges and roll-stock pouch manufacture.
Google Patents, US6920737B2: Method and apparatus for controlling zipper registration in packaging equipment—reference for registration, tacking and sealing zipper material to film.
ASTM International, ASTM F88/F88M-23—seal-strength measurement for flexible barrier materials; use the technique and acceptance limits defined by the package owner.
U.S. Food and Drug Administration, Determining the Regulatory Status of Components of a Food Contact Material—reference for verifying each packaging component against applicable authorization, specifications and conditions of use.
Need a Technical Opinion?
You Might Also Find Helpful

Auger Filler vs Weigh Filler for Powder Packaging
Compare auger and weigh fillers by powder flow, bulk density, dust, dose, refill behavior and acceptance testing before choosing aRead more
Modified Atmosphere Packaging Machine Guide for Pouches
Specify a modified atmosphere packaging machine by food risk, gas recipe, film barrier, seal integrity, residual oxygen checks and FATRead more
How to Choose a Coffee Capsule Filling Machine
Compare CF30, CF80, CF140 and CF240 coffee capsule filling machine routes by capsule, lid, dose, accepted output, tooling and FATRead more
VFFS Film Specification Guide
Define VFFS rollstock by bag geometry, web width, repeat, winding, COF, seal window, roll build and machine-trial acceptance.Read more
End-Load vs Vertical Cartoning Machine: Selection Guide
Compare end-load horizontal and vertical cartoning machines by product infeed, loading direction, carton format, line integration and FAT evidence.Read more
Liquid Form Fill Seal Machine Guide: Sachet, Doypack or Premade Pouch?
Compare liquid sachet, roll-film doypack and premade pouch routes by product flow, dosing, film, sealing, cleaning, RFQ inputs and FATRead morePowder Sachet Manufacturing Process: Equipment and Quality Guide
Follow powder sachet manufacturing from product definition and auger dosing through film forming, dust control, sealing, inspection and FAT.Read moreTurnkey Packaging Line vs Separate Machines: Buyer Decision Guide
Compare a turnkey packaging line with separate machines by responsibility, interfaces, FAT, schedule, total cost and lifecycle support.Read more







