
A side gusset pouch expands through folds along the left and right sides. That description does not define the bottom, longitudinal seam, filling opening, film structure or machine route. A side-gusset package may be formed from roll stock on VFFS equipment or supplied as a premade empty pouch.
This guide separates side gussets from bottom gussets and quad seals, then shows which drawing, film, filler, sealing, accepted-output and FAT evidence should be fixed before gusseted bagging equipment is selected.
It is a flexible package whose side panels contain inward folds that can expand as product enters. The folds increase the package depth and create side panels, but they do not automatically make the pouch self-standing. Standing behavior depends on the bottom construction, product distribution, film stiffness, fill level and handling condition.
Treat “side gusset pouch” as the beginning of a specification, not the complete specification. The pouch versus bag packaging guide explains why commercial names must be converted into a controlled drawing and supply route.
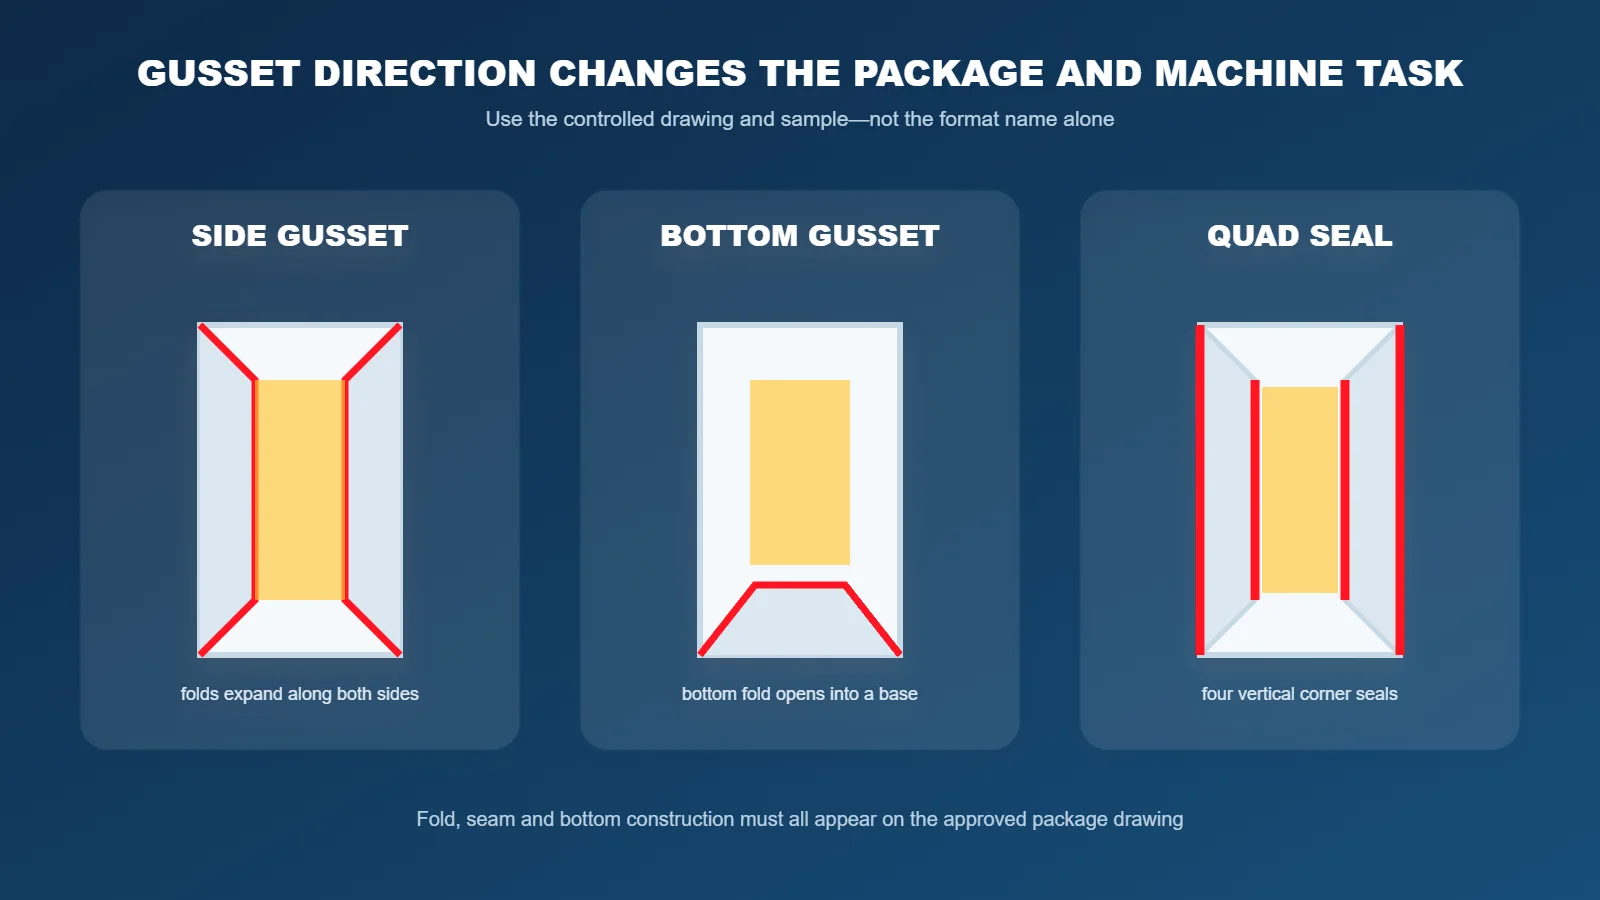
Side gusset, bottom gusset and quad seal are different package definitions
All three descriptions can appear on packs with depth, but the fold and seal locations are different. A quotation that lists only width, length and nominal capacity leaves the forming and handling task unresolved.
Folds along both sides
Confirm gusset depth, fold symmetry, longitudinal seam, bottom closure and how the sides expand under the intended product load.
Fold opens into a base
The lower fold and seal map create the potential footprint. Use the K-seal pouch guide when angled bottom seal zones are part of the design.
Four vertical corner seals
A quad-seal pack uses sealed vertical edges to define panels and shape. Review its separate tooling and film implications in the quad seal pouch guide.
| Decision | Side gusset pouch | Bottom gusset pouch | Quad-seal pouch |
|---|---|---|---|
| Primary geometry | Expandable folds on both sides | Expandable fold at the bottom | Side panels defined by four vertical seals |
| Do not infer | Self-standing result or one seam type | Universal capacity or stability | Compatibility with a standard gusset attachment |
| Drawing focus | Fold depth, back seam and bottom closure | Bottom fold, seal map and filled footprint | Corner-seal position, panel width and bottom |
| Approval basis | Controlled drawing, intended film, representative product, forming or pouch-feeding trial, sealing and agreed finished-pack tests | ||
Put the folds, seams and bottom closure on one drawing
Flat face width does not show the full web requirement or filled depth. State whether dimensions are measured with gussets folded, partially opened or under a defined filled condition. The drawing should use named datum points so the converter, machine supplier and package owner measure the same feature.
If the package includes a true bottom gusset rather than only side folds, use the bottom-gusset forming guide to define fold control and multi-layer seal transitions.
Decide whether the machine forms the gusset or receives it finished
The supply route changes the machine responsibility. A roll-stock VFFS system forms and controls the side folds during production. A premade-pouch system depends on a converter to deliver finished empty pouches, then separates, opens, supports, fills and closes them.
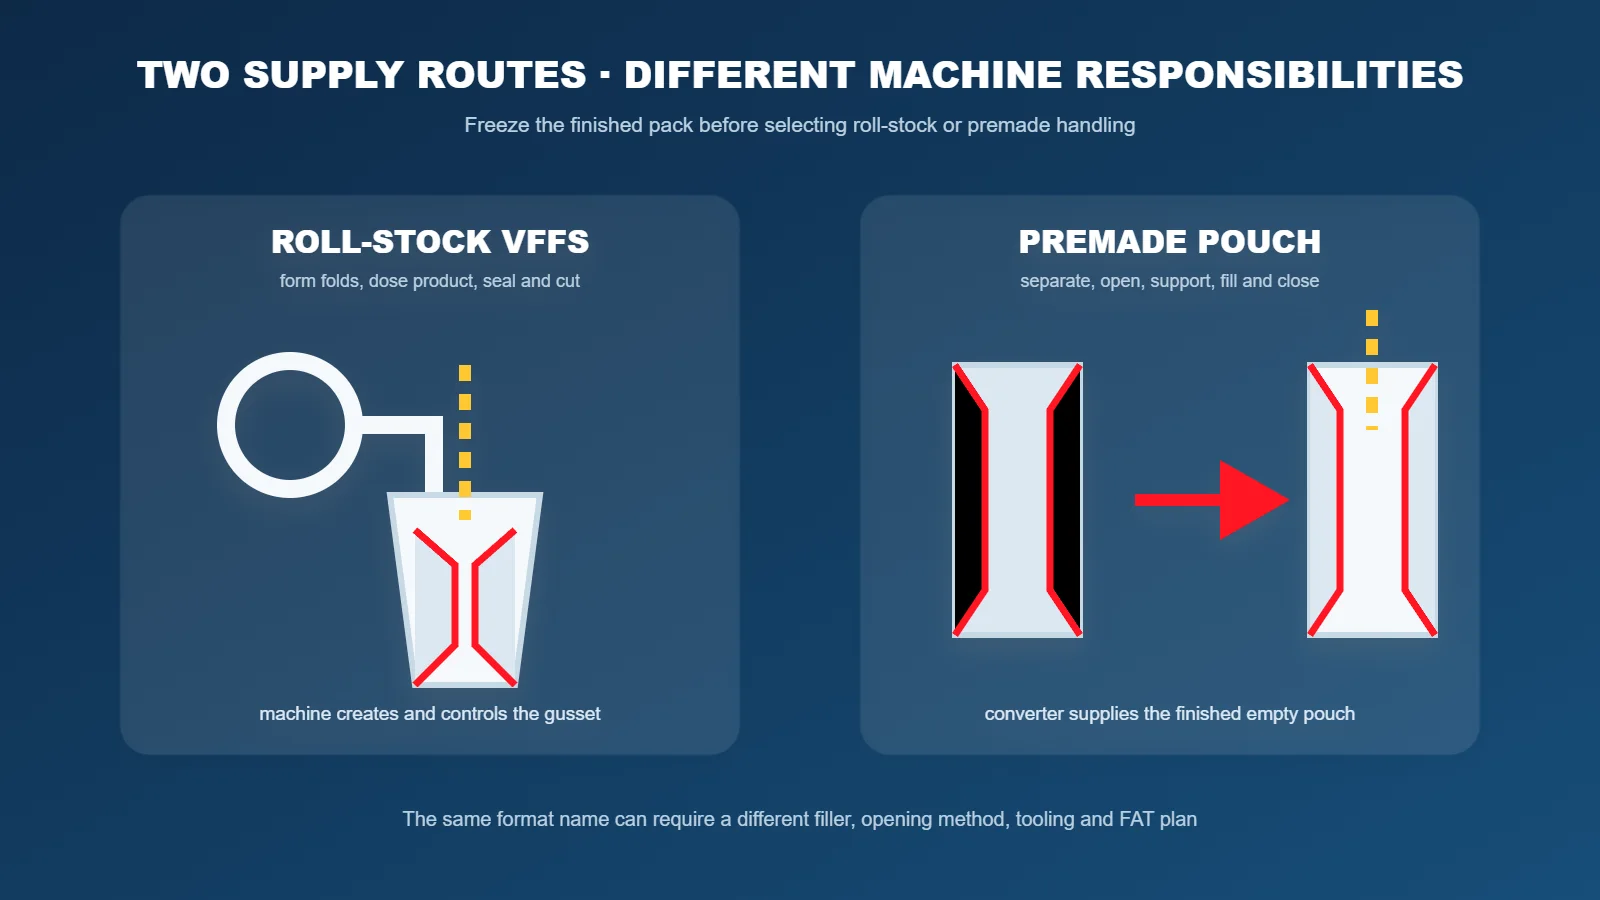
VFFS gusset-forming route
The line controls film unwind, tracking, forming set, gusset attachment or tucker action, longitudinal seam, dosing, transverse sealing, cutting and discharge. Review the full sequence in the vertical form-fill-seal machine guide.
Premade-pouch filling route
The pouch converter owns the finished construction. The packer must feed, pick, grip, open, support, fill and top-seal the approved pouch without trapping folds or damaging the panels. Compare systems on the premade-pouch machine page.
Side folds must remain controlled while the web moves and seals
On VFFS equipment, the forming set and gusset mechanism must create repeatable folds without destabilizing film tracking or the longitudinal seam. The fold must arrive consistently at the transverse jaws. Multiple film layers, sharp transitions and product in the closing area can change the usable seal window.
Guide and form
Control web tension, registration and film centering before the sides are tucked. Record the intended winding direction and sealant orientation.
Create symmetrical folds
Verify left and right gusset depth, fold position and recovery over startup, normal running, roll splice and restart.
Dose without disturbing the package
Match forming-tube clearance, filler cutoff, product fall, trapped air and settling time to the available bag volume.
Seal through layer transitions
Inspect jaw contact, contamination, temperature, pressure, dwell and cooling where gusset folds increase local layer count.
A finished gusseted pouch still has to open and present correctly
Premade pouches can remove in-line gusset forming from the filling machine, but they introduce pouch-feed and opening variables. Blocking, curl, static, film stiffness, gusset memory, zipper position and pouch-to-pouch tolerance can change pickup and mouth presentation.
Separate one pouch
Confirm magazine condition, pouch orientation, static, surface friction and doubled-pouch detection with production-representative lots.
Release every fold
Vacuum and gripper positions must open the mouth without pulling the side gussets into an uncontrolled shape or masking filling access.
Carry product load
Define bottom and side support during filling, settling and transfer so the pouch remains presented for the top seal.
Use the pouch opening and filling guide to document pickup, vacuum, grippers, mouth clearance, nozzle path and withdrawal.
The product decides how the gussets expand and carry load
Free-flowing granules may distribute into side folds readily, while aerated powder, rigid pieces, sticky product or a dense load can produce a different cross-section. Define minimum, nominal and maximum dose, bulk density or piece envelope, temperature, dust, oil, moisture, fragility and the allowed filled shape.
| Product condition | Machine question | Evidence to retain |
|---|---|---|
| Powder or fines | Can dosing and dust control keep fold transitions and seals clean? | Product condition, seal contamination, dose result and rejected sample |
| Granules | Does the product distribute across the package without one-sided loading? | Filled cross-section, weight, side expansion and discharge behavior |
| Rigid pieces | Can the largest piece pass without bridging, puncture or trapped product? | Piece range, damage, seal-area clearance and pack appearance |
| Heavy fill | What support, bottom closure and downstream handling are required? | Filled dimensions, drop or handling test and secondary-pack fit |
Validate the complete material at every fold and seam
State the full laminate, total thickness, sealant side, roll geometry or pouch lot, coefficient-of-friction basis, sealing range and storage condition. Do not approve a replacement material from nominal thickness alone. Stiffness and friction influence fold formation and pouch opening; sealant behavior influences the longitudinal seam and transverse closure.
A seal-strength measurement and a package leak test answer different questions. Record the sample location and failure mode, especially where folds create multiple layers. Use the seal integrity testing guide to separate strength, continuity, leaks and production evidence.
Fin or lap construction
Confirm which surfaces meet, overlap, seam width, position relative to artwork and whether the seam can drift into a fold or downstream contact point.
Layer transition and contamination
Inspect jaw impression, fold alignment, product clearance, temperature, pressure, dwell, cooling, cut position and the agreed test method.
Count conforming gusseted packs—not empty cycles
A gross cycle is not an accepted pack when the dose, fold, seam, code, cut or final shape is outside the agreed criteria. Define the run duration, product and film lots, normal refill or splice conditions, planned stops, inspection method and downstream state before comparing suppliers.
Lock the reference
Record drawing revision, material lot, product condition, target dose, installed tooling, recipe, utilities and machine route.
Measure fold and seam consistency
Sample left and right gusset depth, longitudinal-seam position, transverse seals, dimensions, code and cut through the run.
Challenge normal events
Include refill, film or pouch replenishment, stop/restart, blocked discharge, changeover and first-off release where required.
Separate output and rejects
Report accepted packs, rejected packs by reason, rework, empty cycles, material loss, downtime and operator intervention.
Use the Packaging Machine RFQ Builder to send every supplier the same product, package, output and FAT boundary.
Keep the failed pack before changing several settings
| Observed result | Possible process family | First evidence to preserve |
|---|---|---|
| Unequal side expansion | Fold position, product distribution, web centering or pouch opening | Left/right dimensions, filled orientation and sequence samples |
| Wrinkle at gusset transition | Film tension, tuck timing, jaw presentation, stiffness or gripper support | Wrinkle direction, machine side, settings and empty-material run |
| Leak near folded layers | Alignment, contamination, jaw contact, temperature, pressure or dwell | Failure location, seal impression, material lot and test method |
| Pouch will not open | Blocking, curl, static, gusset memory, vacuum or gripper position | Empty pouch lot, opening video and failed pickup orientation |
| Good startup, later drift | Thermal stabilization, film tracking, refill, product buildup or tooling movement | Time-stamped samples, alarms, stops, material splice and operator action |
Side gusset pouch FAQ
Does a side gusset pouch always stand upright?
No. Side folds add depth, but standing behavior depends on the bottom construction, product distribution, film stiffness, fill level and handling. Approve the filled package under a defined test condition.
Is a side gusset pouch the same as a quad-seal pouch?
No. A side gusset describes expandable side folds. A quad-seal pouch uses four vertical corner seals that define its panels. Some market descriptions overlap, so the controlled seal drawing is the final reference.
Can VFFS equipment make a side gusset bag?
Some VFFS platforms can use gusset-forming attachments or tooling, but suitability must be confirmed for the intended bag dimensions, film, filler, product and accepted output. Do not transfer a brochure option to every machine configuration.
Can a premade-pouch machine fill side-gusset pouches?
Possibly. The exact pouch must be tested for feeding, separation, pickup, true opening, gripping, support, filling and top sealing. Pouch stiffness, folds, zipper and bottom construction can change compatibility.
What should be sent for a gusseted pouch quotation?
Send the controlled flat and filled drawings, physical samples, product and dose data, complete film or pouch specification, all priority sizes, required accepted output, utilities, inspection, downstream scope and FAT method.
Sources used for the side-gusset selection framework
Manufacturer reference identifying gusseted bags as a VFFS application across product states and filler configurations.
Manufacturer reference that distinguishes pillow, gusset, block-bottom and Quatroseal bag styles.
Converter reference listing side-gusseted constructions with quad seal, back fin seal and lap seal options.
Seal-strength test reference; the package owner must define sampling, conditioning, technique and acceptance limits.
Continue from pouch geometry to the complete machine route
Send the pouch drawing, product and supply route
INMAYPACK will review whether the project fits roll-stock VFFS, premade-pouch filling or another package route and identify the forming, opening, filling, sealing and FAT inputs that still need confirmation.
Request a side-gusset pouch application review






