
Powder sachet manufacturing converts a controlled powder supply and roll film into measured, sealed and inspected single portions. The packaging machine is only one part of that process. Product condition, refill behavior, dosing tooling, dust control, film registration, seal cleanliness and the release test must work as one system.
An auger filler is often evaluated for fine, cohesive or non-free-flowing powders, but it is not a universal answer. The correct filling principle and machine configuration must be proven with the real powder, target dose, sachet drawing, film and accepted-output criteria.
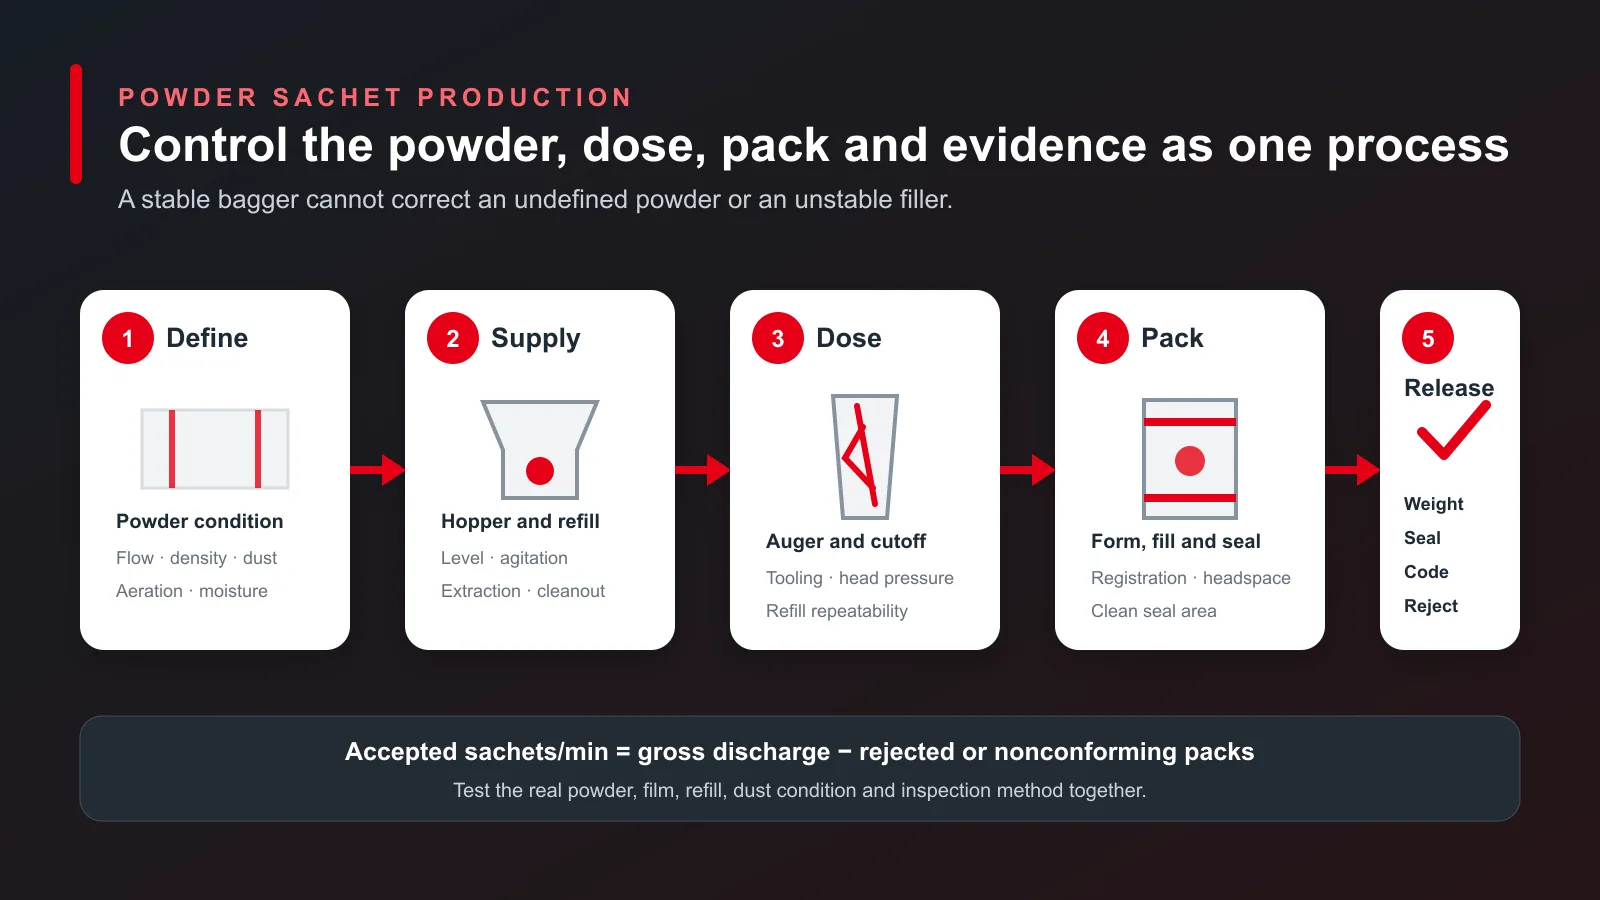
Separate powder manufacture from powder sachet packaging
The phrase “powder sachet manufacturing” is used for two different scopes. A contract manufacturer may blend ingredients, manage raw materials and produce a finished retail product. A packaging-equipment project may begin with an already approved powder and cover only feeding, dosing, sachet forming, sealing, coding, inspection and secondary handling.
Create and release the powder
This may include formulation, ingredient control, mixing, sieving, batch records and product-quality release. These operations are outside the automatic sachet packer's normal boundary unless explicitly included in a complete project.
Convert approved inputs into accepted packs
The line receives a defined powder and approved film, meters the dose, forms and seals the sachet, applies required identification and rejects packs that fail the agreed checks.
Describe how the powder behaves at the filler
A product name does not define its filling behavior. Two drink powders or spice blends can have different density, particle distribution, aeration, moisture response, oil content and static. Those differences change hopper flow, auger fill, cutoff, dust and seal contamination.
| Powder input | Why it matters | What to observe during trials |
|---|---|---|
| Bulk density range | Changes the volume required for a target mass and the relationship between auger revolutions and delivered dose. | Incoming condition, refill condition, settling and sample-to-sample weight distribution. |
| Flow and cohesion | Bridging, rat-holing or uncontrolled flow can starve or flood the dosing zone. | Hopper level response, agitation, feed consistency, cutoff and residual product movement. |
| Aeration and compaction | A powder can change density after conveying, agitation or time in the hopper. | Startup, after refill, steady production and restart after a stop. |
| Dust and fines | Airborne product can contaminate seal surfaces, sensors, machine parts and the work area. | Fill-point extraction, funnel condition, sachet mouth, cleanup and rejected seals. |
| Moisture or oil | Hygroscopic or oily powder may build up, smear, cake or change flow during the run. | Contact surfaces, auger tube, cutoff, seal area and changeover effort. |
| Particle distribution | Mixed or fragile components can segregate or break as the product is conveyed and dosed. | Finished-dose composition, breakage, retained material and batch uniformity. |
A small, freshly prepared laboratory sample may not represent the powder after transport, storage, refill and agitation. Trials should include enough material to observe the expected production states.
Choose the sachet route before fixing the filler configuration
Flat sachets, narrow stick packs and premade pouches create different openings, product-drop windows, film paths and sealing constraints. The package drawing and supplied material determine which machine family can present a controlled container below the filler.
Flat roll-film sachet
A controlled web is formed into a 3-side or 4-side sealed sachet, filled and closed. Confirm the web arrangement, dose, fill opening and powder clearance from the final seal.
Parallel sachet or stick pack
One wide web and several dosing paths can increase nominal output, but lane-to-lane dose, registration, seal condition and reject evidence must remain visible.
Premade powder pouch
The line must separate, open, grip and support the supplied pouch before dosing. Pouch-mouth condition and top-seal contamination become major acceptance points.
Use the powder sachet packing machine page for the single-lane commercial route, the multi-lane sachet machine page for parallel formats and the stick pack machine page for narrow single portions.
Stabilize refill and hopper condition before tuning the dose
The filler cannot deliver a repeatable dose if the material reaching the metering zone changes unpredictably. Bulk transfer, hopper geometry, level control, agitation and refill timing should preserve a usable product condition rather than simply keeping the hopper full.
The powder filling machine overview compares package routes, while the auger filling machine page focuses on dosing hardware and integration.
Configure auger dosing around the real powder and dose range
An auger filler meters powder by rotating a screw through a controlled tube or product path. Delivered mass depends on more than a revolution count. Screw geometry, tooling clearances, hopper assistance, product head, density, cutoff, refill and vibration can all change the result.
Match auger and tube to the task
Target dose, usable pouch opening, powder behavior and required rate affect the screw, tube and funnel arrangement. One large tool is not automatically suitable for every dose in the planned range.
Control the condition above the screw
Level and agitation influence how product fills the auger flights. Review dose behavior before and after refill rather than accepting only a short steady sample.
Stop product movement cleanly
Powder that continues to fall after the intended dose can change weight and contaminate the sachet seal. Observe tailing, dust and buildup at production timing.
Measure finished sachets
Record the target, permitted range, sampling plan, measuring device and treatment of rejected or out-of-range packs. Filler samples alone do not prove finished production.
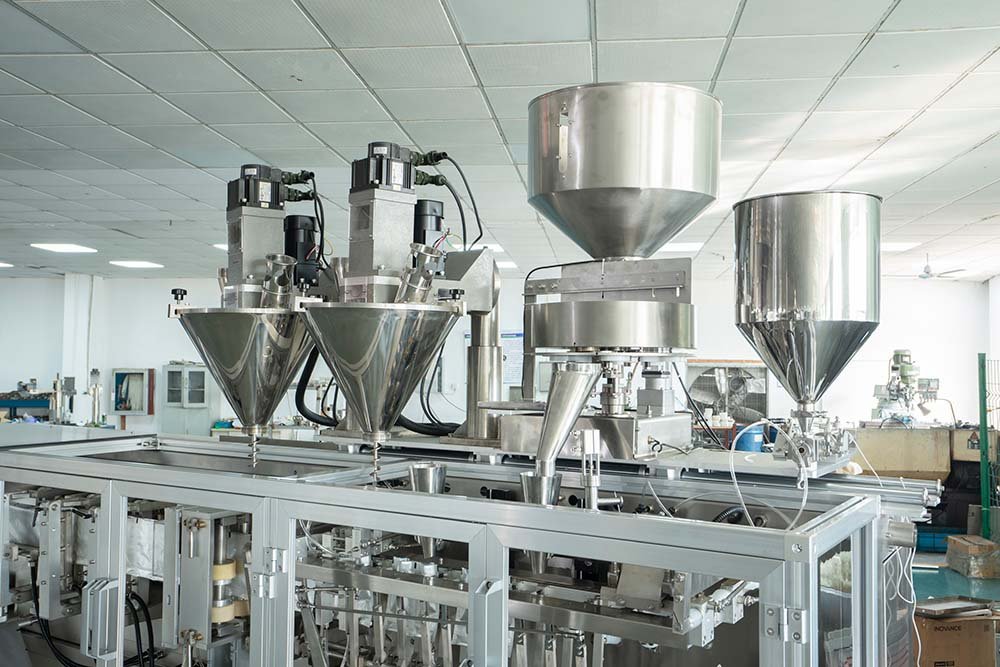
Control dust before it reaches the sachet sealing zone
Powder in the final seal can reduce continuity, create channels or prevent the surfaces from contacting as intended. The line should control the source of dust and the path to the sachet mouth rather than depending on the sealing jaws to crush through contamination.
Reduce uncontrolled product release
Stabilize hopper flow, auger cutoff, funnel position and timing so excess powder does not remain airborne or continue falling after the dose.
Maintain headspace
The selected dose and sachet geometry must leave enough space for product settling, mouth control and the required seal width.
Capture dust at the appropriate source
Extraction should be designed for the actual product and process without removing saleable powder or disturbing dose control. Facility responsibilities must be defined.
Inspect the seal zone
Use the agreed visual, leak, strength or other test to decide whether the finished seal meets the product owner's acceptance criteria.
The buyer must evaluate combustible-dust, exposure, extraction, housekeeping and destination-specific safety requirements for the actual powder. A generic packaging-machine description cannot determine those obligations.
Prove the sachet material under real powder conditions
The approved laminate must form, track, register and seal through the intended operating window. A clean empty-film seal does not prove the final sachet when powder, dust, heat history, cooling and machine timing are introduced.
Hold geometry and print position
Verify roll build, unwind, tension, edge guidance, print marks, pitch, cutting and the seal layout on the controlled sachet drawing.
Coordinate heat, pressure and dwell
Record the usable settings with the approved film and production speed. Include cooling and the load applied during discharge or downstream collection.
Challenge the contamination risk
Run the worst intended powder condition and observe dust, fines, oil or particles in the seal band rather than approving only clean laboratory samples.
Define the test and acceptance limit
Seal strength, leak, burst, dye or other methods answer different questions. The product owner should select the relevant method, sample plan and limit.
Use the stick pack film specification guide for narrow roll-film packs and the seal integrity testing guide to separate seal strength, continuity and package leakage.
Count accepted sachets and retain the reason for every loss
The useful production rate is conforming finished sachets per minute or per shift under a named product, dose, film, format and operating condition. Gross machine discharge can include underweight packs, contaminated seals, registration defects, code failures and rejects that cannot be sold.
| Quality point | Possible control | Evidence to retain |
|---|---|---|
| Dose or net content | Defined sampling, checkweighing or another approved measurement route. | Target, limits, results, measuring device, lot, time and action for out-of-range packs. |
| Seal condition | Visual review plus the agreed strength, leak or integrity method. | Film lot, settings, samples, test method, defect identity and affected production window. |
| Registration and cut | Print-mark control, dimensional checks and artwork-position criteria. | Roll identity, measured position, correction history and rejected count. |
| Code and traceability | Presence, readability and content verification appropriate to the project. | Approved code format, batch relationship, challenge result and rejected samples. |
| Reject function | Detection, physical removal and reject confirmation where specified. | Challenge pieces, cause, response, container control and reconciliation. |
| Accepted output | Gross count minus rejected or nonconforming packs. | Test duration, stops, refills, adjustments, rejects by cause and accepted total. |
Design access and verification before promising a fast recipe change
Powder can remain in hoppers, augers, tubes, funnels, guards and extraction paths. The quotation should identify the product-contact boundary, removable parts, tools, cleaning method, drying requirement, reassembly checks and release evidence.
Reach every required surface
Confirm which parts open, slide or remove and whether the operator can inspect the surfaces identified by the buyer's cleaning procedure.
Control identity and condition
Record augers, tubes, funnels, forming parts, sealing tools, cutters and recipes for each approved product and sachet combination.
Define how clean is accepted
Visual inspection, swabbing, allergen controls or another method must follow the product owner's quality and regulatory assessment.
The packaging machine maintenance guide helps separate preventive tasks, inspection records, wear parts and breakdown response.
Run the FAT through refill, dust, rejection and restart
A short clean run can hide the conditions that limit powder-sachet production. The FAT should use approved or representative powder and film, include the intended packaging modules and report conforming finished sachets.
Use the packaging machine RFQ builder to organize supplier inputs before the trial protocol is issued.
Compare an in-house sachet line with contract packing on the same demand basis
Searches for powder sachet manufacturing often mix two decisions: buying a production line and buying a contract-packing service. The appropriate route depends on demand, product ownership, internal quality capability, capital plan, change frequency and the level of control required.
Own equipment and production control
The buyer manages facility readiness, operators, quality systems, maintenance, materials, validation and capacity. The investment can be justified when control, volume, confidentiality or long-term production needs support it.
Purchase a defined manufacturing service
The brand owner should still approve product, materials, records, release criteria, change control and supplier responsibilities. A service quotation is not comparable with a machine quotation.
If an owned line is the preferred route, compare a single machine module with a coordinated project using the turnkey line versus separate machines guide.
Powder sachet manufacturing FAQ
How are powder sachets manufactured?
An approved powder is supplied to a controlled filler, commonly an application-matched auger for suitable products. Roll film is guided and formed into the required sachet, the dose is delivered, the remaining seals are completed and the finished pack is coded, inspected and released according to the quality plan.
Does every powder sachet machine use an auger filler?
No. Auger dosing is a common candidate for fine, cohesive or non-free-flowing powders, but weigh-based, volumetric or other systems may be considered for different materials and requirements. Selection requires representative trials.
What causes powder sachet weight variation?
Causes can include density change, aeration, unstable refill, bridging, hopper level, agitation, tooling, cutoff, machine vibration, product buildup and the measuring method. Record conditions before and after refill rather than changing one speed setting in isolation.
How is powder kept out of the sachet seal?
Control hopper flow, auger cutoff, funnel position, fill timing, headspace, dust extraction and settling before the sachet reaches the final seal. The approved seal test must still verify finished packages.
What should be sent to a powder sachet machine supplier?
Send representative powder and its condition range, target dose and limits, finished sachet drawings, film and roll data, required accepted output, inspection and coding scope, cleaning needs, utilities, destination and required FAT evidence.
How should powder sachet machine speed be compared?
Compare accepted sachets per minute for the same powder, dose, sachet, film, refill method, test duration, reject rule and downstream condition. Empty cycles or gross discharge alone do not establish production output.
Sources used for the process and quality framework
Primary safety reference explaining combustible-dust hazards and control resources. The buyer must assess the actual powder and facility.
Official U.S. food current-good-manufacturing-practice and preventive-controls regulation; applicability depends on product, market and facility.
Official U.S. reference for checking net contents of packaged goods. Applicable sampling and legal requirements must be confirmed for the destination.
Primary industry guidance for structuring pre-shipment equipment acceptance against user requirements.
Seal-strength test reference; the product owner must define conditioning, technique, sampling and acceptance limits.
Use the page that matches the next decision
Test the powder, dose and sachet before fixing the machine scope
Send representative powder, condition limits, target dose and tolerance, sachet drawing, film data, required accepted output, cleaning needs, destination and FAT criteria. INMAYPACK will review the supply, dosing, forming, sealing and inspection boundary before confirming an applicable configuration.







