
A stick pack machine price is useful only when every supplier is quoting the same product, stick drawing, lane layout, dosing system, accepted output and delivery boundary. A compact one-to-four-lane machine and a six-to-ten-lane production system may answer the same search phrase while carrying very different equipment and validation scope.
This guide gives procurement, engineering and production teams a controlled way to compare stick pack quotations without presenting an unverified universal price range.
Start with the stick pack platform, not the headline price
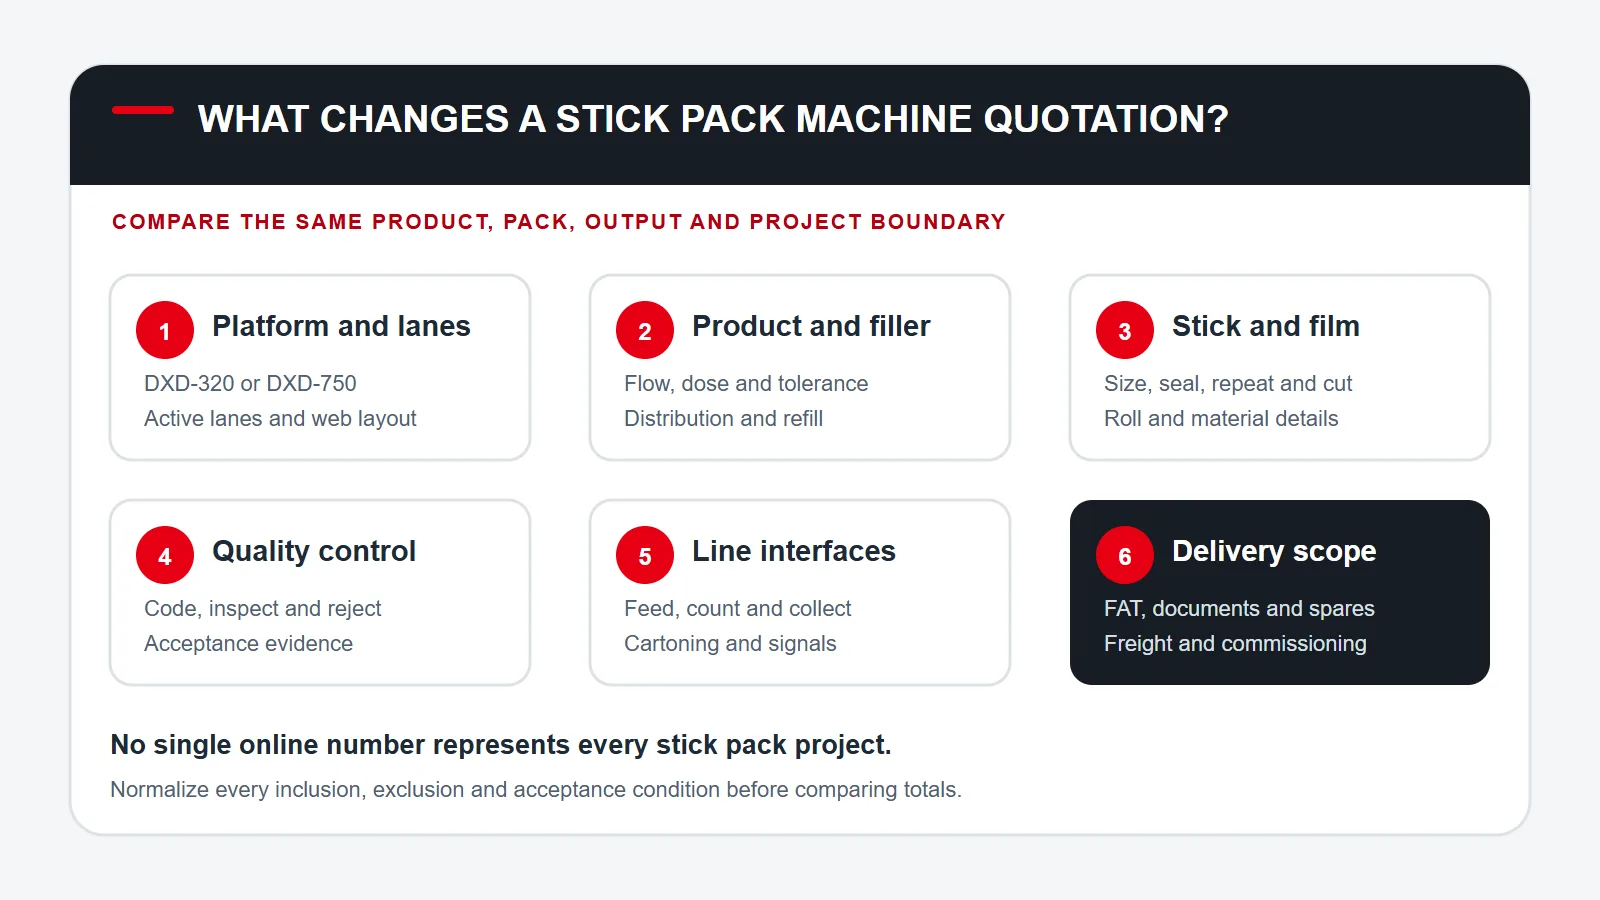
A stick pack machine forms narrow packages from heat-sealable roll film, meters product into one or more forming tubes, makes the longitudinal back seal, closes the ends and cuts the finished sticks. The price changes when any part of that path changes: machine width, number of lanes, filler, product distribution, forming sets, controls, inspection or downstream collection.
INMAYPACK’s available DXD series documentation separates the DXD-320 and DXD-750 stick-pack routes. The figures below are source-document selection boundaries, not production guarantees. The real product, film and acceptance test still determine the approved configuration.
| Selection point | DXD-320 reference | DXD-750 reference | Quotation effect |
|---|---|---|---|
| Documented lane range | 1–4 lanes | 6–10 lanes | More lanes affect web width, product distribution, forming sets, sealing positions, controls and discharge. |
| Maximum film-width reference | 320 mm | 750 mm | Usable web width must include lane pitch, seal widths, trim and registration requirements. |
| Documented fill-volume reference | 1–40 ml | 2–40 ml | Volume does not select the filler by itself; product behavior and mass tolerance still require review. |
| Documented aggregate-output reference | 20–160 sticks/min | 280–480 sticks/min | Compare accepted sticks under the agreed product, film, refill, reject and run conditions. |
| Best comparison use | Lower lane-count projects, format development and moderate output. | Higher aggregate output with a wider multi-lane process. | The correct platform is the result of the application review, not a price tier chosen in isolation. |
Review the DXD-320 and DXD-750 stick pack machine page for the documented model boundary. Use the stick pack versus sachet guide first if the finished package format is not yet approved.
Eight decisions change the stick pack machine quotation
A requirement changes cost when it adds hardware, tooling, controls, engineering, testing or delivery responsibility. These decisions should appear as named line items or controlled inclusions rather than disappearing inside a model label.
Machine width and parallel paths
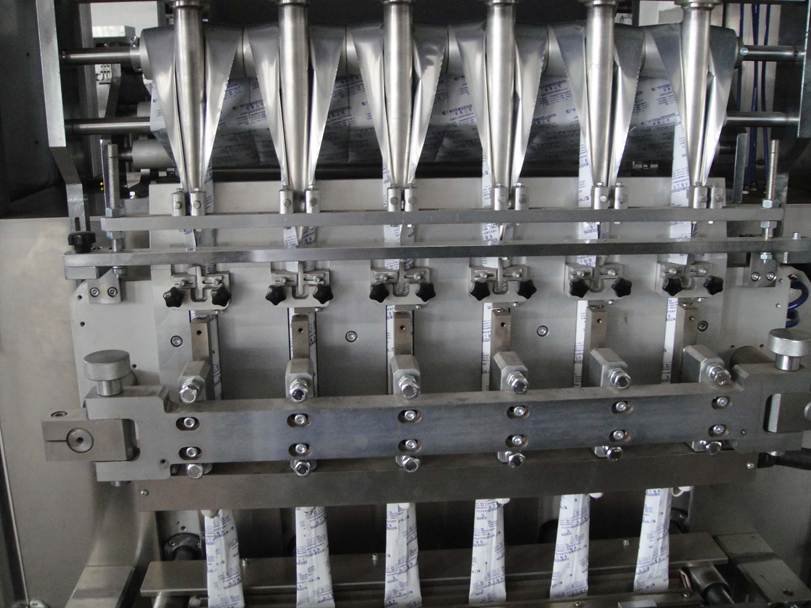
Lane count changes the web path, number of forming sets, dosing paths, seal positions, cutters, controls and collection challenge. Ask for the approved active-lane layout, not only the maximum possible lane count.
Filler and distribution
Free-flowing granules, fine powder, cohesive powder, liquid or paste require different feeding, metering, cutoff and cleaning arrangements. Multi-lane distribution must supply each lane consistently during refill and steady production.
Geometry, structure and print
Stick width and length, seal width, film structure, thickness, roll diameter, artwork repeat, registration mark, tear feature and cut style affect tooling and web control.
Readable code and controlled discharge
Date or lot coding, code verification, tear notches, straight or shaped cuts, string packs and required separation can add mechanical stations, controls and acceptance checks.
Detect, reject and confirm
Weight checks, code inspection, registration checks, metal detection, seal inspection and reject confirmation must be assigned to a specific point in the line and tested as one system.
Feed, collect and pack downstream
Product elevators, vacuum loaders, tanks, discharge conveyors, counting, bundling or cartoning change both equipment scope and signal integration.
Parts, access and cleaning
Multiple stick widths, products or dosing ranges may require additional forming sets, dosing parts, recipes and release checks. Allergen, dust, washdown and access requirements can change construction and documentation.
FAT, documents and spares
Sample trials, run duration, test evidence, drawings, manuals, recipe backups, training, commissioning and initial spares are commercial scope—not free assumptions attached to the base machine.
Lane count multiplies more than the number of forming tubes
Each active lane must receive product, form film, make seals, cut, discharge and produce an accepted pack. The aggregate result can be limited by the slowest shared function: refill, product distribution, film tracking, heat recovery, cutting, counting or downstream collection.
One limit can affect every lane
Film unwind, web tracking, hopper refill, utilities, main control, extraction and downstream handling are shared. A disturbance here can reduce the entire line’s accepted output.
Variation must remain identifiable
Dose, seal, registration, cut and reject data should retain lane identity during FAT. A good average can hide one underperforming lane.
Build the budget beyond the base stick pack machine
A useful budget follows the equipment from confirmed application through accepted operation at the buyer’s site. Country duties, taxes and site work vary by destination and should not be presented as one universal online number.
Primary machine + dosing and product supply + coding and inspection + format parts + FAT + export and delivery + installation or commissioning + initial spares + buyer-side utilities and site work.
| Budget layer | Confirm in writing | Common comparison gap |
|---|---|---|
| Primary machine | DXD platform, active lanes, film path, forming sets, sealing, cutting, guarding, controls and standard documentation. | One quote lists only the frame and process module while another includes project tooling. |
| Dosing and supply | Filler type, number of dosing paths, hopper, agitation, refill, product distribution, contact parts and cleaning boundary. | The filler or upstream feed remains an undefined option. |
| Quality and downstream | Coding, inspection, reject, counting, collection, bundling, cartoning and every interface signal. | Headline output ends at the cutter while labor and control risk move downstream. |
| Format and change parts | Every planned stick width, forming set, cut style, tear feature, film repeat and priority SKU. | Only one production format is included although the RFQ lists several. |
| FAT and samples | Product, film, run duration, refill method, sample plan, defects, accepted output, evidence and retest rules. | “Factory tested” is stated without a controlled acceptance method. |
| Delivery and site | Export packing, exact Incoterms® rule and named place, freight ownership, utilities, unloading, rigging, installation and training. | Suppliers use different risk-transfer and site-responsibility boundaries. |
| Lifecycle readiness | Commissioning spares, wear parts, critical spares, manuals, backups, maintenance tasks and replenishment route. | The initial price excludes items required to recover from predictable failure. |
The selected ICC Incoterms® rule and named place affect cost, task and risk allocation. Record the complete rule in every quotation rather than comparing informal labels such as “FOB price” without the named place and included work.
Compare accepted sticks per minute, not theoretical lane output
A simple multiplication of machine cycles and lanes does not prove production. Product distribution, refill, dose variation, film tracking, sealing, cutting, inspection and collection must sustain the same run. Define the accepted result before the quotation is approved.
Use the multi-lane stick pack process guide to map web, dosing and sealing functions. Use the stick pack film specification guide to prepare the material and trial inputs before comparing output claims.
Put every supplier quotation into one comparison structure
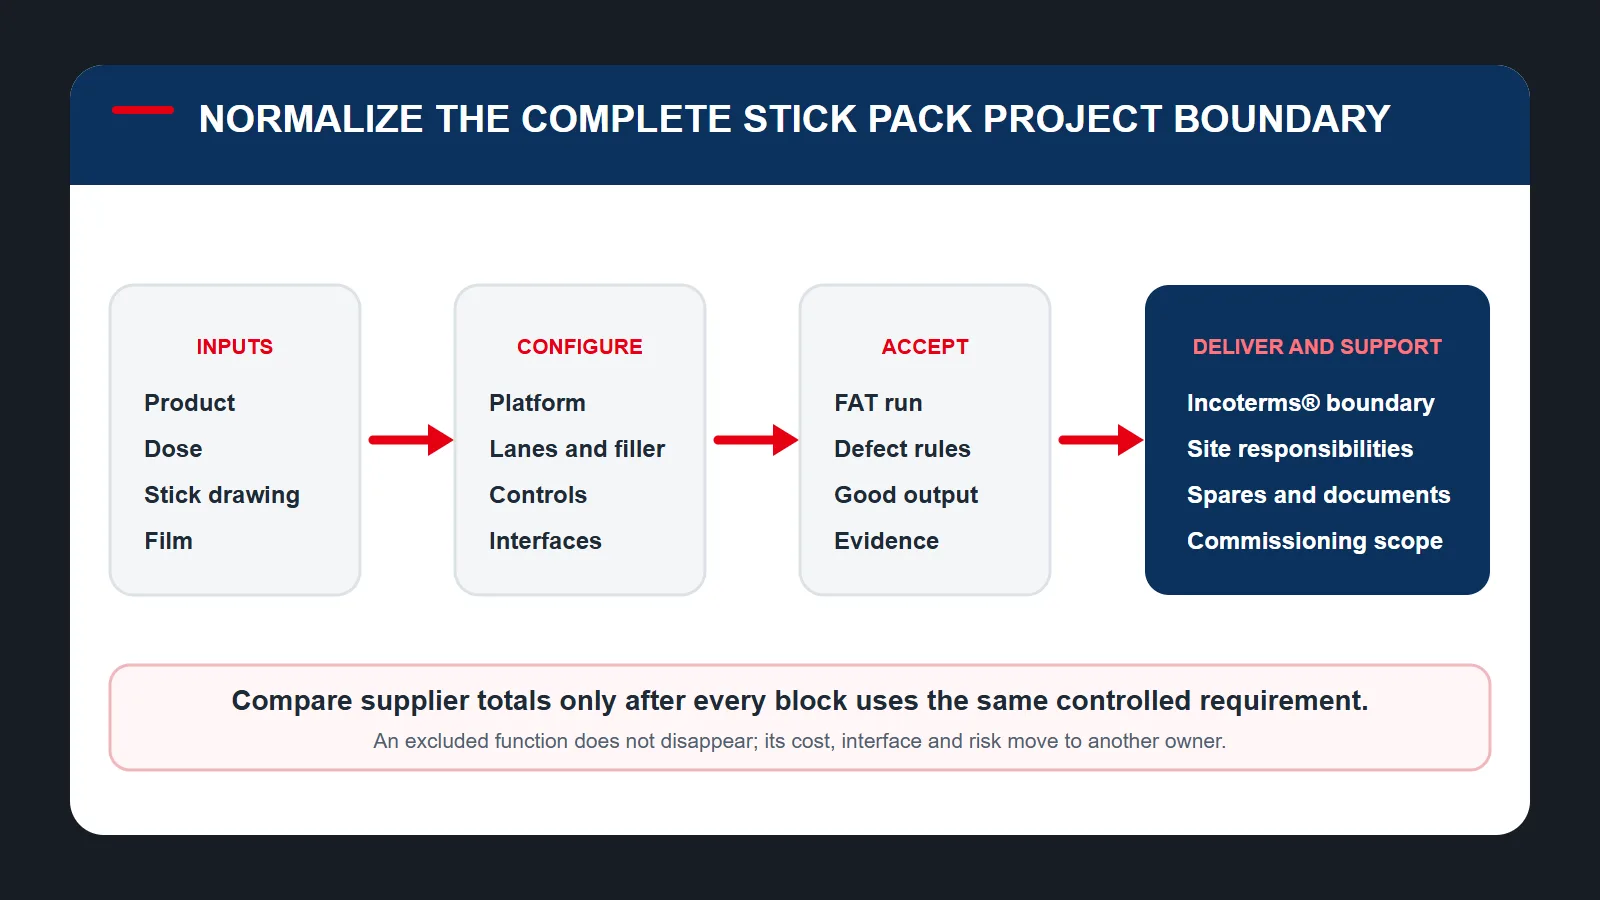
Do not compare totals until the revision, product, package and line boundary match. A disciplined comparison preserves exclusions instead of filling them with assumptions.
Lock one controlled requirement revision
Issue the same product, dose, stick drawing, film, output, utilities, destination, FAT and delivery requirement to every supplier. Record clarifications against that revision.
Separate included, optional, excluded and buyer-supplied items
Require an explicit status for the machine, filler, feed, coding, inspection, reject, conveyors, counting, cartoning, FAT materials, commissioning and spares.
Normalize performance evidence
Compare accepted sticks using the same product, film, active lanes, test duration, reject rules and refill condition. Keep mechanical cycles and theoretical maximums separate.
Normalize delivery and lifecycle scope
Use the same Incoterms® rule and named place. Add buyer-side site costs, required initial spares and known excluded work before comparing the project total.
Resolve deviations before price negotiation
List technical and commercial deviations with an owner and due date. Do not use a discount to hide an unresolved package, output, safety, interface or acceptance gap.
Send these inputs to receive a useful stick pack proposal
A supplier can configure the project faster when the inquiry includes controlled application data rather than only “best price” and a target speed.
State and behavior
Name the product, ingredients where relevant, bulk density or viscosity, particle size, dust, aeration, foam, temperature, cleaning and allergen concerns. Provide representative samples when available.
Nominal and limits
Provide minimum, nominal and maximum dose, the required tolerance, measurement method and priority SKUs. State mass or volume clearly.
Drawing and material
Send finished width and length, seal layout, film structure and thickness, roll details, artwork repeat, registration mark, tear feature and cut style.
Accepted production target
State accepted sticks per minute or hour, shifts, refill pattern, downstream condition and the permitted reject or defect basis.
Utilities and layout
Confirm voltage, frequency, phase, compressed air, extraction, nitrogen or cooling requirements, available height, access and line direction.
FAT and handover
Define run duration, sample plan, defect criteria, inspection, witnessed FAT, documents, training, spare parts, delivery location and required support.
The packaging machine RFQ builder can organize these inputs before supplier contact. For a broader cost comparison across sachet architectures, use the sachet packing machine price guide.
Stick pack machine price FAQ
How much does a stick pack machine cost?
There is no reliable universal price without a defined application. Platform, lane count, filler, product distribution, film and stick format, coding, inspection, downstream handling, FAT, delivery, commissioning and spares all change the quotation. Request a project-specific price against one controlled requirement.
Does a higher lane count always give a better return?
No. More lanes can increase aggregate output, but they also increase dosing, web, sealing, cutting and discharge complexity. The business case should use accepted output, product and film loss, changeover, cleaning, labor, downstream capacity and the actual production plan.
Why do two stick pack quotations have very different totals?
They may cover different machine platforms, fillers, lane layouts, materials, controls, inspections, format parts, testing, delivery points or services. Normalize every included and excluded item before treating the difference as a supplier price difference.
Should the filler be included in the machine quotation?
The quotation should state it explicitly. The product and dose determine the filler, number of dosing paths, supply system, contact parts, controls and cleaning boundary. A base stick pack machine without a defined filler is not a complete production comparison.
What evidence should be requested before shipment?
Request the confirmed configuration, product and film used, settings, run duration, refill condition, lane-level dose evidence, package and seal checks, code and cut results, rejects, stops, accepted output, deviations and the agreed handover documents.
Sources used for the quotation framework
Official ISO reference for risk assessment and risk-reduction principles across machinery life-cycle phases.
Official IEC reference for the electrical, electronic and programmable electronic equipment of machines.
Test-method reference for measuring seal strength; the buyer must still define the applicable sample plan and acceptance limits.
Official source for the trade terms used to clarify delivery tasks, costs and risks in a sales contract.
Continue with the task that matches the project stage
Send the product, stick drawing and accepted-output target
INMAYPACK will review the applicable DXD platform, lane layout, dosing system, film path, interfaces and FAT basis before preparing a configuration-specific quotation. Include representative product and film information so the commercial scope can be compared against one defined operating condition.







