1
Dry dairy powders
Milk powder and dairy blends require a controlled powder supply, a project-matched dosing system, dust management, seal-area protection and a package route proven with the actual powder.
Review milk powder systems →Packaging systems configured around your application Defined project scope

Dairy flexible-packaging systems
Compare milk-powder sachets and pouches, liquid dairy sachets, roll-film spout pouches and premade yogurt pouches by product condition, package route, hygiene boundary and accepted-output test.
Selection boundary
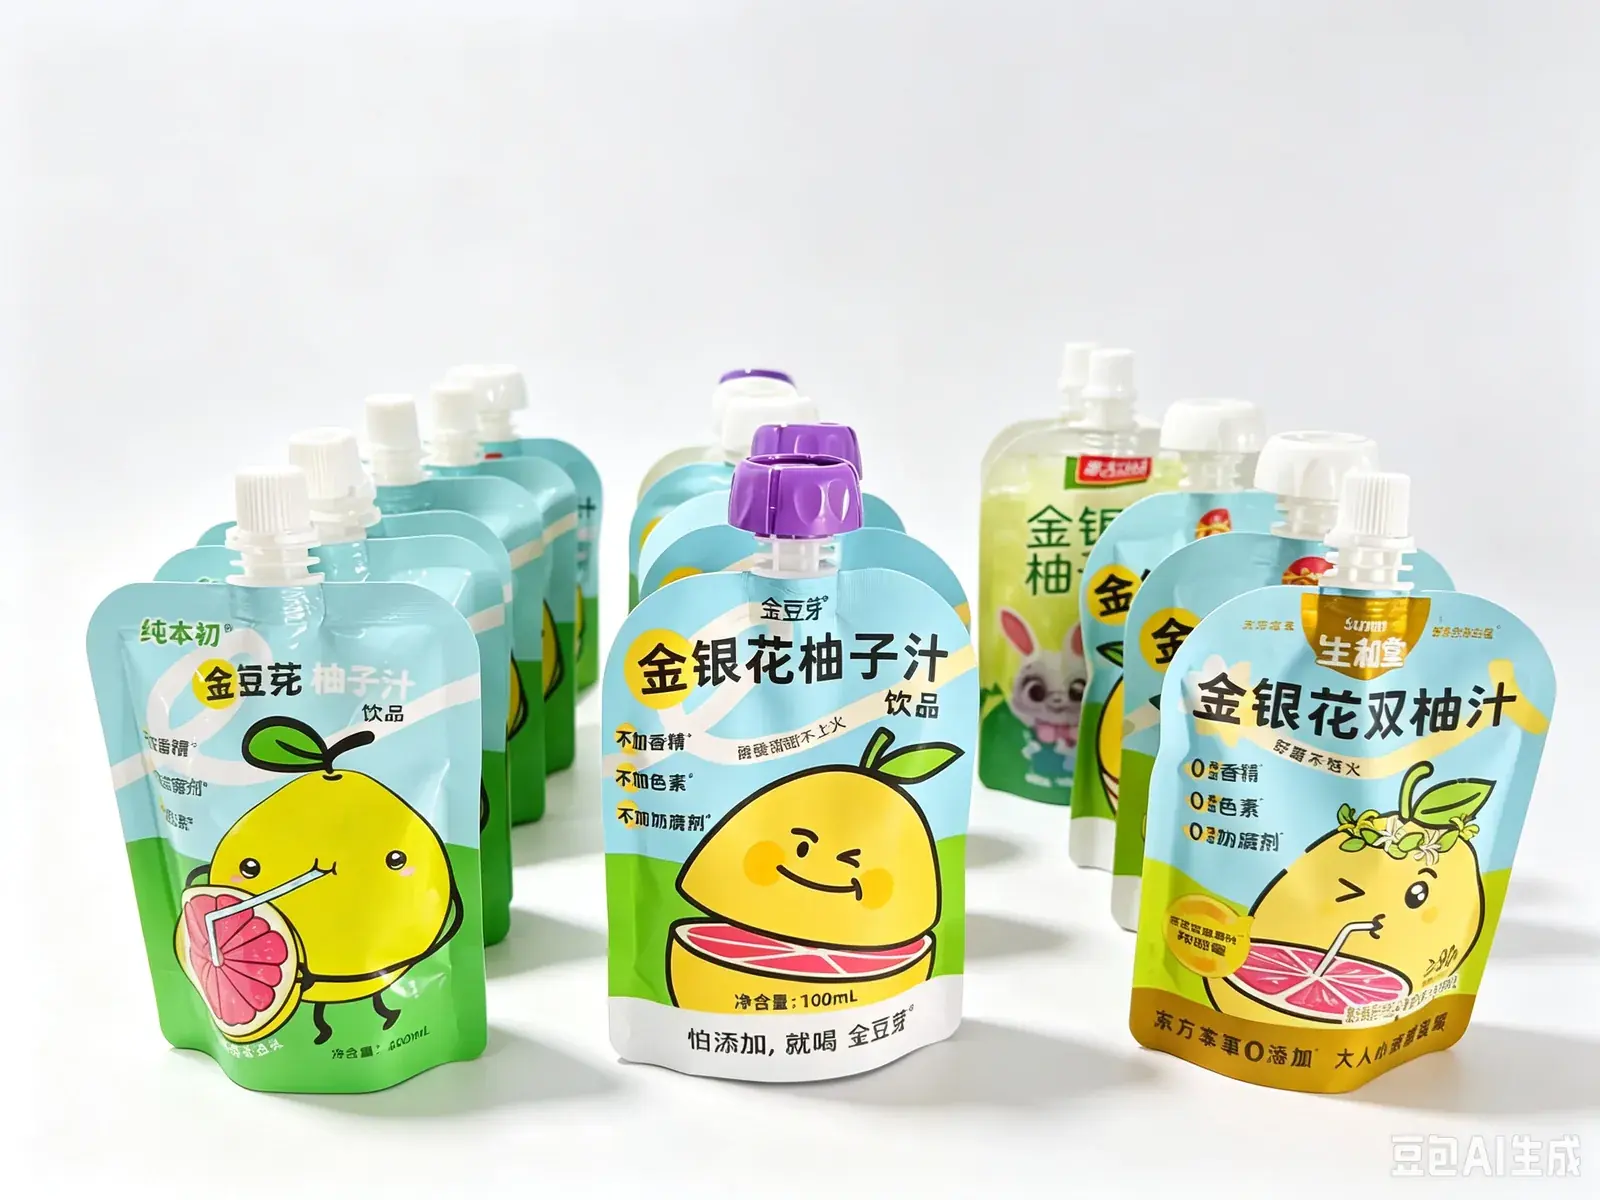
Milk powder, drinkable yogurt and viscous cultured products do not share one filler, package path or cleaning method. The first decision is the product and finished package; the machine platform follows.
Milk powder and dairy blends require a controlled powder supply, a project-matched dosing system, dust management, seal-area protection and a package route proven with the actual powder.
Review milk powder systems →Small liquid or semi-liquid portions can use a roll-film sachet route after viscosity, temperature, dose, cutoff, film and seal acceptance have been defined together.
Review liquid sachet machines →Center- or corner-spout packs may use a premade fill-and-cap route or a roll-film HFFS route. Pouch supply method, spout geometry and cap handling change the complete line.
Review premade spout-pouch filling →This page covers INMAYPACK flexible-package routes. Bottles, cups, thermoformed packs, aseptic cartons and complete dairy-processing systems are separate equipment families and are not presented here as supplied INMAYPACK products.
Package-route comparison
The route changes material responsibility, dosing access, spout or seal operations, changeover work and the FAT evidence needed to approve the project.
Roll film forms a small flat pack around a measured powder dose. Confirm powder flow, auger or other dosing principle, web layout, dust control and seal cleanliness.
Use roll-film doypacks or supplied premade pouches for larger milk-powder formats after fill range, settling, headspace, zipper and accepted-output requirements are defined.
Form, dose and seal smaller liquid dairy portions. Confirm viscosity and temperature range, anti-drip or cutoff behavior, fill tolerance, seal contamination and cleaning access.
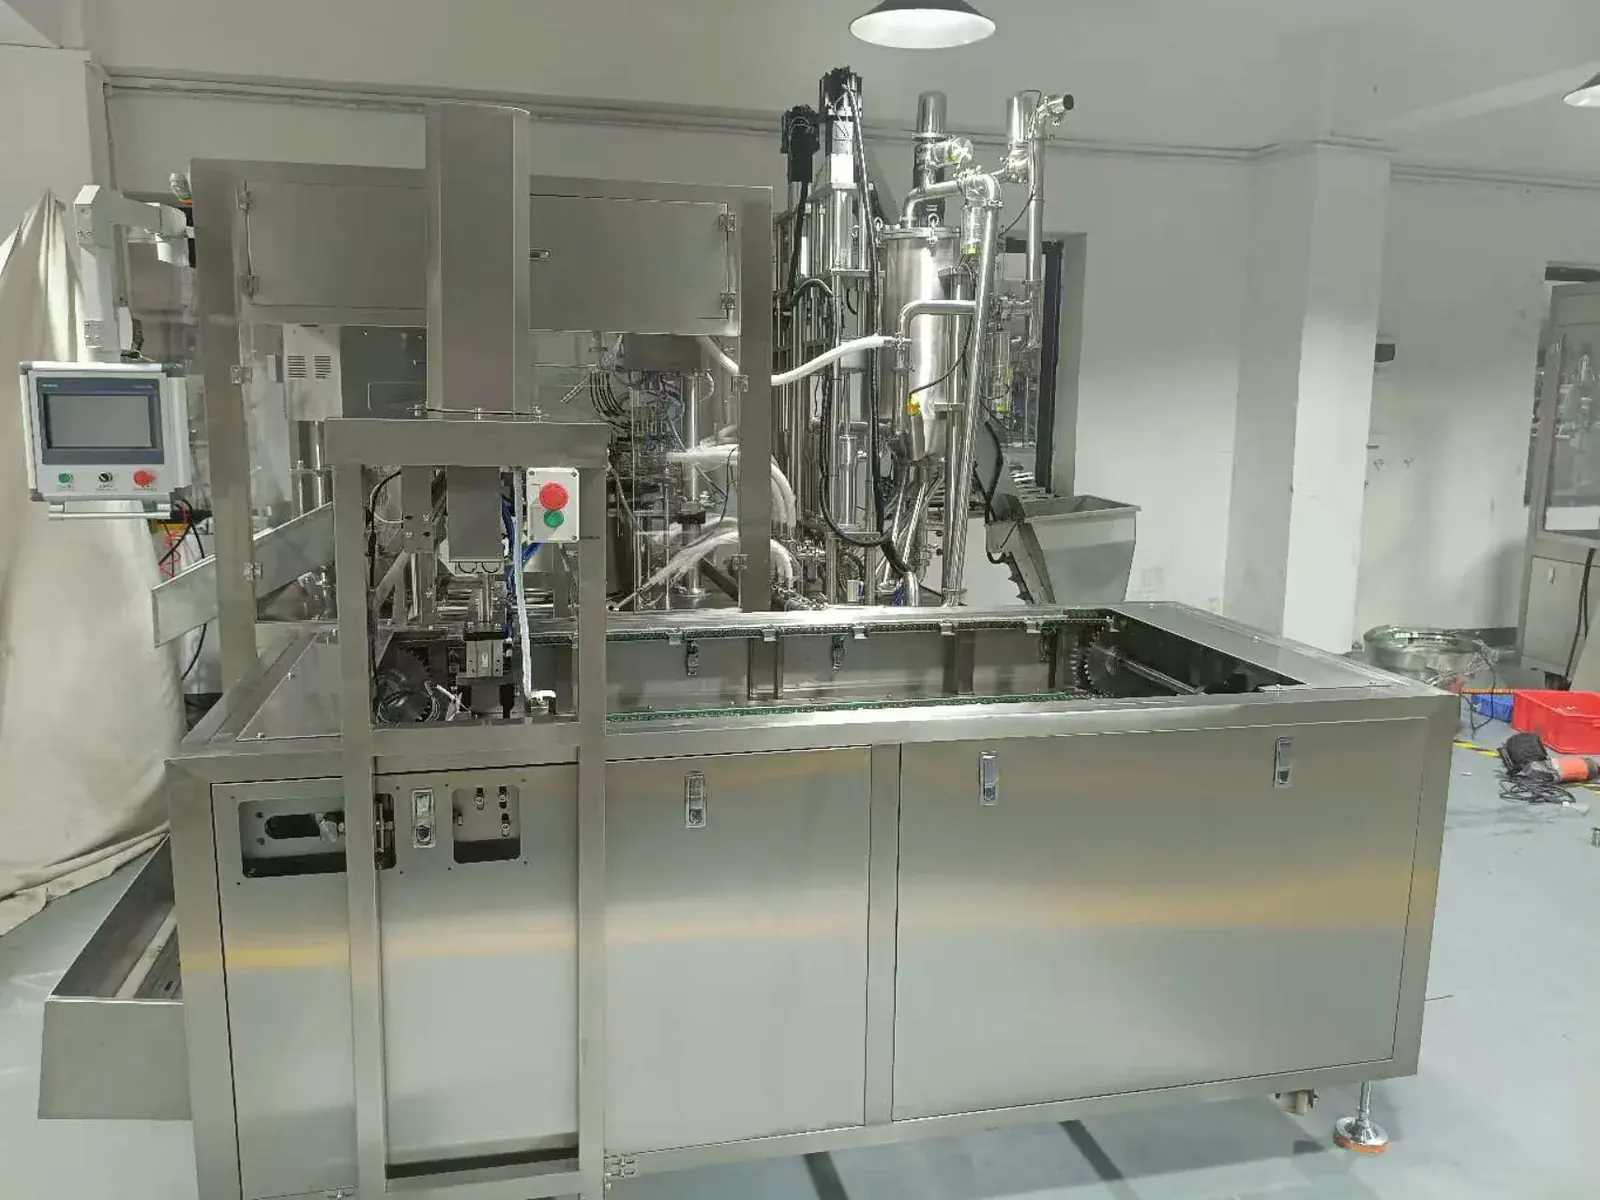
Supply finished pouches with fitted spouts for controlled feeding, filling and capping. Validate the real pouch, cap, spout, carrier, product and replenishment method.
Form the pouch from roll stock and integrate filling, spout handling and capping inside the confirmed HFFS configuration. Film and fitment drawings become machine inputs.
Product condition
“Yogurt” or “milk powder” is not enough information for a machine proposal. Record the usable operating range and the conditions that can change during production.
Provide bulk-density range, flow, aeration, dust, fat or oil tendency, moisture sensitivity, particle distribution, dose range, refill method and the required tolerance basis.
Provide viscosity at the intended fill temperature, particulates, foam, stringing, shear sensitivity, settling or separation, required agitation and maximum permitted hold condition.
List every planned SKU, color or flavor, allergen boundary, batch sequence, cleaning method, changeover frequency and the hardest product that should define the trial.
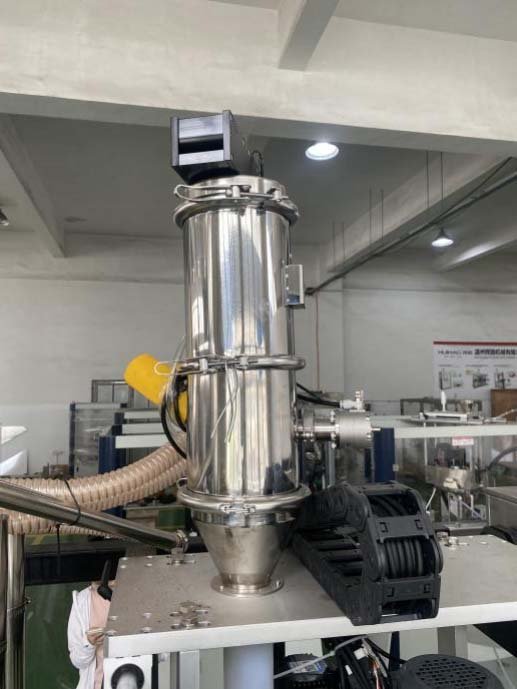
A filler can be accurate under a controlled bench condition and unstable when product level, refill timing, aeration, temperature or viscosity changes. Define how product is delivered to the packaging machine and who controls each upstream boundary.
System comparison
Do not compare an isolated bagger with a quotation that includes feeding, dosing, cap supply, inspection and downstream transfer.
| Decision area | What the buyer provides | What the supplier confirms | Evidence to retain |
|---|---|---|---|
| Product | Operating condition, dose range, worst-case SKU and samples | Product path, metering principle, contact design and controls | Sample identity, setup record and observed filling result |
| Package | Controlled drawing, film or premade pouch, spout, cap and artwork | Handling or forming route, tooling, opening/fill access and sealing | Approved drawing, material lot and retained finished packs |
| Hygiene | Cleaning method, recipe sequence, allergen boundary and plant rules | Contact-part access, removal steps, drain or residue risks and exclusions | Cleaning demonstration, parts list and agreed procedure |
| Output | Required accepted packs by priority SKU and test duration | Complete configuration, operating basis, constraints and reject definition | Accepted count, rejects by cause, stops and interventions |
| Handover | Destination, utilities, training and document requirements | Included scope, exclusions, FAT, delivery, commissioning and support | Approved proposal, FAT record, manuals and open-item closure |
Hygiene and seal control
Dairy applications can expose different risks depending on the product and process. The machine supplier should not infer the buyer's hygiene program or food-safety controls. The project documents should identify the supplied contact path, materials where confirmed, cleaning access, hold conditions and the package acceptance method.
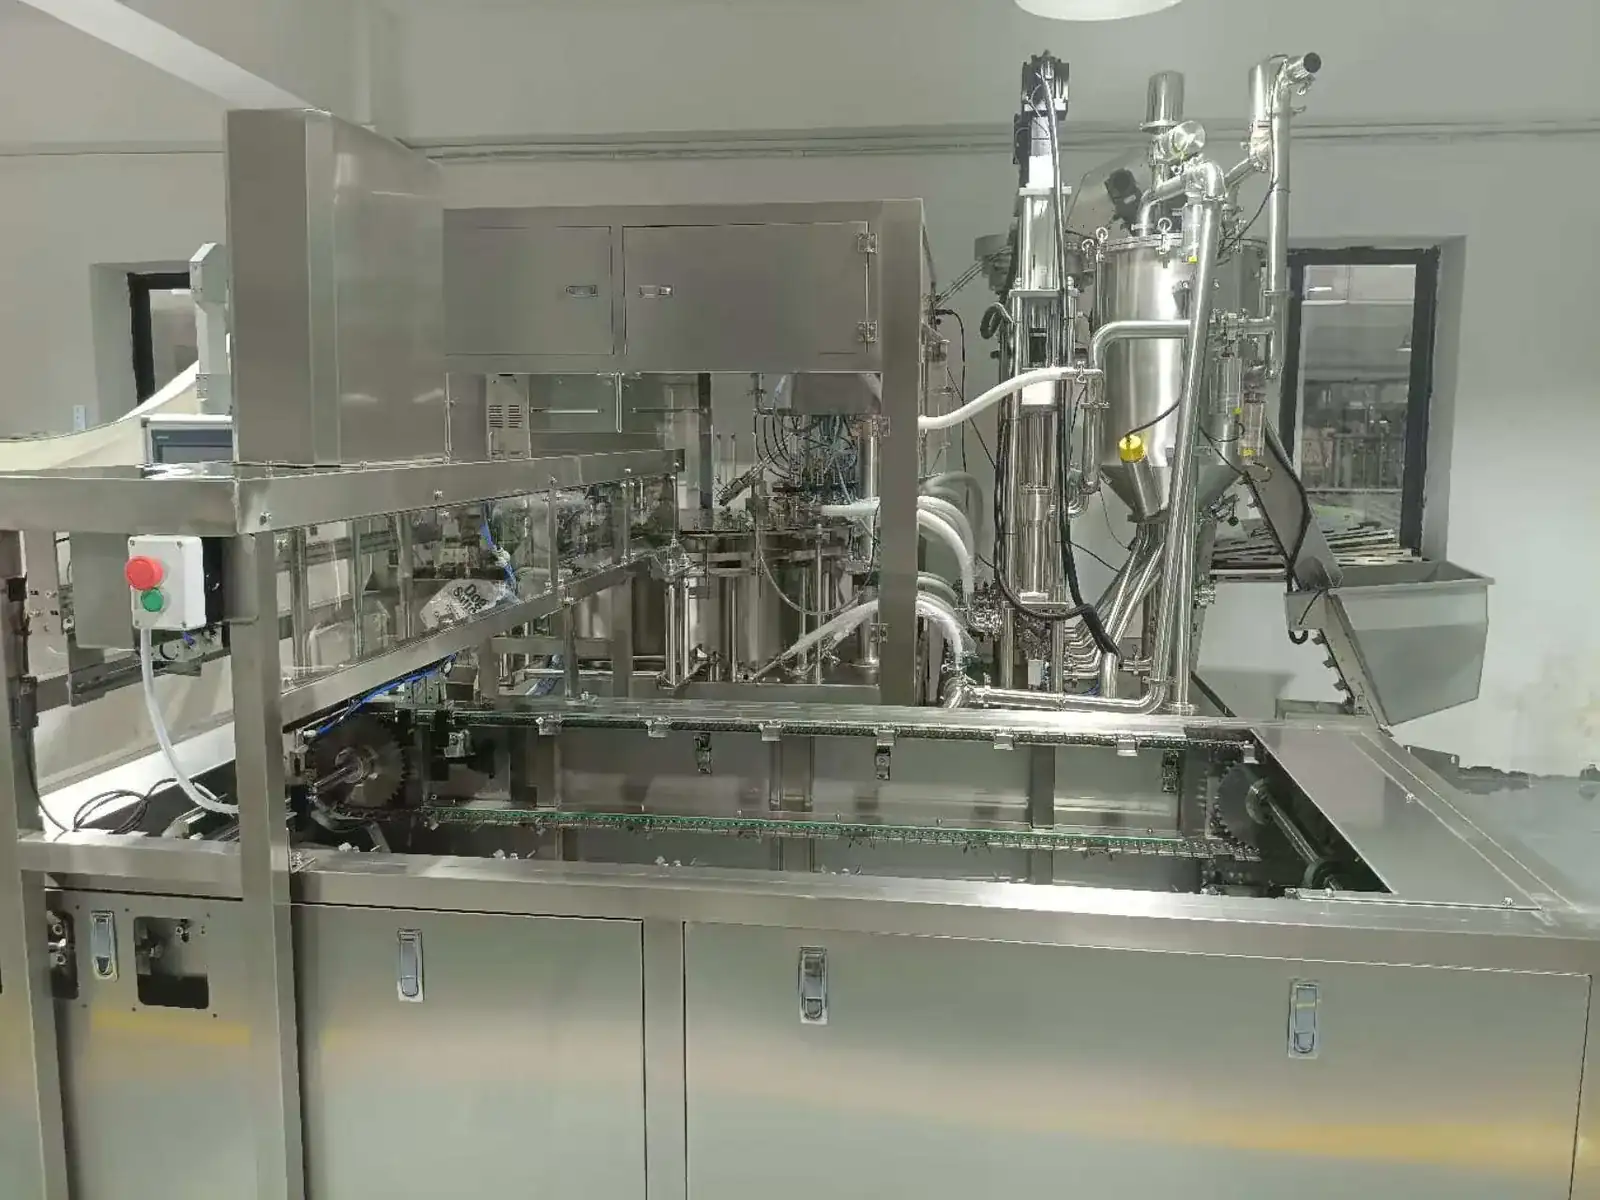
The safest machine choice is usually revealed by the hardest product and package combination. I would freeze a dairy configuration only after that worst-case SKU has been run through the intended filler, package path and acceptance checks—not after an empty-cycle demonstration.
Accepted output
The contractual production basis should name the real product, fill, package, closure, quality criteria, test duration and included line boundary.
Identify the product lot and condition, dose, film or pouch revision, spout and cap, installed filler, machine configuration and operator basis.
Separate accepted packs, dosing rejects, opening or feed failures, contaminated seals, cap defects, stops, empty carriers, rework and product loss.
Include refill, controlled stop, restart, missing pouch or cap, blocked discharge, alarm handling and first-off release after the defined changeover.
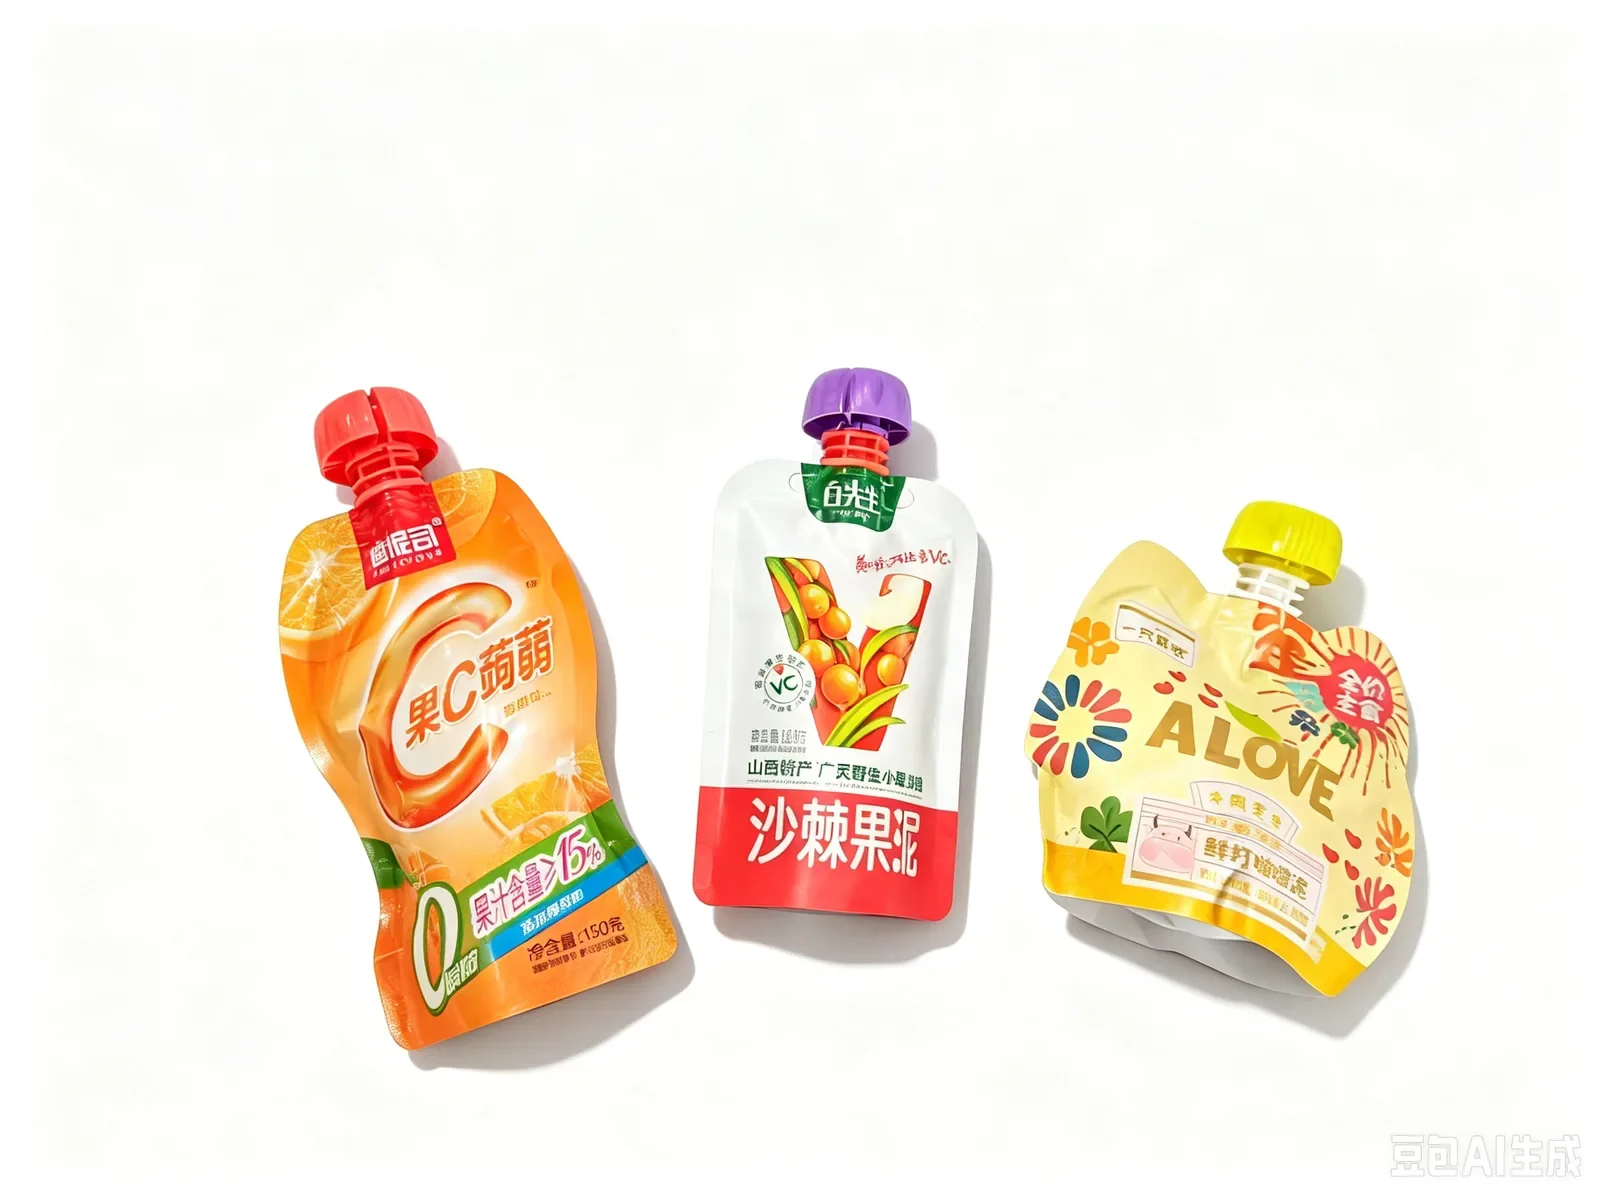
Head count or machine cycle rate is only one input. Fill volume, viscosity, pouch presentation, cap supply, product replenishment, cleaning interruptions and the accepted defect limit can all set the usable output.
For premade spout pouches, compare the available 6-, 8- and 12-head filling and capping configurations only after the same product and package basis has been fixed.
Quotation inputs
Product type, composition limits, density or viscosity range, temperature, particles, foam or dust, dose range, SKU list and representative samples.
Finished dimensions, controlled drawing, roll-film specification or premade pouches, spout and cap drawings, print repeat, samples and expected tolerances.
Accepted output by priority SKU, tolerance method, run duration, defect rules, refill condition, changeovers, operators and downstream destination.
Cleaning method, contact-part access, allergen or recipe controls, product hold condition, plant procedures and required material documentation.
Product supply, tanks or conveyors, coding, inspection, rejection, cap feeding, discharge, accumulation, cartoning, controls and data expectations.
Utilities, available layout, destination requirements, FAT attendance, installation, training, manuals, spares, commissioning and service boundary.
Buyer questions
The candidate route may cover milk powder and dry dairy blends, liquid dairy portions, yogurt or cultured products in confirmed sachets or spout pouches. Suitability is not decided by the product name alone; provide the actual operating condition, dose, package and cleaning requirements for review.
Not as one universal setup. Powder and liquid or cultured dairy products require different dosing and product-contact architectures. Some packaging platforms can be configured around more than one product, but filler change, cleaning boundary, cross-contamination control, tooling, output and validation must be evaluated before any common-platform decision.
Use a sachet when the required portion, opening experience and distribution format support a small sealed pack. Use a spout pouch when reclosure, controlled dispensing or a larger portion is required. Then decide whether the spout pouch is supplied premade or formed from roll film. Material cost alone does not determine the best route.
A premade system receives a finished pouch with a fitted spout, then feeds, fills and caps it. A roll-film HFFS system forms the pouch and integrates the relevant spout operations within the confirmed line. The two routes have different material specifications, machine functions, storage, changeover and acceptance requirements.
Specify accepted finished packs per minute or hour for the named product, dose, package, closure, quality limits and test duration. State the included product supply, filler, cap supply, inspection and downstream condition so an isolated machine cycle is not mistaken for complete-line output.
Use representative product and production-intent packaging. Record the installed configuration, run duration, accepted count, rejects by cause, dose results, seal or cap checks, coding, alarms, stop and restart, refill, changeover, cleaning demonstration and any unresolved deviations. Final regulatory and food-safety approval remains the buyer's responsibility.
Related machine routes
Project review
Send the product condition, dose range, package drawing or samples, required accepted output, cleaning method and destination. INMAYPACK will review the appropriate flexible-packaging route and identify the missing inputs before a scoped proposal.