
Detergent Packaging Machine for Powder and Liquid Pouches
Choose a detergent filling and packing route from the actual formula, flow or powder behavior, dose, flexible package and acceptance test—not from one generic machine description.
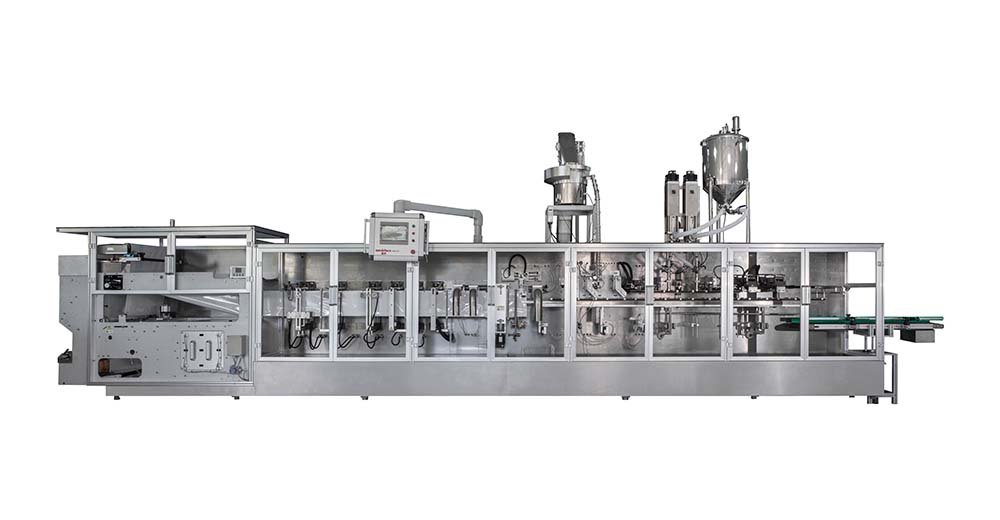
Separate liquid detergent from powder before choosing the machine
“Detergent” is a market category, not a filling specification. A pump that handles one liquid formula does not automatically suit another product with different viscosity, foaming, air entrainment, temperature behavior or cutoff. A powder filler faces a different set of variables: bulk density, flow, dust, compaction, refill consistency and the way powder reaches the seal area.
This page covers detergent packed in heat-sealed flexible sachets and pouches. It does not claim one universal configuration for liquids and powders, and it does not cover rigid bottles, jugs, cartons, pods, tablets or bars. Those packages and products require separate equipment and project review.
Match the dosing principle to the physical product
Liquid detergent filling route
A liquid detergent pouch packing machine must control the formula from supply vessel to nozzle. Pump and nozzle selection depend on the real product, target fill, temperature range, foaming, stringing or dripping behavior and the way the pouch presents beneath the fill point.
- Define viscosity behavior and supply condition.
- Observe foam, tails, drips and air entrainment.
- Confirm product-contact material compatibility.
- Test stop, restart, refill and changeover conditions.
Detergent powder dosing route
A detergent powder packing machine must keep product feeding and dosing stable while limiting unacceptable dust at the package and seal. Filler selection depends on the supplied powder, bulk-density variation, flow, particle distribution, compaction, target dose and refill method.
- Supply a representative production powder.
- Define hopper refill and powder conditioning.
- Control dust near the seal and machine enclosure.
- Check settling, finished-pack shape and dose method.
Choose the flexible package architecture before the model
Flat detergent sachets
Form, fill, seal and cut compact packs from approved roll stock. The fill opening, film, seal layout and dose must work together. Compare the liquid sachet route or the powder sachet route.
Roll-film stand-up pouches
Form a bottom-gusset pouch, present the opening, fill and close it in one HFFS process. Film tracking, gusset forming, opening access, fill cutoff and sealing require one combined trial. Review liquid doypack systems.
Spout pouches
Coordinate the pouch drawing, spout, cap, filling access and closure sequence. A successful pump demonstration alone does not qualify the complete spout-pouch process. See the spout pouch filling machine route.
Supplied premade pouches
Pick, open, fill and seal an approved finished pouch. Pouch consistency, opening access and sealing presentation belong in the acceptance test. Compare premade pouch filling and sealing. If the supplied detergent pouch already has a fitted spout, review the separate premade spout pouch filler and capper.
Refill and multi-dose packs
Define the consumer opening, reclosure, carrying and dispensing requirements before selecting pouch size and closure. Do not infer the required machine from the phrase “refill pouch” alone.
Multiple formulas or fragrances
List the complete range. Product changes can alter metering, foam, dust, residual product, cleaning, first-off checks and the time required to release acceptable packs after changeover.
Send the information that changes the line
| Input | What to provide | Decision affected |
|---|---|---|
| Product identity | Liquid or powder, formula family, representative sample and current safety data or handling information | Machine scope, contact path and project review |
| Physical behavior | Liquid flow, viscosity and foam behavior; or powder bulk density, flow, dust and compaction behavior | Metering principle, hopper, pump, nozzle and dust control |
| Operating condition | Supply temperature, hold time, refill method, planned stops and restart condition | Product supply, repeatability and trial sequence |
| Target fill | Nominal amount, permitted variation and the method used to check finished packs | Dosing architecture and FAT sampling plan |
| Package | Drawing, dimensions, film or premade-pouch source, closure, seal layout and opening feature | Machine family, tooling, forming, pickup and opening |
| Changeover | Formula range, fragrances, colors, pack sizes, cleaning method and acceptable residual product | Access, drainability, cleaning boundary, recipes and release checks |
| Line interfaces | Upstream supply, coding, inspection, discharge, counting, cartoning and case handling | Layout, controls, responsibilities and quotation boundary |
Define every handoff from product supply to accepted pack
Supply the detergent
Define how the liquid or powder reaches the filler, how the operating condition is maintained and who owns replenishment and product consistency.
Meter the dose
Select and trial the dosing principle with the actual formula instead of assuming that one pump or powder filler suits every detergent.
Form or open the pack
Control roll-film forming or premade-pouch pickup, presentation and opening using the approved production material.
Protect the seal
Manage liquid drips, foam and tails or powder dust and settling so unacceptable product does not remain in the seal area.
Seal and close
Establish the usable sealing window and, for spouted packs, the spout and cap sequence required by the project.
Inspect and discharge
Agree coding, visible checks, reject conditions, finished-pack handling and the evidence recorded during acceptance.
Control foam, cutoff and seal-area exposure
A detergent filling machine must be evaluated as a connected liquid path. The useful test includes the supply source, transfer, metering device, nozzle, pouch position and fill profile. Watch what happens when the product is replenished, when the machine stops and when it restarts—not only during a short stable run.
Foam can consume headspace or change the required fill motion. Tailing and dripping can contaminate the seal. Product temperature and trapped air can change behavior between the sample room and production. The accepted configuration should therefore be based on a representative formula and the intended operating range. Use the pouch filling system selection guide to compare the metering boundary.
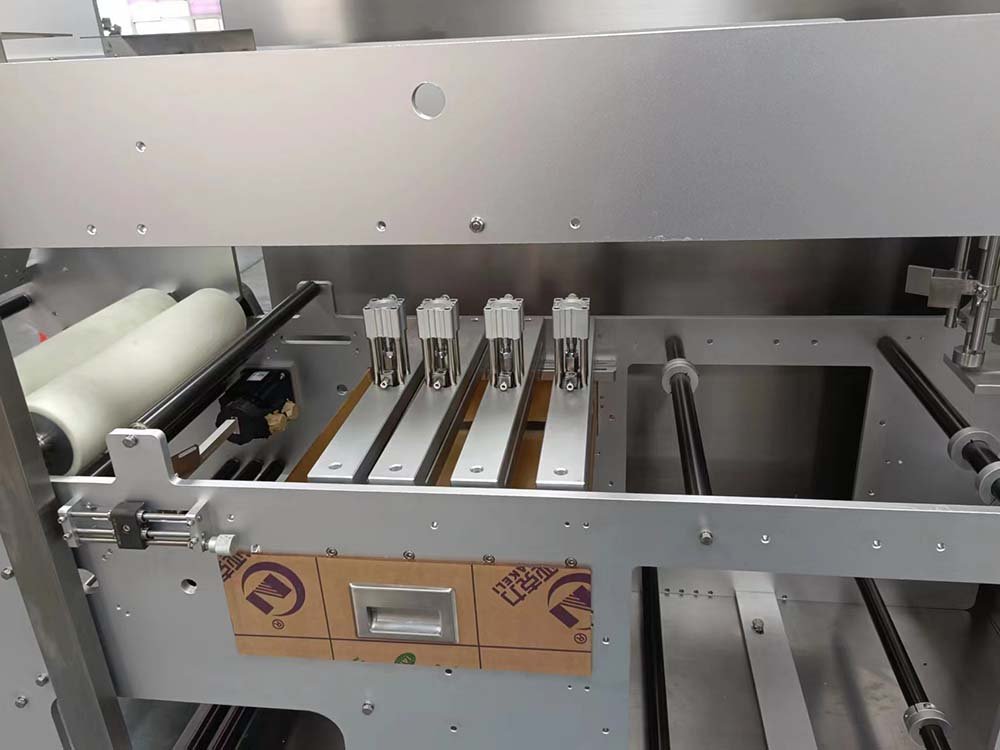
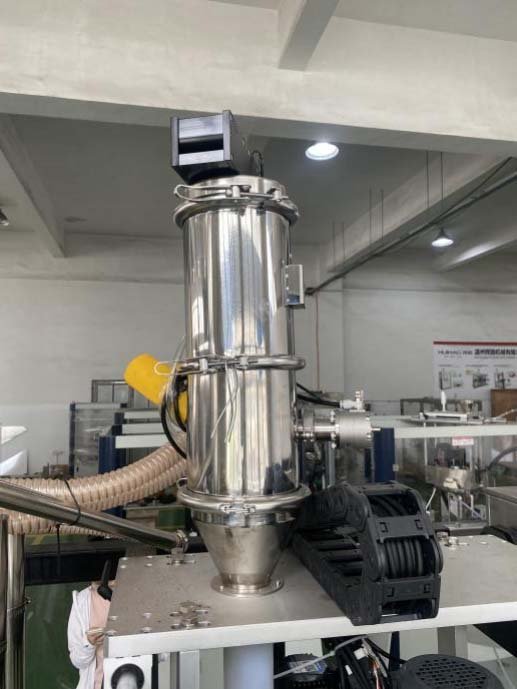
Keep feeding, dosing and seal cleanliness on one test basis
Powder behavior at the filler depends on more than nominal dose. Bulk-density changes can alter the volume occupied by a dose. Refill events can change head pressure or compaction. Fine dust can reach the sealing surface, while a settled powder can change the shape and handling of the finished pack.
Define the production powder, upstream transfer, hopper refill, dosing principle, package opening and dust-removal boundary together. Trial the expected start, steady run, refill, planned stop and restart conditions. For a broader comparison of dry-product equipment, review the powder filling machine selection hub.
Confirm materials, cleaning and product handling before approval
Control the failure modes that change usable output
Opening and presentation
A formed or supplied pouch must open consistently and remain positioned for the agreed fill. Wrinkles, static, closure features or pouch variation can reduce usable access.
Liquid contamination
Observe foam, splash, stringing and nozzle cutoff during stable running, stops and restarts. Define how affected packs are detected and rejected.
Powder contamination
Check airborne and falling dust, product settling and the timing between fill and seal. A clean demonstration pack does not prove a sustained production condition.
Seal window
Use the intended film or pouch structure and agree temperature, dwell, pressure and finished-seal checks for the supplied material.
Spout and closure
For refill pouches, test the controlled drawing, spout presentation, weld or insertion relationship, filling access, cap sequence and leak checks together.
Downstream handling
Confirm coding, inspection, discharge, accumulation and secondary packing without damaging, distorting or contaminating the accepted package.
Use the stand-up pouch seal integrity guide to define evidence instead of judging a package by appearance alone.
Make every supplier price the same detergent line boundary
| Scope group | Define before comparison | Evidence to request |
|---|---|---|
| Product supply | Source vessel or powder feed, transfer method, operating condition, replenishment and ownership | Marked process boundary and line-layout drawing |
| Primary package | Roll film or premade pouch, drawing, dimensions, closure, lane or station architecture | Approved material and configuration drawing |
| Dosing system | Liquid or powder metering principle, contact path, hopper or pump, nozzle and cutoff | Recorded trial using the agreed detergent and dose |
| Product controls | Foam, drip, dust, seal contamination, code, reject conditions and inspection interfaces | Test method, samples and retained results |
| Changeover | Formula and pack range, residual-product limit, cleaning steps, change parts and release checks | Procedure, responsibility matrix and first-off record |
| Downstream scope | Discharge, accumulation, counting, cartoning, case packing and line control | Interface list and included equipment |
| Delivery and support | Documents, training, installation support, spare-parts scope and acceptance responsibilities | Issued quotation and handover list |
For a wider project boundary, review turnkey packaging solutions before comparing quotations.
Accept the finished detergent pack—not an empty-cycle claim
Freeze the test basis
Record the formula or approved sample, product condition, target fill, package material, drawing, closure and machine configuration.
Define accepted output
Agree how output is counted, sustained test duration, allowed stops, sample frequency, reject rules and the definition of an acceptable pack.
Test operating events
Include normal running, replenishment, planned stops, restart behavior and the changeover work that materially affects production.
Check the product path
Inspect the liquid contact path or powder feeding and dust boundary at agreed points before, during and after the test.
Verify package quality
Apply the agreed fill, code, seal, closure, leakage, contamination and finished-pack handling checks to the defined sample.
Retain useful evidence
Keep settings, faults, rejects, samples, test results and the video or records required by the issued project scope.
Use the stand-up pouch machine FAT checklist to structure the acceptance discussion.
Detergent packaging machine FAQ
Can one machine pack both liquid detergent and detergent powder?
Do not assume so. Liquids and powders use different supply, metering and contamination-control architectures. A project may share some package or downstream equipment, but each product path requires separate review and testing.
What pouch formats can be reviewed?
Flexible-package options include roll-film flat sachets, roll-film stand-up pouches, spout pouches and supplied premade pouches. The appropriate route depends on dose, opening and closure requirements, material, product behavior and accepted-pack economics.
What information is needed for a quotation?
Send the product type, representative formula or sample, handling information, target fill, package drawing and samples, material source, closure, output goal, utility and upstream/downstream requirements, formula range and acceptance expectations.
How is a foaming liquid detergent evaluated?
Test the actual formula through the proposed supply, metering and nozzle path. Observe foam, headspace, fill motion, dripping and restart behavior, then define the accepted finished-pack checks and output on that basis.
How is detergent powder dust handled?
Dust control begins with the full path from transfer and hopper refill through dosing, pouch presentation and sealing. The required extraction, enclosure, access and cleaning boundary must be defined for the supplied powder and site.
Can the line pack bleach or solvent-rich cleaners?
Not by default. Products with materially different corrosion, compatibility, vapor, safety or hazardous-area requirements need a separate review based on current product information and destination-site requirements.
Does this page cover bottle filling?
No. This page covers flexible sachets and pouches. Bottles, jugs and other rigid containers require a different filling, closure, labeling and handling route.
What should a detergent packaging FAT include?
Use the agreed product, package and configuration. Define duration, acceptable packs, sampling, reject rules, replenishment, stops, restarts, changeover events and the evidence retained for approval.
Related detergent pouch routes and project support
Liquid packaging machines
Compare liquid sachet, doypack, spout-pouch and premade-pouch architectures.
Powder filling machines
Review powder behavior, feeding, dosing, dust and flexible-package choices.
Liquid sachet systems
Evaluate roll-film flat sachet forming, filling, sealing and accepted output.
Spout pouch systems
Define the pouch, spout, filling access and closure sequence as one project.
Service and project support
Review documentation, testing, training and post-delivery responsibilities.
Contact INMAYPACK
Send the detergent, package, target fill, output goal and line boundary for review.
Send the detergent and package the line must actually run
Share the liquid formula or powder sample, operating condition, target fill, pouch drawing or samples, closure, output goal, changeover range and required line boundary. INMAYPACK can then review the flexible-package route against one defined acceptance basis.